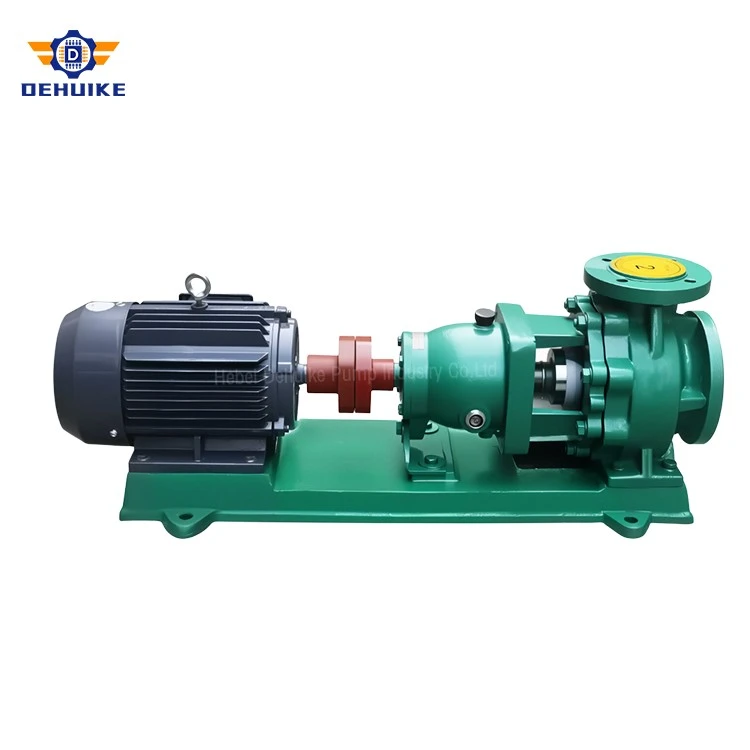
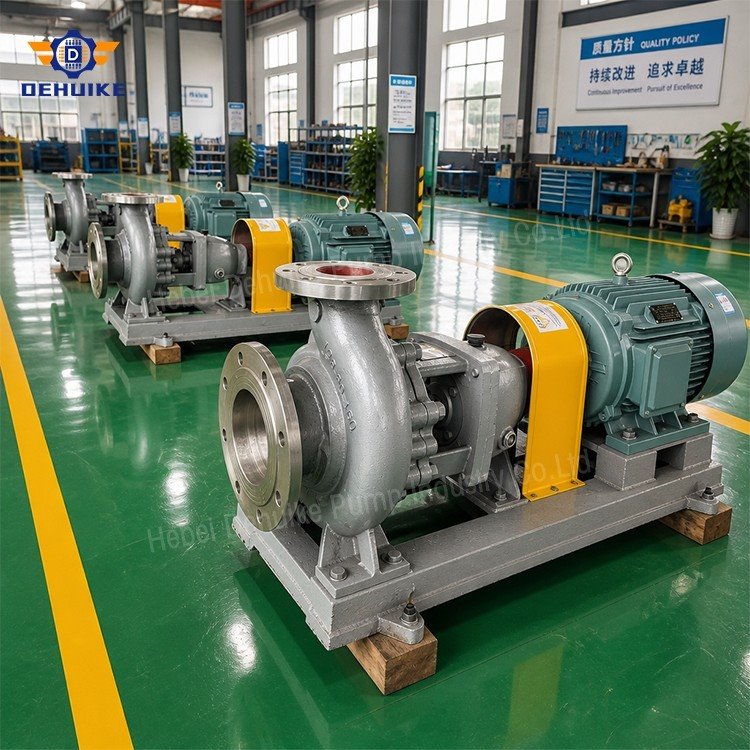
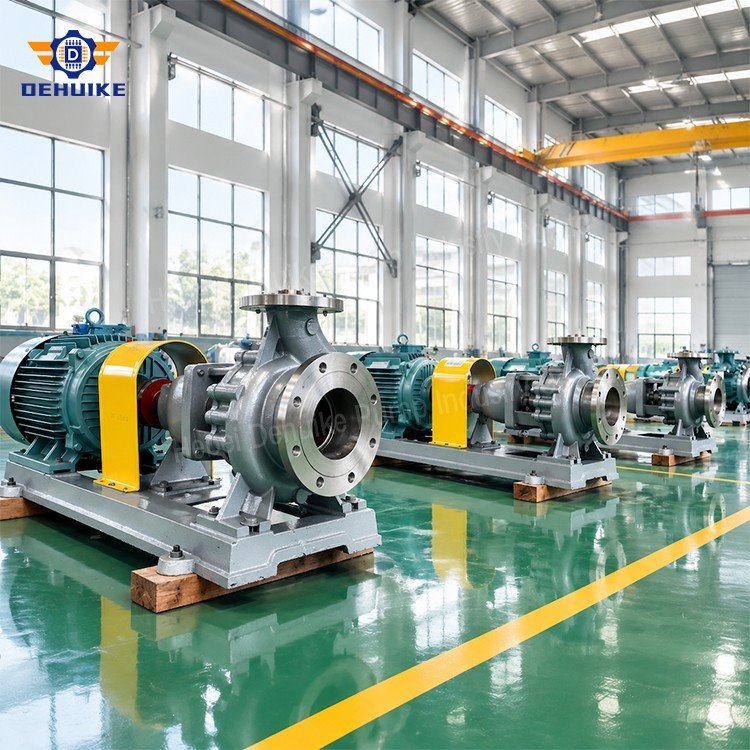
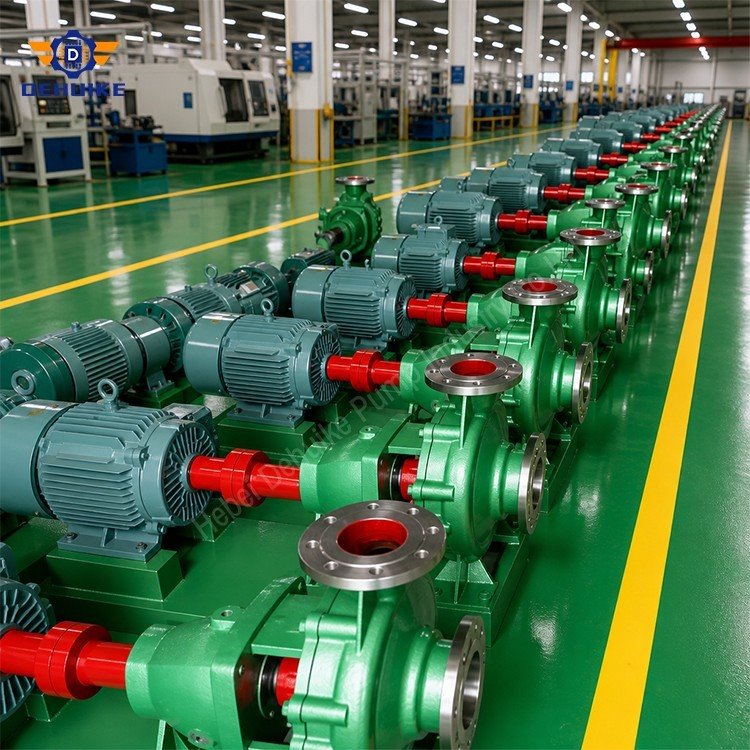
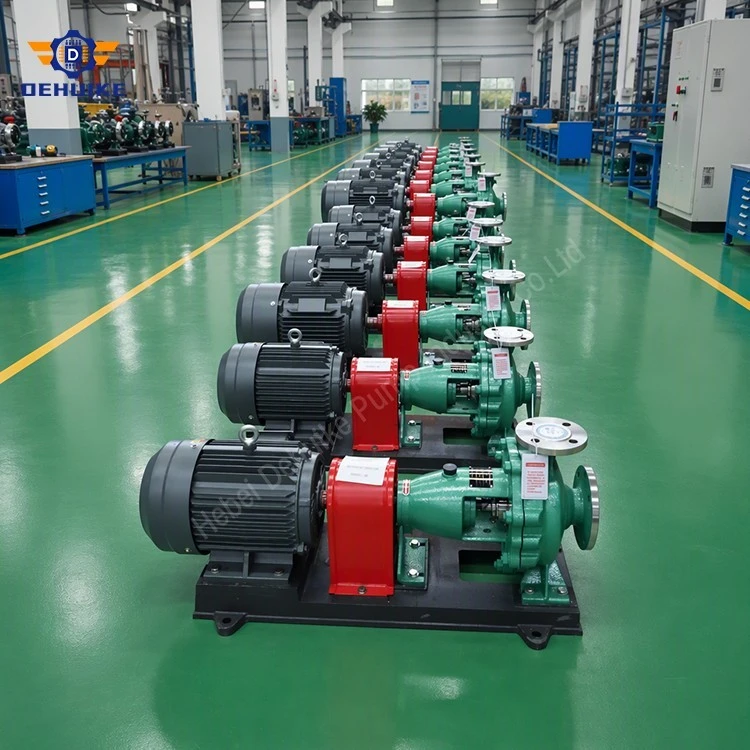
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of acid resistant chemical pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk acid resistant chemical pump for sale here from our factory. Also, pricelist is available.
Acid-Base Corrosion Dynamics, Extreme pH Media Handling, and Fluid Transport Realities
Conveying aggressive acidic electrolytes, industrial mineral pickling liquors, and acid-gas absorption solutions represents one of the most hazardous fluid handling frontiers across international process engineering. In continuous-flow processing plants where operating media exhibit extreme acidity (frequently reaching pH levels below 1.5) combined with thermal swings up to 150°C, ordinary metallic pump components suffer rapid deterioration. The combined kinetics of galvanic attack, anodic dissolution, and hydrogen-induced cracking degrade standard carbon steels and low-alloy cast irons within mere operational days. The Acid Resistant Chemical Pump is engineered specifically to withstand these destructive operating regimes, providing continuous fluid containment, hydro-mechanical stability, and robust process reliability across demanding chemical installations.
From an electrochemical perspective, metallic degradation in acidic solutions depends on the oxidizing versus reducing potential of the fluid stream. In highly oxidizing acidic media-exemplified by concentrated nitric acid or hot chromic acid baths-metal preservation relies on establishing an uninterrupted, thermodynamically stable chromium oxide surface passivation barrier.
Conversely, reducing or halogenated acids-such as hydrochloric acid, dilute sulfuric acid, and hydrofluoric blends-rapidly depassivate ordinary stainless steels by scavenging surface oxygen. To defeat these dual degradation pathways, the Acid Resistant Chemical Pump utilizes tailored multi-component metallurgy, incorporating controlled percentages of chromium, nickel, molybdenum, and nitrogen to guarantee chemical passivity across diverse acid concentration gradients.
Thermodynamic fluid properties also vary dramatically across different industrial acid grades. For example, concentrated 98% commercial sulfuric acid exhibits a high specific gravity approaching 1.84 kg/dm³ alongside elevated dynamic viscosity at lower ambient temperatures. Such high-density fluids exert severe hydraulic mass loadings and increased radial hydraulic forces against the pump impeller and casing cutwater. The heavy-duty acid chemical transfer pump accounts for these extreme fluid densities through reinforced structural casting walls, heavy-duty drive shafts, and carefully sized electric motor couplings that prevent motor overload trips during cold fluid startup.
Beyond chemical composition, internal fluid dynamics directly dictate component service life in acidic environments. High-velocity localized turbulence, secondary Taylor-Görtler vortices, and micro-bubble implosions aggressively scour passivated metallic boundaries, exposing fresh metal substrate to cyclical chemical erosion. Compliant with ISO 2858 and ISO 5199 manufacturing standards, the Acid Resistant Chemical Pump features hydrodynamically optimized volute contours and streamlined impeller waterways. This design suppresses localized eddies, minimizes boundary-layer wall shear stress, and prevents low-pressure recirculation zones where stagnant acid pockets or aggressive crystalline deposits can initiate localized crevice attack.
Plant safety standards in acid-processing environments demand that maintenance procedures minimize technician contact with hazardous fluids. The Acid Resistant Chemical Pump incorporates an engineered back-pull-out structural architecture complemented by integrated casing drain ports. Operators can thoroughly flush, neutralize, and evacuate internal acid volumes prior to disassembling the rotating cartridge. By withdrawing the complete rotating assembly-including the enclosed impeller, precision alloy shaft, seal chamber, and bearing housing-rearward toward the motor, overhauls are conducted without unbolting suction and discharge piping manifolds or disturbing casing baseplate anchors, cutting turnaround craft labor down to under ninety minutes.
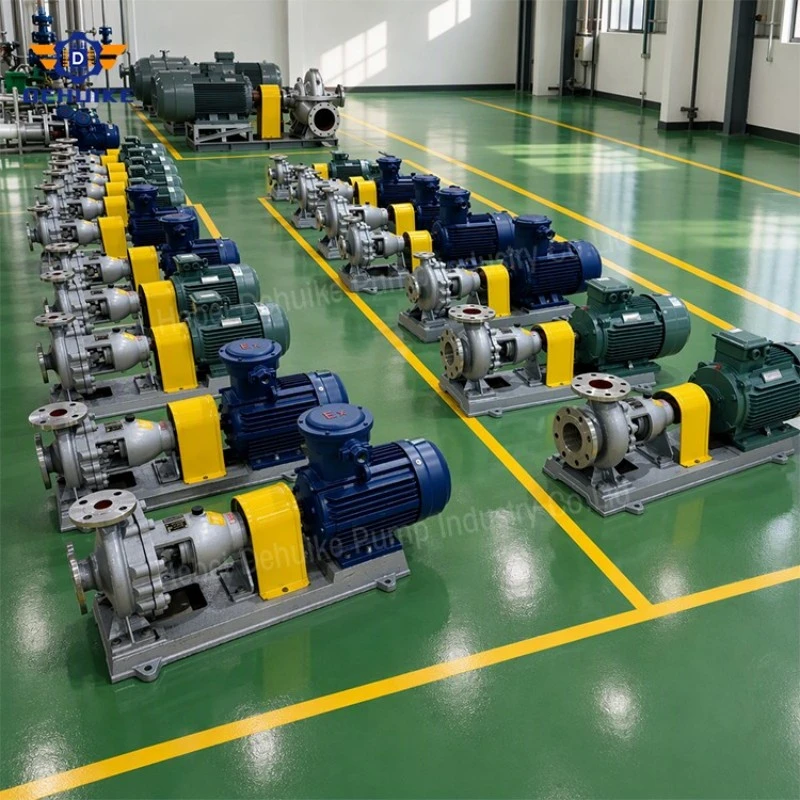
Technical Specifications & Tri-Series Parametric Envelopes
Modern chemical facilities require versatile hydraulic envelopes capable of satisfying high-head acid absorption tower recirculation as well as high-volume, low-shear acid railcar unloading. To facilitate accurate engineering sizing and avoid hydraulic mismatching, the Acid Resistant Chemical Pump platform is structured into three dedicated performance categories. The parameters tabulated below represent verified performance data collected from calibrated factory testing loops, categorized by rotational speed and impeller geometry.
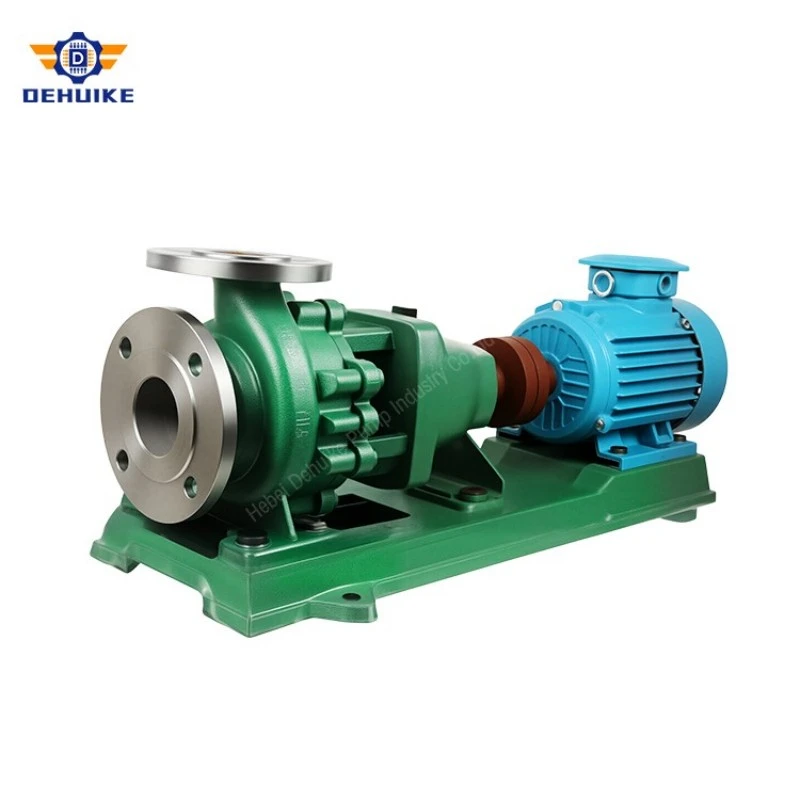
2.1 Series 1: Standard 2-Pole High-Flow Acid Series (2900 r/min Baseline)
Operating at a nominal 2-pole synchronous speed of 2900 r/min (50 Hz), Series 1 encompasses the high-velocity, full-diameter baseline envelope engineered for applications requiring high discharge pressures and substantial flow delivery. Capable of generating single-stage heads up to 125 meters and handling capacities from 50 m³/h up to 200 m³/h at rated efficiency points, Series 1 models are widely specified for long-distance acid distribution headers, reactor vessel pressure injection, and multi-stage scrubber tower circulation.
With untrimmed impellers running at 2900 r/min, Series 1 achieves hydraulic efficiencies reaching 78% in heavy chemical frames, significantly curbing continuous electrical power consumption. Net Positive Suction Head requirements (NPSHr) remain tightly governed between 2.0 and 4.0 meters at the rated optimal efficiency point. Below are verified baseline ratings for representative Series 1 models:
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH80-65-125 |
80 |
65 |
2900 |
50 |
20 |
74 |
3.63 |
5.5 |
3 |
|
IH80-65-160 |
80 |
65 |
2900 |
50 |
32 |
73 |
5.97 |
7.5 |
2.5 |
|
IH100-80-125 |
100 |
80 |
2900 |
100 |
20 |
78 |
7 |
11 |
4.5 |
|
IH100-80-160 |
100 |
80 |
2900 |
100 |
32 |
78 |
11.2 |
15 |
4 |
|
IH100-65-200 |
100 |
65 |
2900 |
100 |
50 |
76 |
17.9 |
22 |
3.6 |
|
IH100-65-250 |
100 |
65 |
2900 |
100 |
80 |
72 |
30.3 |
37 |
3.8 |
|
IH100-65-315 |
100 |
65 |
2900 |
100 |
125 |
66 |
51.6 |
75 |
3.6 |
|
IH125-100-200 |
125 |
100 |
2900 |
200 |
50 |
81 |
33.6 |
45 |
4.5 |
2.2 Series 2: Hydraulic Trimming Energy-Optimization Series (A/B Trims at 2900 r/min)
In continuous acid processing lines, operating a pump with excessive impeller diameter creates excess discharge head that must be dissipated across restrictive control valves, causing accelerated valve trim erosion, severe fluid turbulence, and high electrical power waste. The Series 2 Acid Resistant Chemical Pump solves this system inefficiency through precision impeller trimming (denoted by letter suffixes A and B), calibrated according to centrifugal affinity laws.
By fine-tuning outer vane diameters on automated CNC machining equipment, Series 2 aligns pump output directly with actual piping friction curves. For instance, trimming model IH100-80-160 down to its 'A' trim reduces rated discharge head from 32 m to 28 m, curtails absorbed shaft power from 11.2 kW to 9.16 kW, and allows pairing with an economical 11 kW motor while preserving an impressive 78% hydraulic efficiency. This engineering optimization lowers ongoing electrical utility expenditures across 8,760 hours of annual operation.
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH80-65-125A |
80 |
65 |
2900 |
44.7 |
16 |
75 |
2.27 |
4 |
3 |
|
IH80-65-160A |
80 |
65 |
2900 |
46.8 |
28 |
73 |
4.8 |
5.5 |
2.5 |
|
IH100-80-125A |
100 |
80 |
2900 |
89.4 |
16 |
78 |
5 |
7.5 |
4.5 |
|
IH100-80-160A |
100 |
80 |
2900 |
93.51 |
28 |
78 |
9.16 |
11 |
4 |
|
IH100-65-200A |
100 |
65 |
2900 |
95 |
45 |
76 |
15.35 |
18.5 |
3.6 |
|
IH100-65-250A |
100 |
65 |
2900 |
93.5 |
70 |
72 |
26.6 |
30 |
3.8 |
|
IH100-65-315A |
100 |
65 |
2900 |
95.5 |
114 |
66 |
45.03 |
55 |
3.6 |
|
IH125-100-200A |
125 |
100 |
2900 |
190 |
45 |
81 |
28.8 |
37 |
4.5 |
2.3 Series 3: 4-Pole Low-Shear Heavy-Duty Acid Series (1450 r/min J/JA/JB Trims)
When conveying boiling organic acids, concentrated acid slurries carrying abrasive crystal precipitates, or viscous polymerizing media, high-speed 2900 r/min operation introduces severe fluid shear, rapid mechanical seal face heating, and elevated risk of vapor cavitation. The Series 3 low-speed acid process pump addresses these severe conditions by pairing the wet-end with 4-pole electric drives running at a nominal 1450 r/min (denoted by suffix J).
Operating at half rotational speed cuts impeller peripheral velocity by 50%, reducing mechanical sliding friction and dynamic seal face thermal stress by more than seventy percent. Furthermore, Series 3 achieves exceptionally benign suction behavior, maintaining critical NPSHr levels down to 2.5 meters. Operating power requirements drop to modest ranges (0.48 kW to 6.3 kW across large frames), making Series 3 the preferred technical selection for sensitive crystallization, spent acid recycling, and continuous heavy-duty chemical processing.
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH80-65-125J |
80 |
65 |
1450 |
25 |
5 |
71 |
0.48 |
0.75 |
2.5 |
|
IH80-65-160J |
80 |
65 |
1450 |
25 |
8 |
69 |
0.79 |
1.5 |
2.5 |
|
IH100-80-125J |
100 |
80 |
1450 |
50 |
5 |
75 |
0.91 |
1.5 |
2.5 |
|
IH100-80-160J |
100 |
80 |
1450 |
50 |
8 |
75 |
1.45 |
2.2 |
2.5 |
|
IH100-65-200J |
100 |
65 |
1450 |
50 |
12.5 |
73 |
2.33 |
4 |
2 |
|
IH100-65-250J |
100 |
65 |
1450 |
50 |
20 |
68 |
4 |
5.5 |
2 |
|
IH100-65-315J |
100 |
65 |
1450 |
50 |
32 |
63 |
6.92 |
11 |
2 |
|
IH125-100-200J |
125 |
100 |
1450 |
100 |
12.5 |
76 |
4.48 |
7.5 |
2.5 |
Exotic Acid-Resistant Alloys, Heavy-Walled Wet-End Castings, and Dynamic Seal Containment
The mechanical durability of the Acid Resistant Chemical Pump depends on its robust physical construction, heavy corrosion allowances, and leak-free sealing architecture. Every internal component is engineered to maintain dimensional stability and fluid containment under aggressive chemical exposure:
- Reinforced Pressure-Retaining Casing: Heavy-walled casing volutes feature substantial extra metal thickness as an engineered corrosion allowance against gradual acid dissolution. The casing includes a top-centerline self-venting discharge nozzle and integrated bottom casing drain tapped with acid-resistant blind plugs for safe draining prior to maintenance.
- Precision Balanced Enclosed Impeller: Cast with smooth three-dimensional backward-curved vanes to maximize hydraulic efficiency. Axial thrust forces are counteracted via precision-machined rear wear rings and calibrated balance holes that vent pressurized acid back to the suction eye, protecting drive bearings from thrust fatigue.
- Heavy-Duty Stepped Alloy Shaft: Designed with an enlarged diameter beneath the sleeve to minimize the shaft overhang ratio (L³/D⁴), holding dynamic shaft deflection to less than 0.04 mm at the seal faces. This rigid geometry prevents micro-misalignment and premature seal face chipping under fluctuating pressure conditions.
- API 682 Compliant Seal Chamber: An enlarged bore cavity promotes convective fluid circulation around dynamic sealing faces. The chamber accommodates single cartridge seals, balanced double mechanical seals (API Plan 52/53A/53B), and chemically inert silicon carbide against silicon carbide faces with perfluoroelastomer (FFKM) secondary O-rings for complete containment of hazardous fumes.
- Auxiliary Quench and Barrier Fluid Integration: For crystallizing acid streams such as technical-grade phosphoric acid, the stuffing box incorporates steam quench or demineralized water flushing ports (API Plan 62) to dissolve abrasive salts on atmospheric seal faces, preventing face binding and catastrophic leakage.
- Sealed Rigid Cast Bearing Frame: Houses a matched pair of heavy-duty angular contact ball bearings and a cylindrical roller bearing in an oil-lubricated cast housing. Labyrinth bearing isolators prevent ambient atmospheric acid fumes and moisture from penetrating the lubricating oil sump.
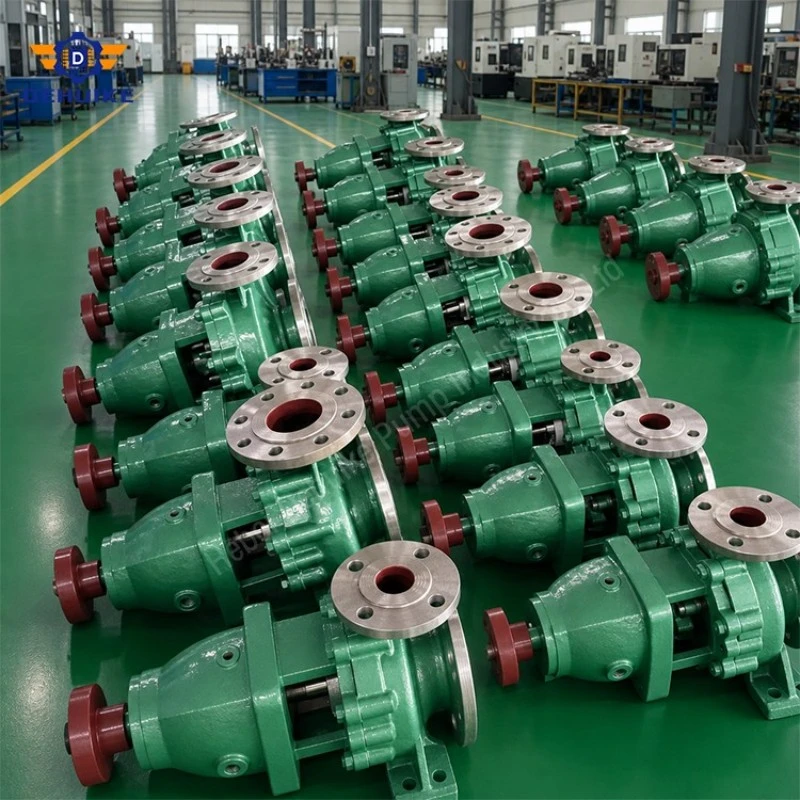
Exotic Alloy Melting, Solution Annealing, and Passivation Pickling
Manufacturing fluid machinery for aggressive chemical services requires stringent metallurgical discipline, modern foundry technology, and rigorous post-cast chemical passivation. Component fabrication follows a tightly controlled sequence to ensure uniform microstructure and maximum corrosion resistance:
- Specialized Metallurgical Formulations: Wetted castings are produced across a dedicated alloy matrix: 304 (CF8) for clean oxidizing acids; 316L (CF3M) with ultra-low carbon (<0.03%) and 2.5% Molybdenum for organic and dilute mineral acids; Duplex 2205 (S31803 / 1.4462) with PREN > 35 for chloride-laden brines and hot acidic mixtures; and nickel superalloys (Hastelloy C-276 / Alloy 20) for severe boiling acid services.
- High-Purity Silica Sol Investment Casting: Molds are prepared using fine silica sol ceramic slurries, resulting in wetted waterways with surface finishes of Ra 1.6 to 3.2 µm. This micro-smoothness eliminates surface micro-porosity and inclusions where localized pitting cells initiate.
- High-Temperature Solution Annealing Heat Treatment: All stainless and duplex alloy castings undergo mandatory solution heat treatment at 1050°C–1120°C followed by rapid water quenching. This thermodynamic cycle redissolves precipitated chromium carbides back into the austenitic solid matrix, eliminating chromium-depleted grain boundaries and preventing intergranular stress corrosion failure.
- Chemical Pickling & Surface Passivation: Following multi-axis CNC machining, all wetted surfaces undergo chemical immersion pickling in a formulated hydrofluoric-nitric acid bath in full accordance with ASTM A380 specifications. This removes free iron contaminants and embedded tooling particles, followed by concentrated nitric acid passivation that produces an unbroken chromium oxide protective surface film.
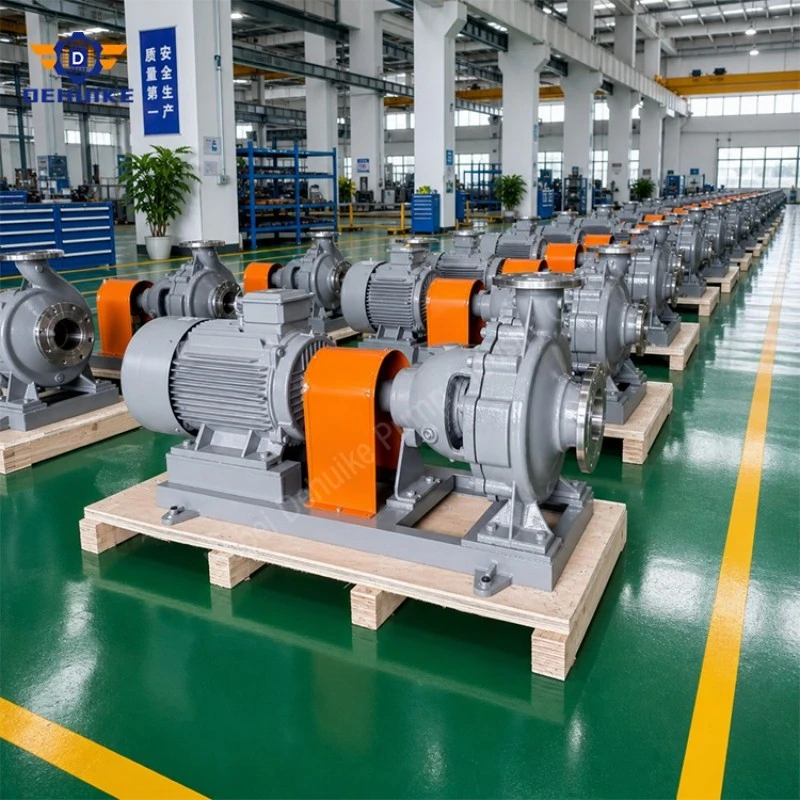
Acid Immersion Testing, Hydrostatic Pressure Integrity, and NDT Wall-Thickness Validation
Quality assurance for the Acid Resistant Chemical Pump operates under certified ISO 9001 quality management protocols, ensuring that every manufactured unit satisfies international engineering standards before dispatch:
- Optical Emission Spectrographic Verification: Direct-reading spectrometers verify the exact elemental chemistry of every melt prior to casting, ensuring carbon, chromium, nickel, and molybdenum contents conform strictly to ASTM and EN specifications.
- Non-Destructive Ultrasonic & Dye Penetrant Flaw Detection: High-stress casing volutes, suction flanges, and impeller hubs undergo ultrasonic testing (UT) and liquid penetrant testing (PT) to verify zero internal porosity, shrinkage cavities, or micro-cracks.
- 100% Hydrostatic Casing Pressure Testing: Every completed pump casing is subjected to hydrostatic pressure testing at 1.5 times the maximum design pressure (2.4 MPa / 24 bar for 1.6 MPa rated casings). Pressure is held continuously for a minimum 30-minute dwell duration, verified by digital data loggers to confirm zero pressure decay or fluid weeping.
- Acid Immersion Corrosion Rate Validation: Material sample coupons from each alloy heat undergo standardized laboratory immersion testing in boiling acid test solutions in accordance with ASTM G28 / ASTM A262 Practice E, confirming corrosion rates remain well within certified tolerance boundaries.
- Dynamic Balancing & Closed-Loop Performance Testing: Impellers are dynamically balanced to ISO 1940 Grade G2.5, and fully assembled pump sets are tested on digitized hydraulic test loops to ISO 9906 Grade 2B standards to verify certified flow, head, efficiency, and NPSHr curves.
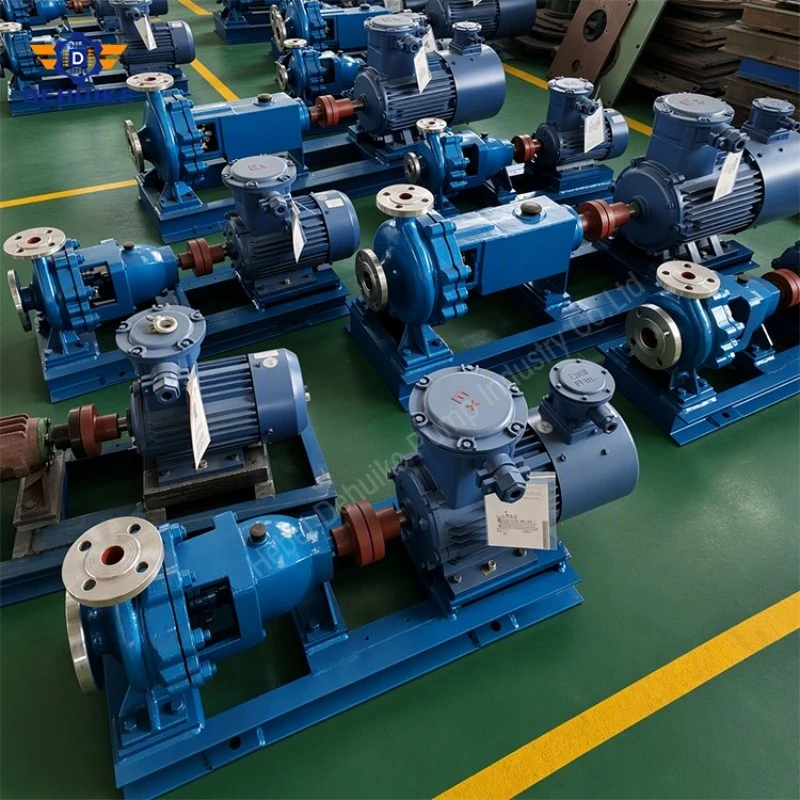
Global Heavy Chemical, Mining Acid-Leaching, and Fertilizer Plant Deployments Across 90+ Countries
The long-term industrial reliability of the Acid Resistant Chemical Pump line is demonstrated across thousands of active installations spanning North America, Europe, Southeast Asia, the Middle East, South America, and Africa. Serving industrial fluid-handling operators in more than 90 countries worldwide, our equipment operates in critical continuous-process infrastructure:
- Industrial Fertilizer & Chemical Synthesis Complexes: Delivering continuous phosphoric acid slurry transfer, concentrated nitric acid injection, and ammonium sulfate brine circulation in large-scale fertilizer plants across Southeast Asia and the Middle East.
- Hydrometallurgical Mining Leaching Projects: Handling sulfuric acid pregnant leach solutions (PLS), copper and nickel electrowinning electrolytes, and aggressive autoclave discharge streams in mining operations across South America and Central Africa.
- Flue Gas Desulfurization & Acid Gas Scrubbing: Pumping acidic limestone slurries, hydrochloric acid scrubber blowdown, and sulfur dioxide absorption liquor in thermal power generation and metallurgical smelting facilities.
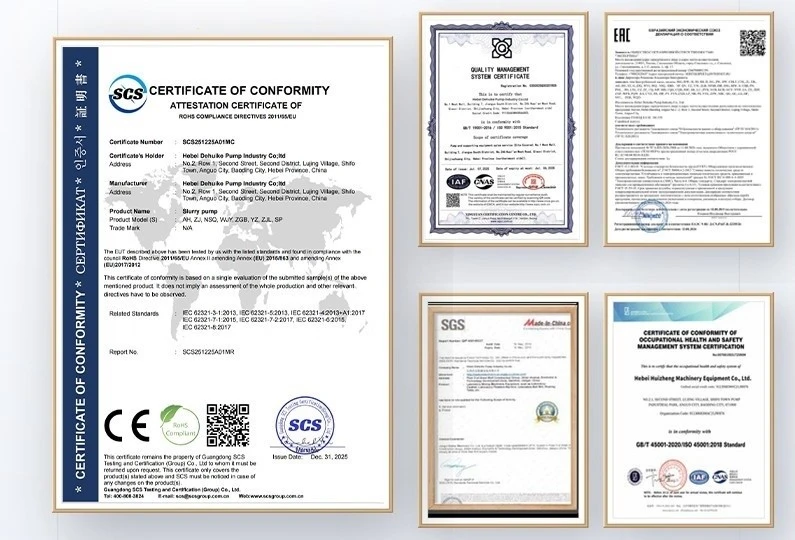
- Comprehensive International Certification Compliance: Manufacturing operations adhere strictly to certified ISO 9001 quality management frameworks, reinforced by EAC (Eurasian Conformity) certification for Eurasian customs territories and RoHS environmental compliance, ensuring seamless global customs clearance and regulatory acceptance.
Severe Inorganic Acids, Spent Acid Regeneration, and Acid Gas Scrubbing Loops
Engineered for versatile operational resilience across diverse industrial environments, the Acid Resistant Chemical Pump is deployed across six primary industrial fluid handling sectors:
- Sulfuric & Nitric Acid Processing: Safely circulating commercial sulfuric acid solutions (from dilute 10% to concentrated 98% sulfuric acid across ambient to elevated temperatures) and nitric acid solutions in dye synthesis, explosives, and chemical fertilizer lines.
- Hydrochloric Acid & Chlorinated Solutions: Pumping pickling liquor, regenerated acid, and aqueous hydrochloric solutions utilizing specialized duplex stainless steels or nickel-based superalloys.
- Phosphoric Acid Wet-Process Manufacturing: Handling raw phosphoric acid, gypsum slurry filtration feeds, and concentration evaporator circulation in fertilizer manufacturing plants.
- Spent Acid Regeneration & Recycling: Transferring spent alkylation acid, hazardous acid sludges, and waste acid effluent across continuous recycling and thermal recovery furnaces.
- Metal Surface Treatment & Pickling Lines: Circulating continuous mixed-acid pickling baths (hydrofluoric-nitric acid) for stainless steel wire, strip, and tube manufacturing plants.
- Industrial Wastewater Neutralization: Conveying heavy-metal acidic wastewater, chemical dosing neutralization streams, and chemical effluent clarifier feeds.
Company Strengths: Vertically Integrated Heavy Acid Equipment Fabrication & 30+ Years Heritage
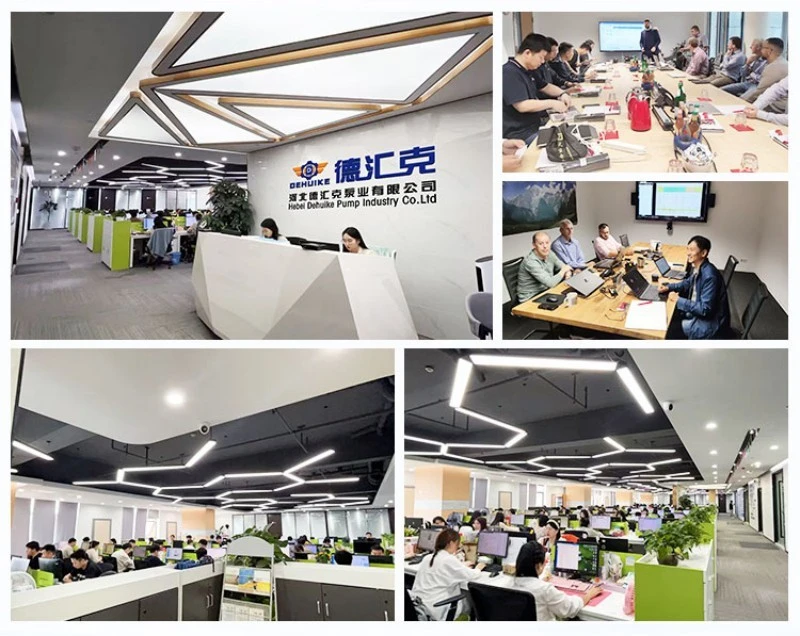
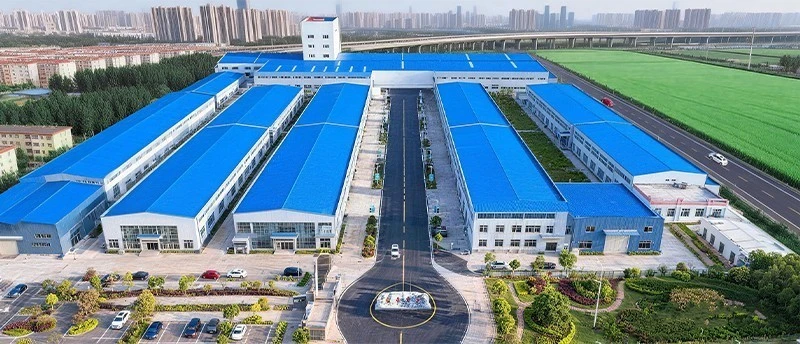
Hebei Dehuike Pump Industry Co., Ltd. represents an elite industrial machinery manufacturing entity that unites specialized acid-handling metallurgy, precision hydrodynamic research, and automated production tooling under one roof. With more than 30 years of dedicated manufacturing experience in severe chemical fluid handling, our production facilities deliver reliable fluid solutions to industrial processing complexes in over 90 sovereign nations worldwide.
Our factory infrastructure features fully independent metallurgical casting autonomy, operating advanced induction melting furnaces and computer-controlled silica sol molding lines. Because we control all casting operations in-house rather than outsourcing to commercial jobbing foundries, our metallurgists enforce strict grain boundary purity, preventing the macro-inclusions and internal shrinkage cavities that cause premature acid penetration. Standardized component interchangeability across our product range lowers customer spare parts inventory costs by more than thirty percent, providing unmatched commercial value across multi-pump plant installations.
To ensure seamless international project procurement, every manufactured unit is backed by our comprehensive 2-year (24-month) whole-machine equipment warranty, safeguarding against structural casting defects, shaft failure, and hydraulic non-conformance (consumable mechanical seal faces, O-rings, and gaskets excluded). Commercial dispatches are managed via professional global freight logistics, accommodating expedited air transport (50 kg to 500 kg for critical breakdown components) and ocean container shipping (500 kg and above for heavy capital projects), quoted under Incoterms 2020 on FOB and CIF destination port agreements.
Hot Tags: acid resistant chemical pump, China acid resistant chemical pump manufacturers, suppliers, factory