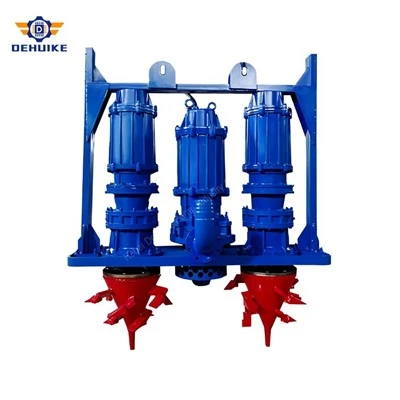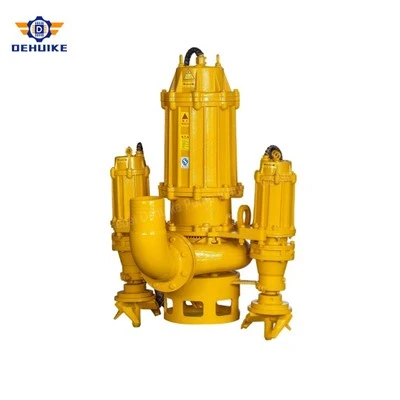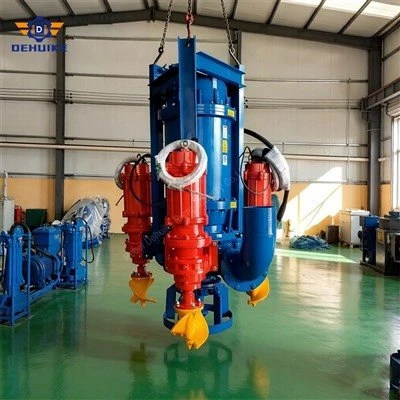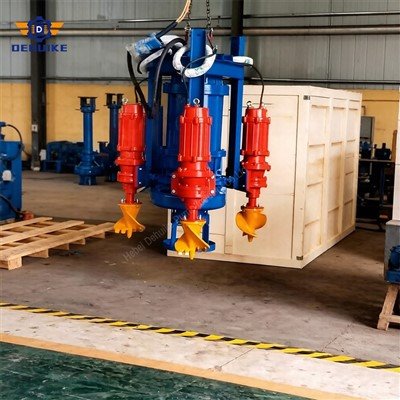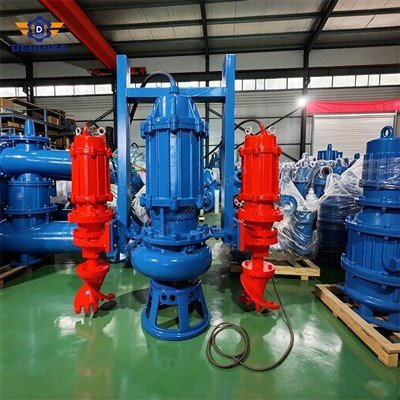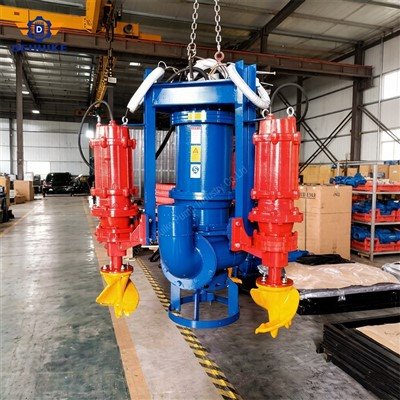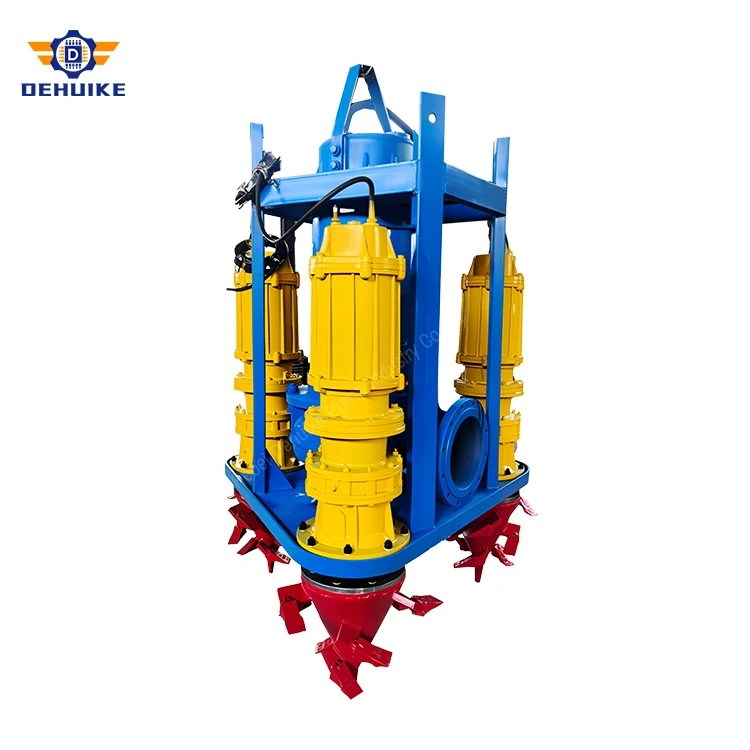
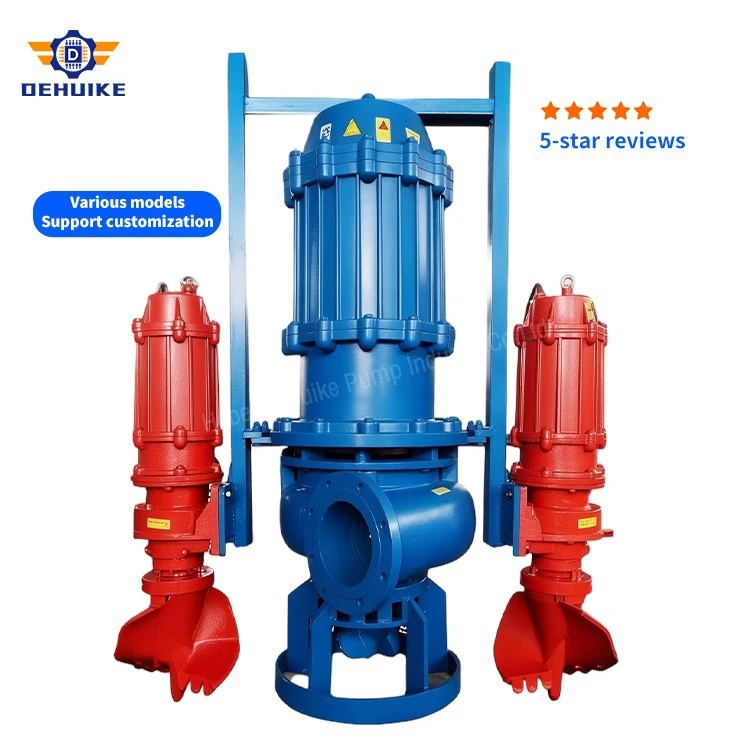
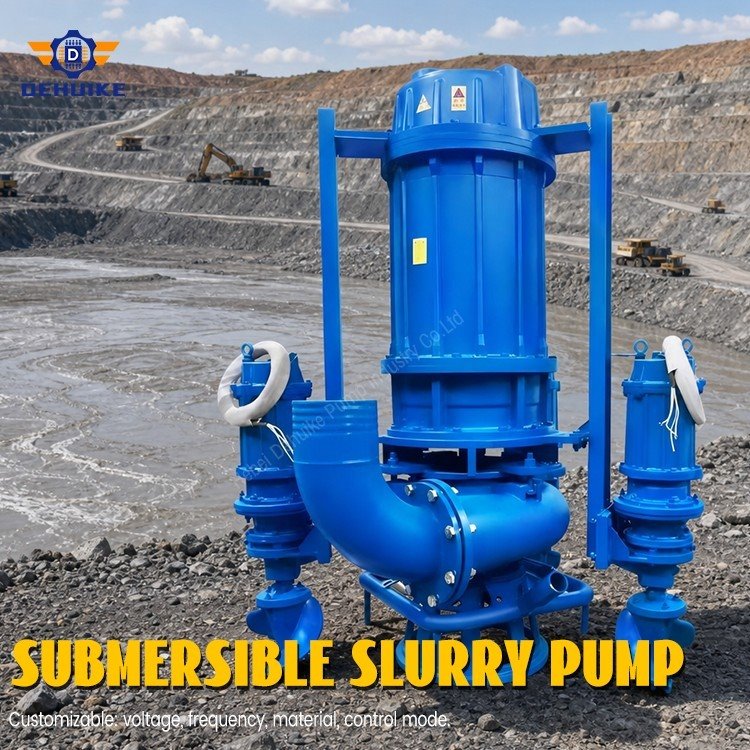
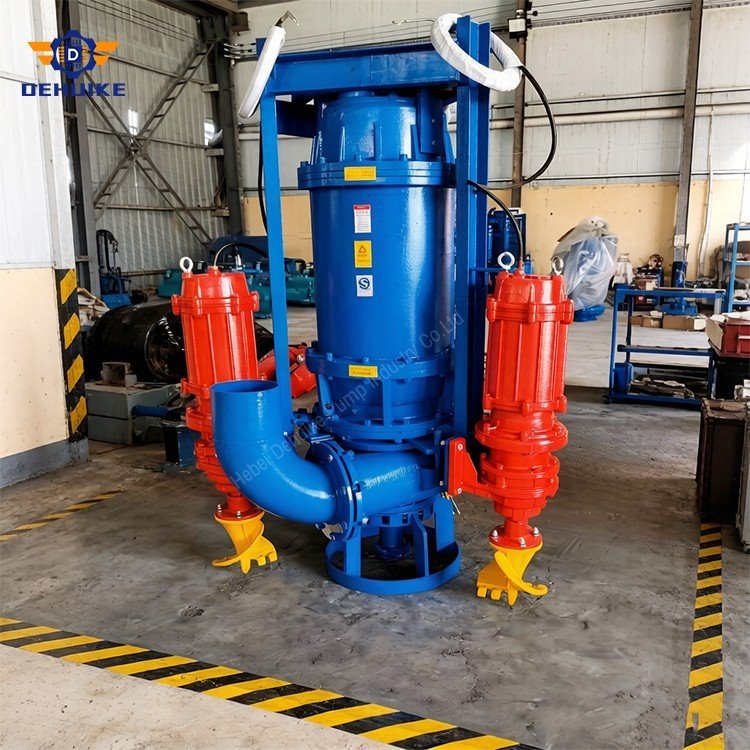
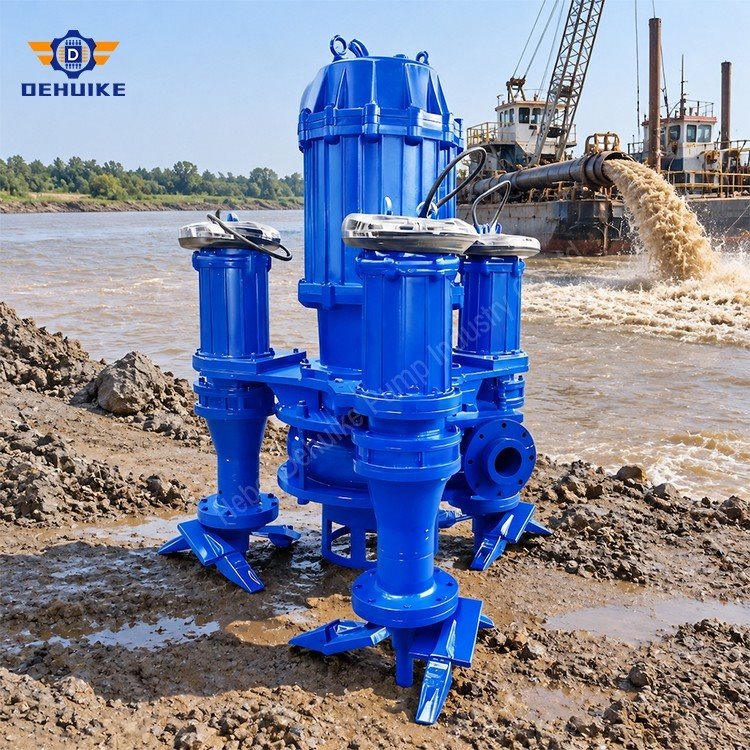
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of submersible mining slurry pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk submersible mining slurry pump for sale here from our factory. Also, pricelist is available.
Introduction - Hydraulic Architecture and Operational Principles in Severe Mineral Slurry Extraction
Extreme Mineral Slurry Challenges: Open-pit excavations, underground haulage sumps, mineral flotation circuits, and tailings retreatment facilities routinely confront extreme operating conditions when handling multi-phase mixtures of crushed ore, quartz fines, flotation reagents, and abrasive metallurgical grit. Traditional surface-mounted centrifugal pumps operating on dry ground require complex suction intake manifolds, vacuum priming apparatus, or deep civil pump rooms. In deep underground mine sumps or fluctuating tailings dams, long dry suction lines frequently suffer from vapor locking, cavitation, and air binding as water levels vary. The Submersible Mining Slurry Pump fundamentally resolves these operational vulnerabilities by operating entirely immersed within the collection sump, eliminating atmospheric priming requirements and suction pipe friction entirely.
Submerged Hydraulic Advantages over Surface Stations: Direct submerged operation delivers significant structural and mechanical efficiencies for mining infrastructure. By submerging both the hydraulic wet end and the heavy electric motor beneath the liquid surface, the equipment eliminates civil pump house construction costs, priming ejectors, and cumbersome foot valves. Atmospheric head acts directly upon the submerged suction nozzle, providing positive suction pressure that broadens the cavitation-free operating window even when pumping dense mineral pulps with specific gravities exceeding 1.35 kg/dm³. Moreover, because the entire pump body is submerged, the surrounding liquid provides continuous external convective cooling across the motor shell, preventing stator overheating during high-load processing cycles.
Settled Solid Agitation and Rheological Dynamics: Mineral slurry conveyance involves multi-phase rheology where suspended ore solids continuously attempt to settle out of suspension under gravitational pull. When pumps operate intermittently in mine sumps, coarse particles settle into hard, consolidated cakes around the suction intake. Standard dewatering pumps quickly starve and burn out when attempting to ingest these consolidated beds. By incorporating a dedicated rotating mechanical agitator ahead of the main suction eye, a purpose-built Submersible Mining Slurry Pump mechanically breaks up compacted sediment, blending it into a fluid mixture that passes freely through wide internal casing waterways.
Manufacturing Heritage and Engineering Foundation: Backed by over thirty years of specialized industrial pump manufacturing, Hebei Dehuike Pump Industry Co., Ltd. (DHK Pump) engineers the standardized NSQ series of submersible mining slurry pumps. Operating with high-chromium alloy wet ends (Cr27) and IP68 hermetic motor enclosures, our equipment provides mining corporations and mineral processing plants across more than 50 export countries with durable, high-efficiency slurry handling assets.
Specifications & Technical Data - Comprehensive Performance Selection Matrix
Standardized NSQ Mining Platform: The standardized NSQ equipment series encompasses an extensive hydraulic spectrum designed to meet diverse mining duties, ranging from compact localized sump dewatering to large-scale tailings reclamation. Operating speeds, discharge calibers, and motor powers are matched to maintain stable fluid velocity and prevent line choking.
2.1 Certified Operational Ratings across the NSQ Submersible Slurry Matrix
Verified Model Performance Matrix: The performance matrix below details certified engineering data across 16 representative small, intermediate, and heavy-duty industrial models, verified through rigorous factory water calibrations:
2.2 Slurry Density Correction and Critical Deposition Sizing Discipline
Slurry Specific Gravity and Power Derating: Pumping mineral ore slurries requires specific hydraulic corrections relative to clear water. As solids concentration increases, the specific gravity (SG) of the mixture rises, increasing required shaft power in direct proportion to mixture density. Operating engineers must apply power correction factors using the relationship:
Velocity Window Rules: P_slurry = P_water x SG_mixture x 1.15 (service safety factor). Motor ratings must be sized to prevent overload trips during unexpected density surges. Furthermore, pipeline sizing must guarantee that line velocity stays strictly between 2.8 and 4.0 m/s depending on particle d50. Velocities below 2.5 m/s result in stationary bed deposition, causing rapid pipeline clogs, whereas velocities exceeding 4.5 m/s exponentially accelerate internal pipe wall erosion.
Optimal Operating Point: Operating units should always be aligned within 80% to 110% of their Rated Optimal Efficiency Point (BEP). Sustained operation far to the left of BEP induces aggressive hydraulic recirculation within the cutwater zone, accelerating localized casing erosion, whereas continuous operation beyond BEP increases motor thermal loading and risks cavitation on impeller inlet blades.
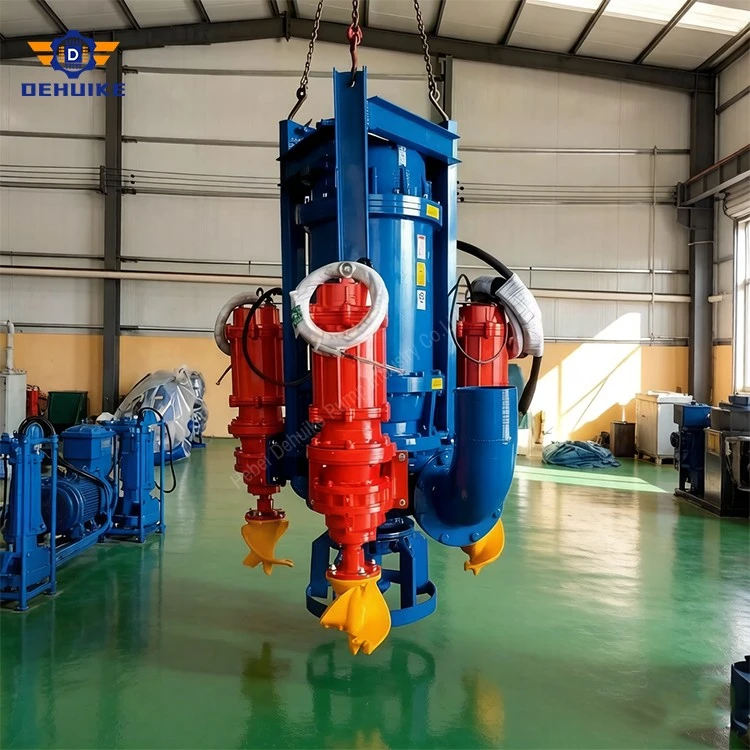
Product Details - Mechanical Subassembly Anatomy, Metallurgy, and Sealing Integrity
Subassembly Engineering: The mechanical architecture of the Submersible Mining Slurry Pump is engineered specifically to survive high-impact slurry erosion, heavy particulate abrasion, and extreme underwater hydrostatic pressure.
Extra-Thick High-Chromium Alloy Wet End (Cr27 / 58-62 HRC): All components in direct contact with mineral slurry-including the spiral volute casing, enclosed slurry impeller, bottom mechanical agitator, and suction liner plate-are cast from high-chromium white cast iron (Cr27 / ASTM A532 Class III Type A). The microstructure consists of extremely hard eutectic M7C3 chromium carbides (1,200 to 1,400 HV microhardness) supported within a heat-treated martensitic matrix, achieving a bulk hardness of 58 to 62 HRC. This metallurgy resists both aggressive gouging abrasion from sharp crushed ore and micro-cutting from fine silica tailings.
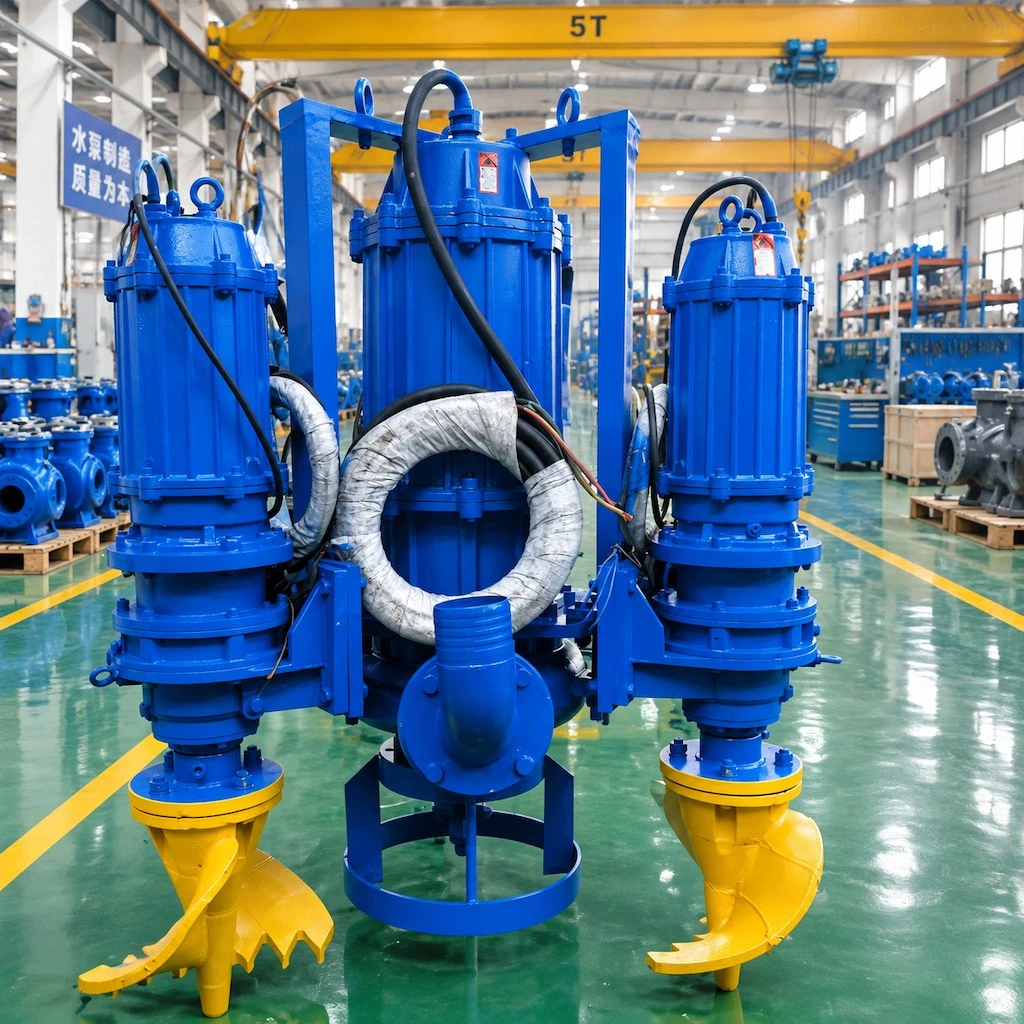
Integrated Submerged Mechanical Agitator: Mounted below the main impeller on an extended rotor shaft, an auxiliary rotating mechanical agitator features heavy pitched cutting blades. The agitator churns into settled mineral sediments, spraying pressurized slurry jets that fluidize compacted sand and ore fines, ensuring a high-density, homogenous slurry enters the pump intake.
Tandem Double Mechanical Shaft Seals in Oil Buffer Reservoir: Isolation between the wet hydraulic end and the electric motor is maintained by a tandem dual-cartridge mechanical seal assembly operating in an independent oil reservoir. Seal running faces are precision-lapped from sintered silicon carbide versus solid tungsten carbide. The oil bath provides continuous hydrodynamic lubrication and thermal dissipation, completely preventing slurry ingress even at submerged water depths up to 30 meters.
Heavy-Duty IP68 Submersible Electric Motor with Class H Insulation: The integral three-phase electric induction motor is housed within a heavy cast iron waterproof shell rated IP68 for continuous underwater duty. Stator windings feature Class H insulation (rated to 180°C) and vacuum pressure impregnation (VPI) treatment, providing exceptional thermal endurance and resistance to moisture condensation.
Integrated Thermal and Moisture Leakage Detection Sensors: The motor assembly incorporates built-in thermal sensors (PT100 or bimetallic switches) embedded directly within the stator windings to guard against overheating, alongside optical moisture probes positioned within the oil buffer chamber and motor housing to detect water ingress instantly, triggering automatic trip protection before electrical winding damage occurs.
Heavy-Duty Alloy Rotor Shaft and High-Capacity Bearings: The high-tensile 40Cr forged alloy steel shaft is supported by paired heavy-duty angular contact ball bearings and cylindrical roller bearings, designed with an L10 bearing life exceeding 50,000 operational hours under continuous radial and axial slurry thrust loads.
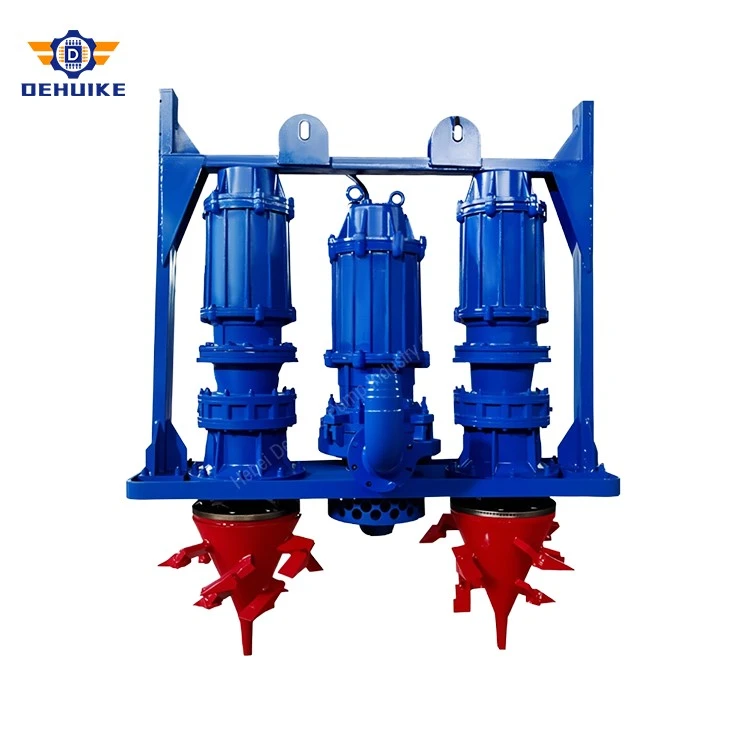
Features / Equipment Characteristics - Submerged Agitation, Compact Footprint, and Mining Reliability
Core Operational Features: The engineering features of the Submersible Mining Slurry Pump provide mining operators, plant engineers, and civil contractors with clear operational advantages over legacy vertical cantilever or horizontal slurry installations.
Elimination of Civil Pump House and Priming Infrastructure: Unlike vertical cantilever sump pumps that require deep civil structures, long drive shafts, and multiple support bearings, the submersible unit operates directly suspended inside the sump. This eliminates shaft whip, structural alignment issues, and costly sump excavation works.
High-Concentration Slurry Extraction up to 60% Solids: Equipped with its bottom rotating agitator, the pump delivers high solids concentrations (up to 60% by weight and 45% by volume), allowing mining operations to reclaim dense mineral sands and tailings without needing external high-pressure water jetting trucks.
Versatile Sump Installation and Auto-Coupling Retrieval: The pump accommodates multiple installation configurations: resting directly on a flat sump bottom via an integral support strainer, suspended from a crane hoist cable, or mounted on dual stainless steel guide rails with an auto-coupling discharge pedestal for rapid retrieval.
Low Acoustic Noise and Submerged Thermal Dissipation: Operating completely submerged underneath the water table suppresses hydraulic turbulence and motor noise, keeping plant acoustic emissions well below 70 dB(A) at 1 meter, dramatically improving underground mine working conditions.
Modular Replacement of Critical Wear Components: Standardized components allow rapid replacement of high-wear parts (impellers, agitators, and front liners) without dismantling the electrical motor chamber, reducing scheduled overhaul times to under two hours.
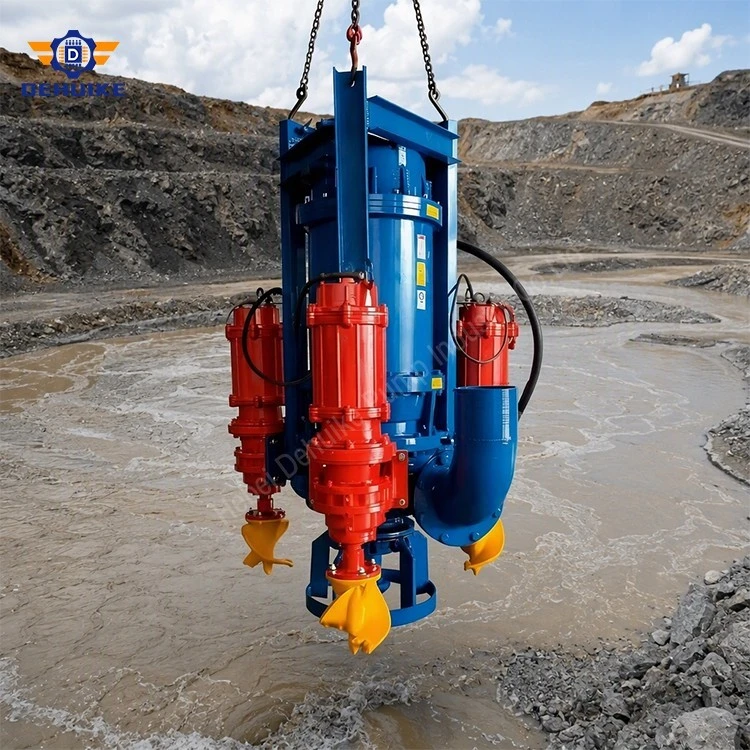
Application - Underground Mining, Mineral Concentrators, Tailings Storage, and Ash Handling
Field Application Scope: Owing to its high wear resistance, integrated mechanical agitation, and robust IP68 submersible sealing, the Submersible Mining Slurry Pump is widely utilized across demanding mining and metallurgical operations:
Underground Mine Drainage and Incline Shaft Dewatering: Handles dirty mine runoff containing heavy drilling mud, rock cuttings, and abrasive quartz sand, pumping slurry from bottom collection sumps to surface settling ponds without requiring underground pump stations.
Mineral Processing Plant Sump Cleanout and Cyclone Feed: Installed in flotation underflow sumps, thickener overflow basins, and cyclone feed collection pits to transfer concentrated mineral pulps containing copper, gold, iron, nickel, and zinc ores.
Tailings Pond Reclamation and Settling Basin Desilting: Transports settled tailings slimes and abrasive sand deposits from tailings dams, reclamation ponds, and emergency spill catchments to filtration plants or secondary reprocessing circuits.
Coal Ash Slurry and Steel Mill Slag Granulation Pits: Handles abrasive bottom ash and fly ash slurry in coal-fired power stations and metallurgical blast furnace slag granulating pits, withstanding thermal shocks up to 60°C.
Aggregate Quarry Wash Plants and Civil Caisson Desilting: Deploys in aggregate wash plants, alluvial gold dredging pits, and construction caissons to evacuate heavy mud, sand, and gravel deposits without clogging.
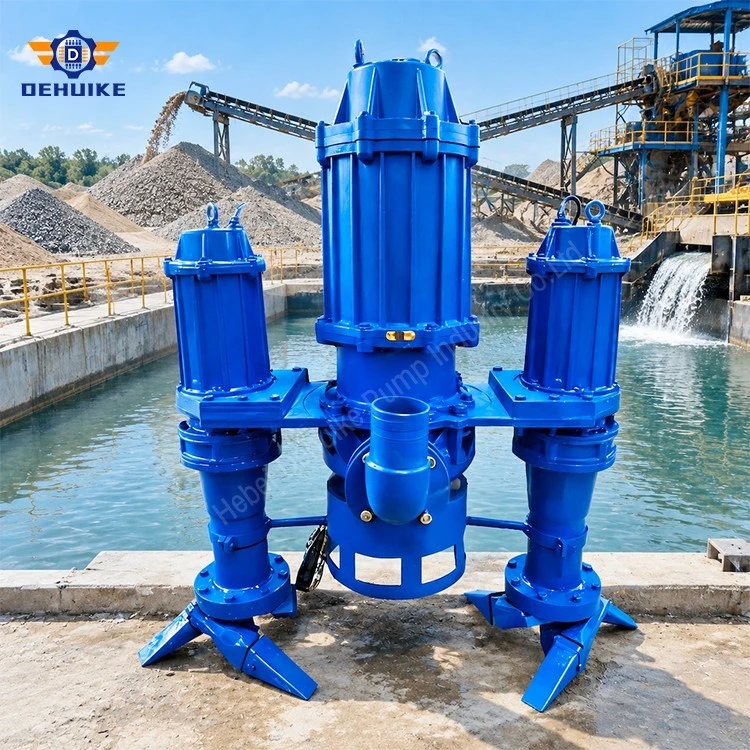
Production Process & Quality Assurance
Stringent Quality Assurance Protocol: Manufacturing quality at Hebei Dehuike Pump Industry Co., Ltd. is governed by certified quality management systems from raw furnace melt through final submerged testing.
Precision Induction Melting and Spectrometric Chemical Analysis: High-chromium white iron alloys are melted in medium-frequency electric induction furnaces under digital thermal monitoring. Molten chemistry is verified via vacuum optical emission spectrometry prior to tapping at 1,480°C, ensuring carbon, chromium (26.0–28.0%), silicon, manganese, and molybdenum conform strictly to ASTM A532 Grade III Type A specifications.
Automated Furan Resin Sand Molding for Hydraulic Smoothness: Pump volutes, impellers, and agitator castings are formed using automated furan resin sand molding. Chemically bonded sand cores provide high dimensional rigidity, resisting molten alloy washing and producing cast waterways with exceptionally smooth surfaces and tight wall thickness tolerances.
Controlled Thermal Hardening and Tempering Heat Treatment: Raw wear castings undergo high-temperature furnace annealing followed by controlled air-quench hardening and tempering cycles, converting the microstructure into hardened martensite containing dispersed eutectic chromium carbides with uniform hardness between 58 and 62 HRC.
Multi-Axis Horizontal CNC Precision Machining: Critical bearing registers, mechanical seal cavities, and motor stator fits are machined on multi-axis CNC horizontal boring centers in unified setups, maintaining coaxial alignment within ±0.015 mm to ensure perfect mechanical seal face parallelism.
Factory Submerged Proof Testing and Dynamic Balancing: Every assembled pump unit undergoes submerged hydrostatic pressure testing at 1.5 times rated working pressure, high-voltage dielectric insulation tests (2,500V for 1 minute), and dynamic balancing of all rotating assemblies to ISO 1940 Grade G2.5, ensuring vibration velocities remain well below 2.5 mm/s RMS.
Our Service & Commercial Advantages
-
Manufacturer-Direct Commercial Partnership: Procuring fluid handling machinery directly from Hebei Dehuike Pump Industry Co., Ltd. connects international mining operators, contractors, and distributors with an established engineering manufacturer supported by extensive foundry and machining capabilities.
30+ Years Manufacturing Heritage and Rapid Deployment: With over 30 years of specialized manufacturing experience, Dehuike operates an 8,000+ square meter heavy industrial facility supported by an audited network of more than 900 certified industrial supply partners. This comprehensive manufacturing base allows standard bare units and complete automated pump skids to be assembled and dispatched within 10 to 15 business days.
Custom Engineered Control Packages and Auto-Coupling Systems: Our engineering division works closely with project contractors to evaluate slurry specific gravity, calculate pipeline friction head losses, and deliver custom packages including automated dual guide rail systems, lifting chains, specialized power cables, and intelligent starter control cabinets (DOL, Star-Delta, Soft-Starter, or VFD).
Comprehensive 24-Month Manufacturer Warranty: Every Submersible Mining Slurry Pump is backed by Dehuike's comprehensive 24-month (2-year) factory equipment warranty covering the complete pump machine (excluding standard consumable wear components like impellers, agitators, and casing liners).
Hot Tags: submersible mining slurry pump, China submersible mining slurry pump manufacturers, suppliers, factory