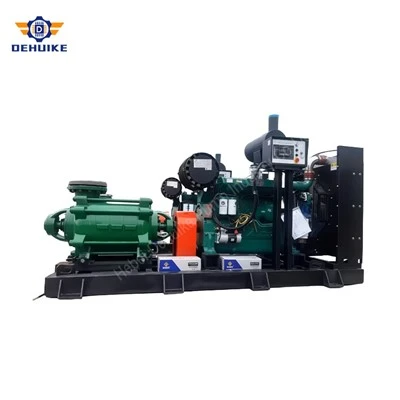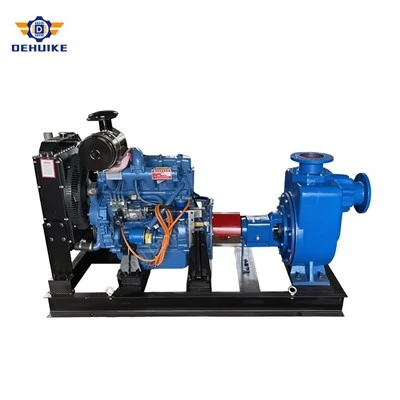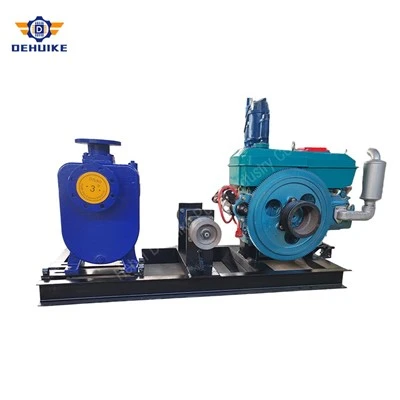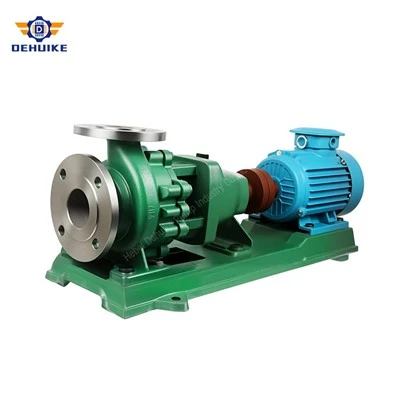
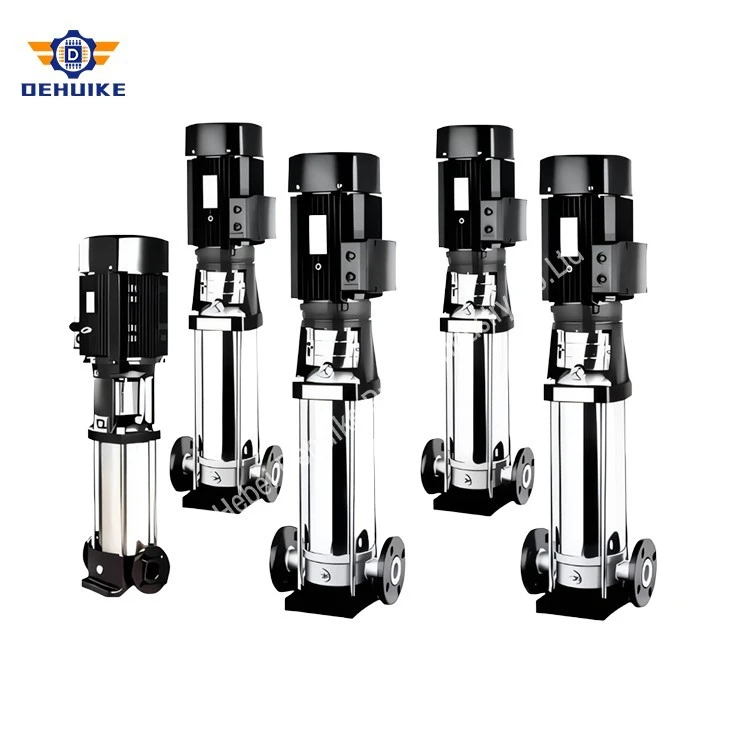
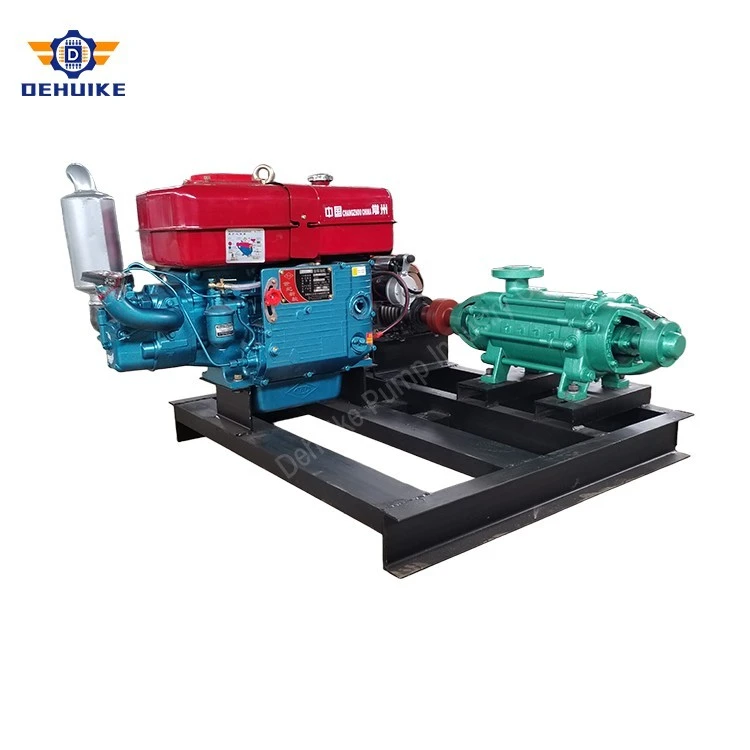
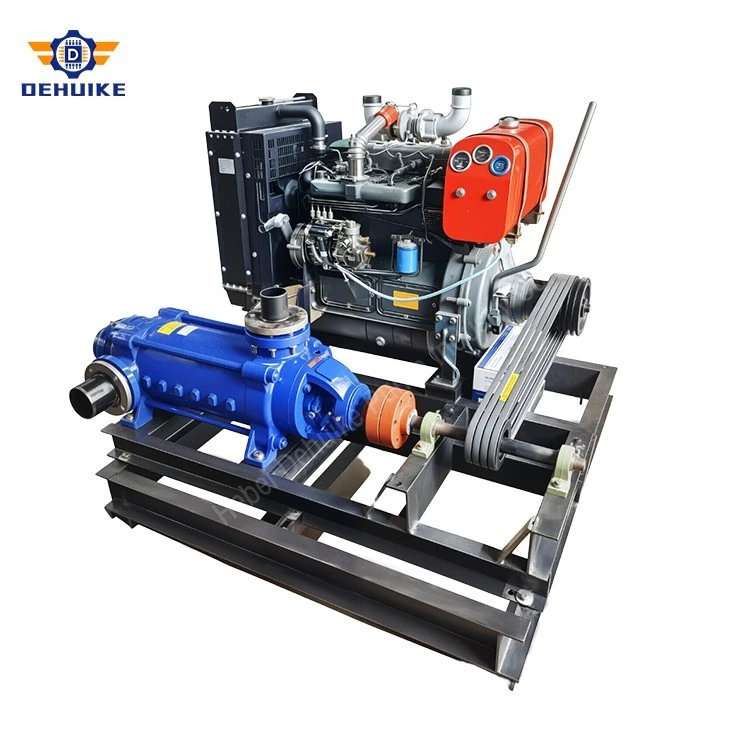
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of multistage water supply pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk multistage water supply pump for sale here from our factory. Also, pricelist is available.
Long-Distance Pressure Boosting Dynamics
Municipal water distribution networks, heavy industrial manufacturing campuses, elevated commercial balancing reservoirs, and regional water transfer pipelines face severe hydraulic transport challenges. Moving large volumes of treated potable water or industrial process water across hilly topography, extended pipeline corridors, and high-rise pressure zones generates immense friction losses and static head requirements. When delivery requirements demand pressures exceeding 1.0 to 2.5 MPa, standard single-stage centrifugal transfer pumps reach their mechanical limits; excessive impeller diameters and high tip velocities produce turbulent fluid shear, accelerated casing wear, and low energy efficiency.
The heavy-duty Multistage Water Supply Pump solves these fluid-distribution challenges through a series-arranged hydraulic architecture. Rather than relying on a single high-velocity impeller, water flows sequentially through multiple matched enclosed impellers and stationary diffuser bowls mounted along a common horizontal drive shaft. Each successive stage imparts an incremental velocity and pressure boost, accumulating total dynamic heads up to 273 meters (2.68 MPa) while maintaining stable hydraulic efficiency and minimal mechanical vibration. This modular sectional approach provides water authorities and plant engineers with versatile pressure zoning solutions tailored precisely to site elevation profiles and network flow demands.
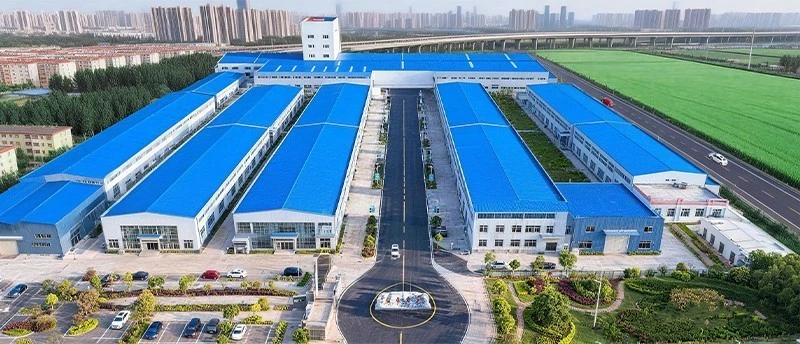
Engineered and fabricated by Hebei Dehuike Pump Industry Co., Ltd. (operating in global markets under the DHK Pump mark), our DA1 series sectional multistage water supply pumps draw upon more than 30 years of specialized metallurgical casting, precision machining, and fluid machinery packaging. Operating from an integrated modern campus exceeding 8,000 m² and reinforced by an audited cooperative supply chain of 900+ certified industrial component suppliers, Dehuike delivers high-reliability clean water distribution packages to municipal utilities, industrial plants, and commercial complexes across 50+ countries worldwide.
Sectional Ring Architecture
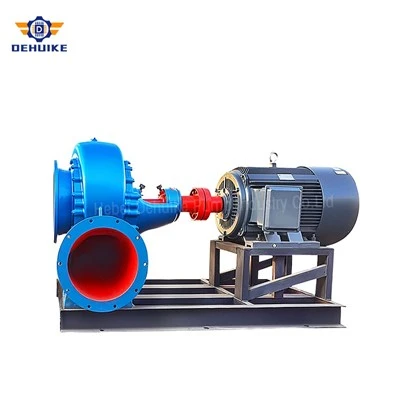
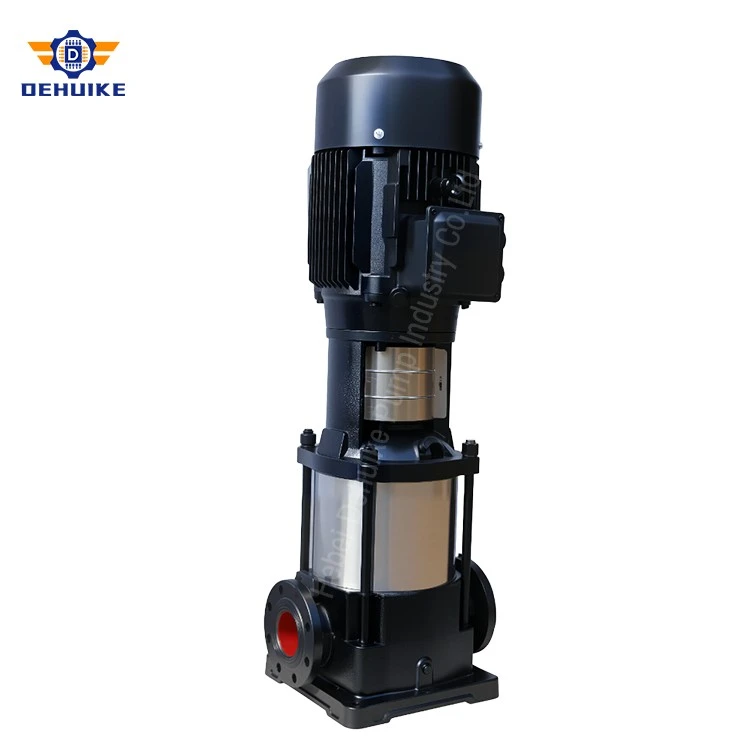
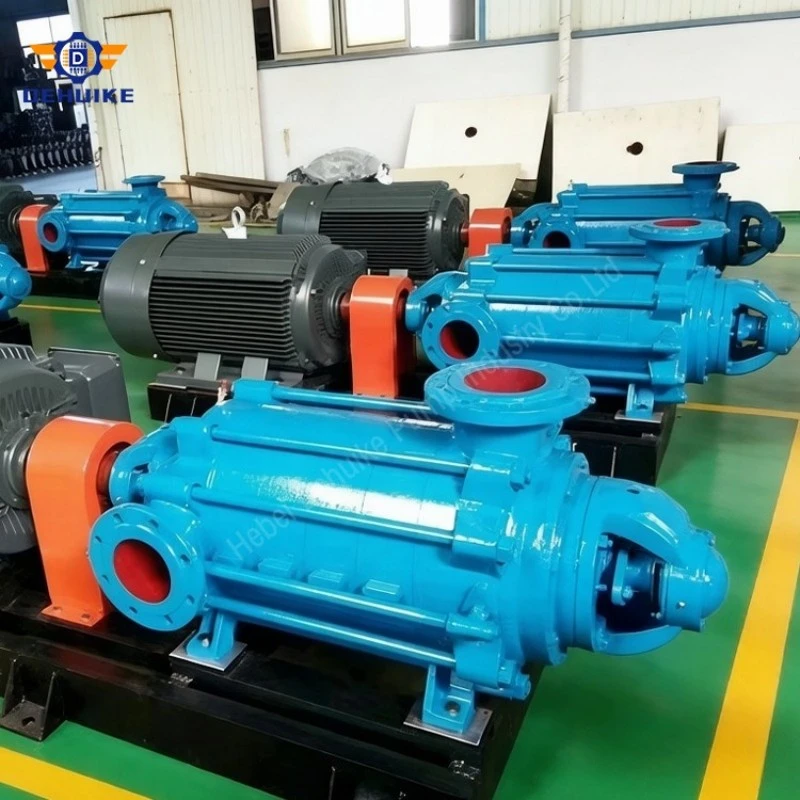
A rigorous mechanical teardown of our DA1 series horizontal Multistage Water Supply Pump reveals the specialized structural architecture required to maintain hydraulic equilibrium and pressure containment across high-differential municipal distribution networks. Key mechanical subsystems are engineered for decades of continuous 24/7 service:
Segmented Ring-Section Casing with High-Tensile Tie Rods: The pressure containment boundary comprises an intake suction casing, modular intermediate stage bowls, and a heavy discharge delivery head cast from high-density gray cast iron (HT250 / Class 35) or ductile nodular iron (QT450-10). These individual stage rings are aligned via precision male-female spigot registers with elastomeric O-ring seals, and clamped together longitudinally by heavy high-tensile alloy steel tie bolts. This sectional design allows exact hydraulic matching by varying the stage count while facilitating straightforward replacement of individual worn stage rings during scheduled plant overhauls.
Precision-Cast Enclosed Impellers & Radial Diffusers: Every hydraulic stage features a precision-cast enclosed multi-vane impeller matched to a stationary radial diffuser ring. Impeller waterways and diffuser guide vanes are polished to mirror-smooth hydraulic finishes, minimizing boundary layer turbulence and optimizing kinetic-to-pressure energy conversion. The radial diffuser channels direct fluid smoothly into the eye of the subsequent stage with minimal vortex recirculation.
Automated Hydraulic Balancing Mechanism (Balancing Drum / Disc): Because all stage impellers face in the same direction, cumulative hydraulic forces generate massive axial thrust directed toward the suction inlet. Our pumps integrate a self-regulating hydraulic balance mechanism at the high-pressure discharge end. High-pressure water bleeds across a calibrated radial clearance into an internal balance chamber, automatically shifting the rotor axially to maintain an optimal lubricating fluid film between rotating and stationary balance faces, neutralizing axial thrust without overloading drive bearings.
Dual Water-Cooled Bearing Pedestals with Oil-Ring Lubrication: The rigid alloy rotor shaft is supported at both ends by heavy-duty spherical roller bearings (or precision angular contact ball bearing sets) housed in rigid cast-iron bearing brackets isolated from the liquid casing. The housings feature oil-ring splash lubrication reservoirs and internal cooling jackets, maintaining lubricant operating temperatures safely below 65°C even during continuous full-load summer operation.
Flexible Shaft Sealing Architecture (Gland Packing vs. Mechanical Seal): To suit diverse operating environments, the stuffing box can be fitted with traditional braided PTFE-graphite gland packing with lantern ring water injection (preferred for remote municipal stations where gradual dripping provides visual confirmation) or balanced single/cartridge mechanical seals with silicon carbide friction pairs for zero-leakage factory utility headers.
Technical Parameters
Proper engineering selection of a Multistage Water Supply Pump requires matching required pipeline flow rates, total dynamic discharge heads, suction lift margins, and electric driver ratings against verified performance curves. Dehuike Machinery manufactures the DA1 series across five primary frame sizes, delivering flow rates up to 162 m³/h and dynamic heads up to 273 meters across ten-stage configurations.
The technical parameter table below summarizes standardized operational ratings for representative DA1 series ten-stage clean water supply models, highlighting flow capacity, developed head, operating speed, motor power, and suction requirements:
Hydraulic Sizing & System Pressure Zoning Protocol: When selecting a Multistage Water Supply Pump for municipal distribution or factory utility loops, system designers must align operating flow regimes within 85% to 105% of the Rated Optimal Efficiency Point (BEP). Operating significantly to the left of BEP generates excessive internal recirculation and increases axial thrust on the balancing mechanism, whereas running excessively far to the right increases Net Positive Suction Head Required (NPSHr), heightening cavitation risk. Plant engineers should calculate Net Positive Suction Head Available (NPSHa)-by factoring atmospheric barometric pressure, suction reservoir water level, fluid operating temperature, and intake pipe friction losses-to maintain a safety margin of at least 1.0 meter above catalog NPSHr.
Precision Metallurgy
Manufacturing a reliable high-head Multistage Water Supply Pump capable of operating continuously under pressures exceeding 2.5 MPa requires rigorous metallurgical control, precision multi-axis CNC machining, and automated dynamic balancing. At Dehuike, every multistage pump progresses through an integrated production flow:
Electric Induction Smelting & Chemical Spectrographic Verification: Raw materials are smelted in medium-frequency electric induction furnaces using high-purity virgin pig iron, selected steel scrap, and specialized alloying additions. Prior to tapping, molten metal chemistry is analyzed via optical emission spectrometry (OES) to ensure optimal carbon, silicon, and manganese ratios, producing dense pearlitic microstructures in gray iron (HT250) or spheroidal graphite nodularity exceeding 90% in ductile iron (QT450-10) without porosity.
Furan Resin Sand Molding of Precision Hydraulic Stage Bowls: Individual stage bowls, suction casings, and discharge covers are formed in rigid furan-bonded resin sand molds. This precision foundry process yields smooth internal water passages with minimal surface roughness, drastically reducing boundary layer friction and ensuring uniform pressure buildup across all ten consecutive stages.
Multi-Axis CNC Machining of Precision Casing Registers: All critical mating surfaces-including male-female spigot registers, O-ring sealing grooves, diffuser locating shoulders, and bearing bracket fits-are machined on heavy horizontal CNC boring centers in single-setup operations. Register concentricity and perpendicularity are maintained strictly within ±0.012 mm, eliminating shaft angular misalignment across the ten-stage stack.
Two-Plane Dynamic Balancing (ISO 1940 Grade G2.5): All cast impellers and balance discs undergo precision machining and computerized two-plane dynamic balancing adhering strictly to ISO 1940 Grade G2.5 standards, eliminating harmonic unbalance forces that could induce shaft deflection at 2950 RPM.
Hydraulic Tie-Bolt Pre-Tensioning & Assembly: During final assembly, high-strength alloy tie rods are tightened using calibrated hydraulic bolt tensioners in an automated cross-pattern sequence. This controlled pre-stressing guarantees leak-tight metal-to-metal stage face sealing under full dynamic operating pressures.
Testing Protocols
Because municipal water transfer and factory utility supply pumps must operate without unexpected shutdowns or pipeline pressure collapse, Dehuike enforces strict quality verification under accredited ISO 9001 governance, supported by international EAC and RoHS product certifications:
Hydrostatic Proof Pressure Containment Testing: Every assembled multistage casing undergoes cold-water hydrostatic pressure testing at 150% of maximum rated design working pressure (reaching test pressures up to 4.2 MPa / 42 bar) for a continuous 30-minute hold period, verifying complete casing density, tie-bolt clamping integrity, and zero flange seepage.
100% Non-Destructive Examination (UT & PT): High-tensile casing tie rods, discharge heads, and shaft forgings undergo 100% ultrasonic flaw inspection (UT) to verify freedom from subsurface voids or micro-cracks. Impeller vanes and balance discs undergo liquid dye penetrant testing (PT) across all high-stress radii.
Closed-Loop Full-Speed Hydraulic Bench Validation: Completed pump assemblies are mounted on our automated computerized closed-loop hydraulic testing station. Calibrated electromagnetic flowmeters, high-frequency dynamic pressure sensors, and digital torque meters record flow, total head, absorbed kilowatt power, and efficiency across multiple throttling points, verifying compliance with ISO 9906 Grade 2B standards.
Mechanical Vibration & Thermal Bearing Run-In: Units undergo full-load mechanical testing to verify balance disc hydraulic equilibrium and monitor bearing housing vibration velocity against ISO 10816-3 Class II limits (maintaining overall RMS vibration strictly below 2.8 mm/s).
Manufacturing Pedigree
Procuring heavy-duty multistage clean water supply machinery requires selecting an established manufacturer with deep metallurgical mastery, precision machining capacity, and responsive international commercial support. DHK Pump provides decisive competitive advantages for water authorities and industrial contractors:
Three Decades of Specialized Fluid Machinery Excellence: Backed by over 30 years of continuous specialized manufacturing experience, Hebei Dehuike Pump Industry Co., Ltd. has perfected multistage centrifugal hydraulic models using advanced Computational Fluid Dynamics (CFD). Our designs optimize hydraulic energy efficiency while maintaining mechanical robustness.
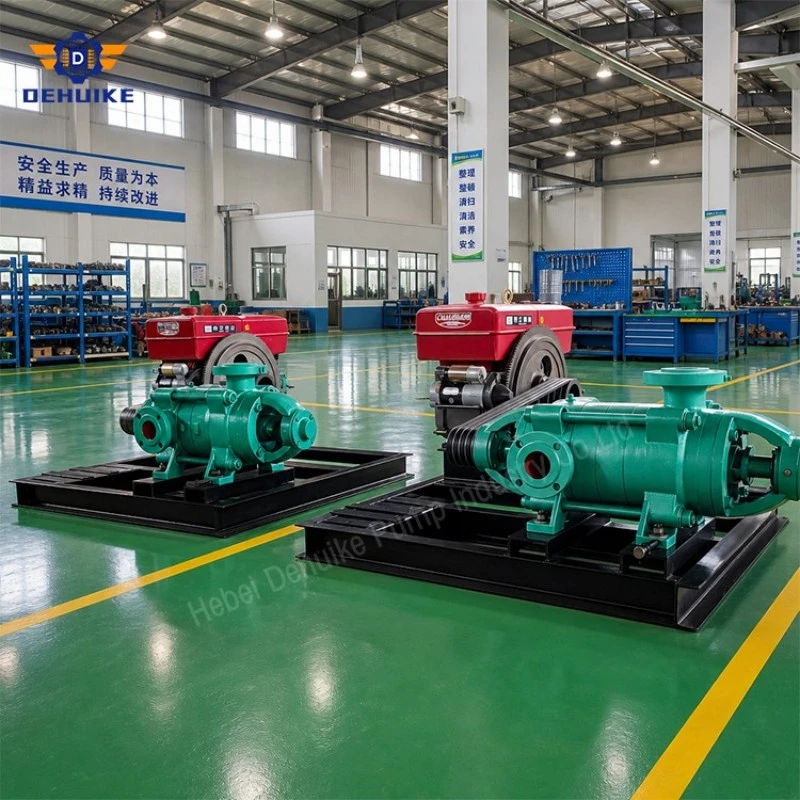
8,000+ m² Modern Integrated Heavy Manufacturing Facility: Our specialized industrial complex houses resin sand molding lines, medium-frequency electric melting furnaces, multi-axis horizontal boring machines, dynamic balancing stations, and automated test bays under one roof, providing complete quality traceability across every production step.
Audited Supply Chain Network (900+ Certified Partners): Leveraging an established cooperative network of 900+ vetted industrial component partners across China, we maintain robust stocks of premium electric motors, heavy-duty mechanical seals, trailer axles, and certified alloy ingots, ensuring reliable production schedules and expedited deliveries.
Comprehensive 24-Month Factory Warranty Commitment: Every complete Multistage Water Supply Pump manufactured by our works carries an official 24-month (two-year) comprehensive factory warranty covering the casing, rotor assembly, bearing bracket, and baseplate against defects in materials and craftsmanship.
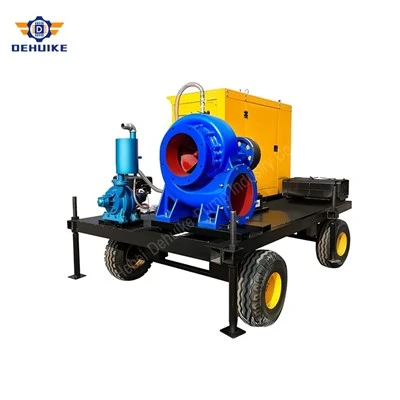
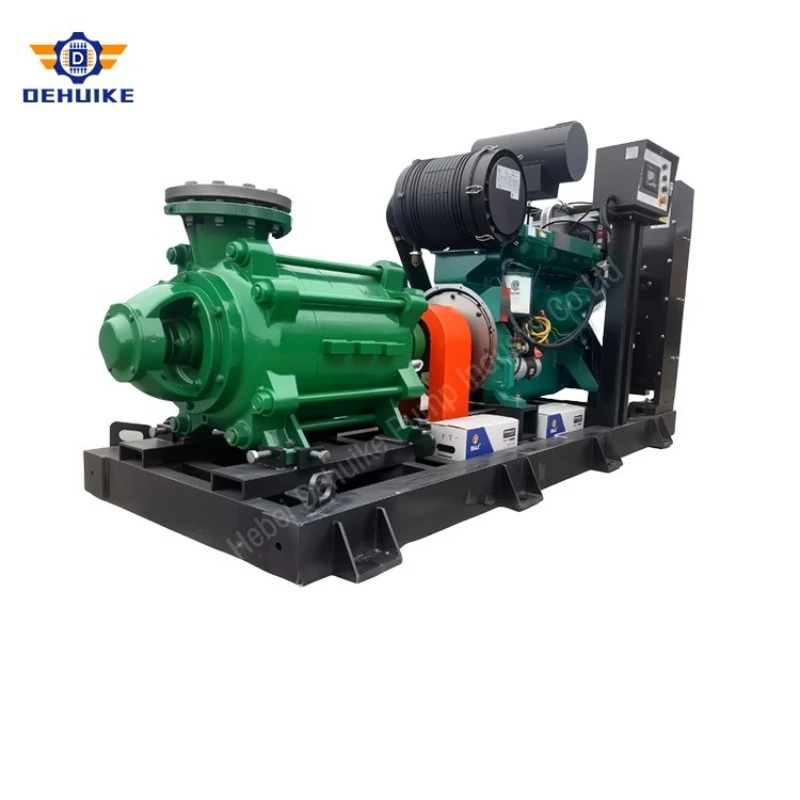
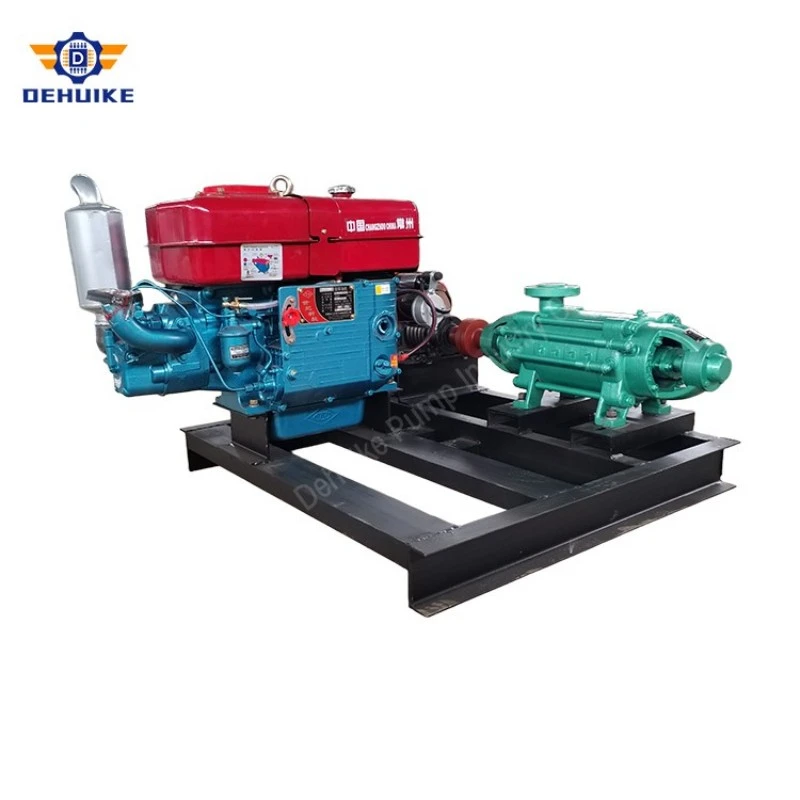
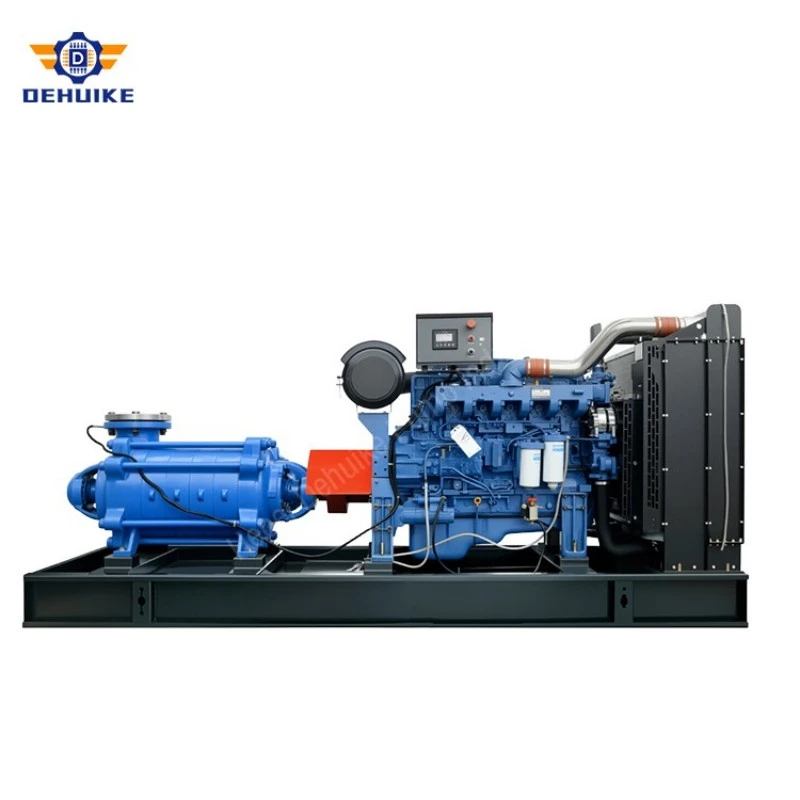
Flexible Powertrain Skid Packaging: Beyond stationary bare-shaft pumps, we engineer fully autonomous, skid-mounted or trailer-towable pump packages equipped with high-efficiency electric motors (IP55/IP66, Class F/H insulation) or diesel engines with automated start controllers for standalone emergency water transfer.
Worldwide Procurement Support
Dehuike delivers end-to-end commercial transparency, hydraulic engineering support, and dependable global logistics to streamline equipment procurement for international EPC contractors, municipal authorities, and industrial distributors:
Pre-Purchase Pipeline Hydraulic Analysis & CAD Layouts: Our applications engineering department provides complimentary technical evaluations for prospective installations. By reviewing static suction heights, pipeline friction curves, elevation profiles, and required delivery pressures, our engineers verify net positive suction head available margins (NPSHa), recommend optimal pump models, and provide customized 2D/3D CAD dimensional models within 2 hours of inquiry.
Custom Flange Standards & Voltage Windings: We accommodate international jobsite standards, machining connection flanges to ANSI/ASME B16.5 Class 150/300, European EN 1092-1 PN16/25/40, or Japanese JIS standards. Electric drive motors can be wound for international voltages and frequencies (such as 380V, 415V, 440V, 460V, or 575V at 50Hz or 60Hz, medium-voltage 6kV/10kV).
Standardized International Multimodal Logistics: We manage international shipments strictly via maritime container shipping (>500 kg heavy pump skids) and dedicated air transport (50–500 kg for urgent maintenance spares). Commercial contracts are quoted under transparent international trade terms, offering FOB and CIF destination port agreements without hidden port handling fees. All units are secured inside heavy-duty, seaworthy non-fumigation plywood crates with internal vapor-corrosion-inhibitor wrapping.
Hot Tags: multistage water supply pump, China multistage water supply pump manufacturers, suppliers, factory