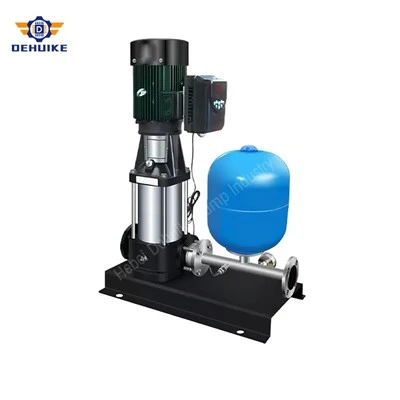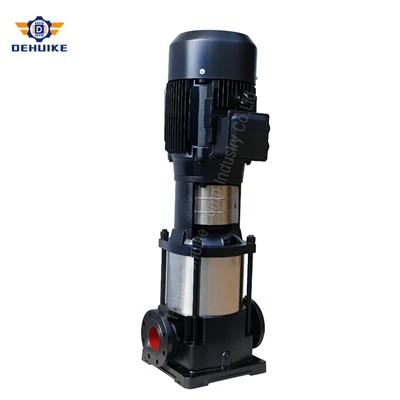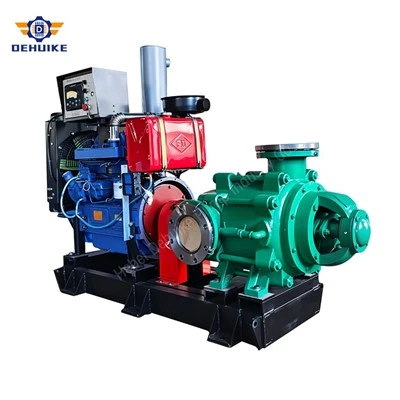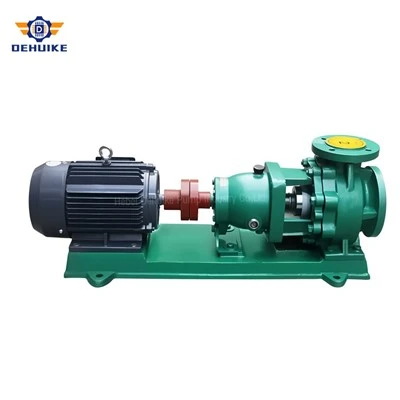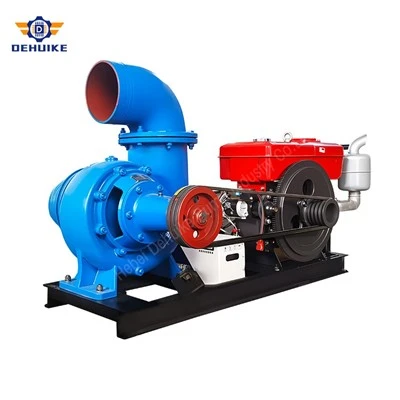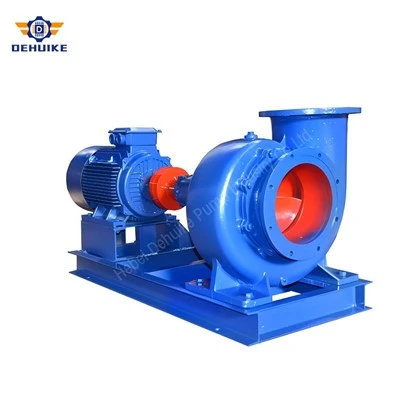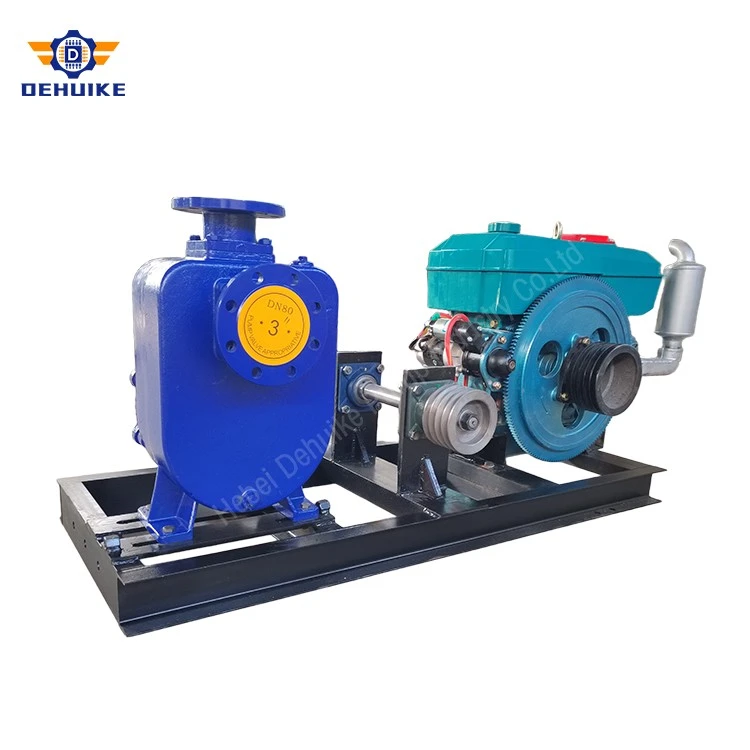
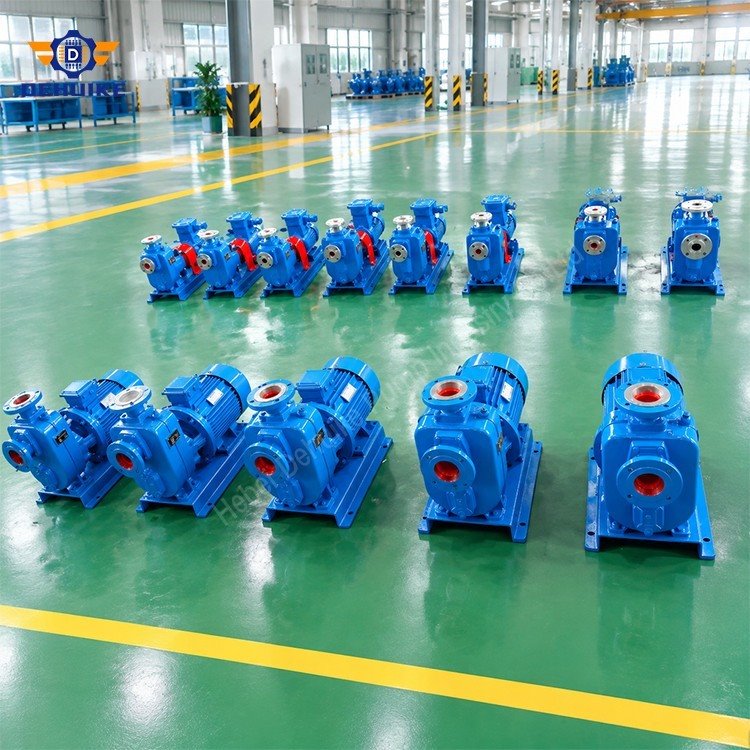
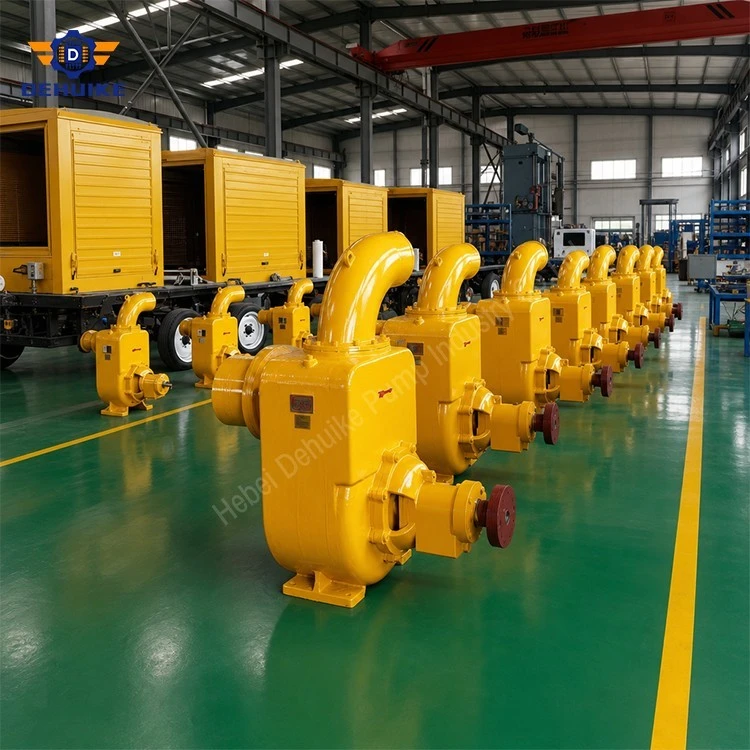
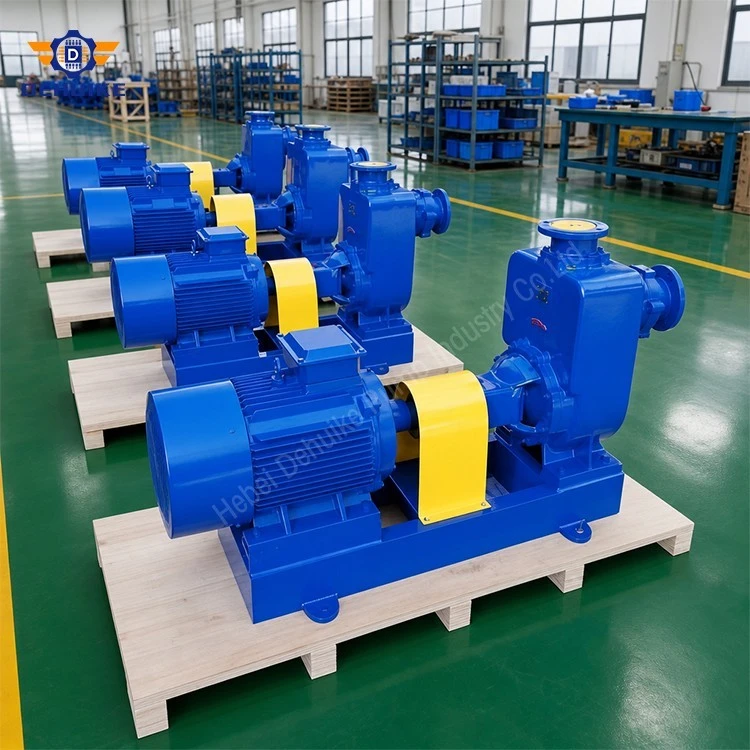
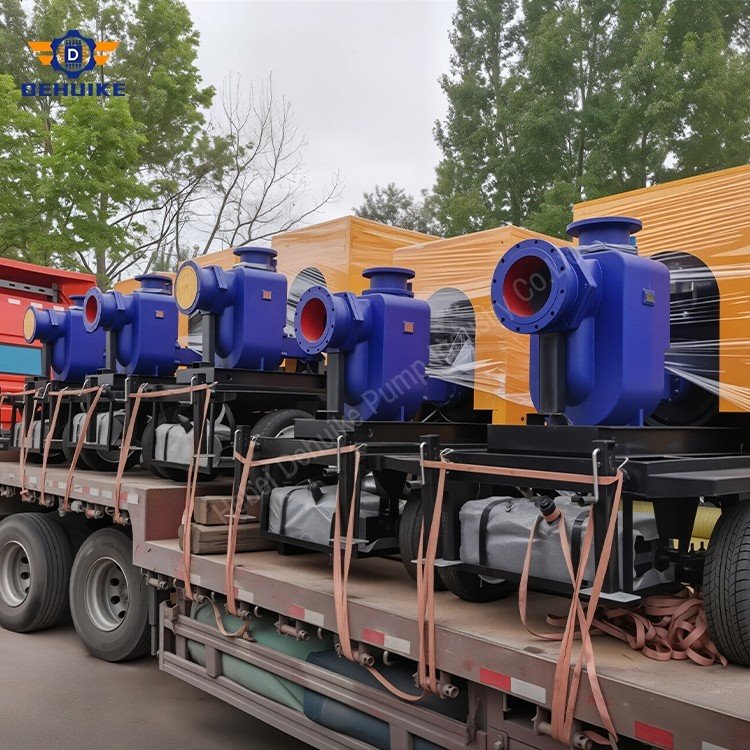
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of industrial self-priming water pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk industrial self-priming water pump for sale here from our factory. Also, pricelist is available.
Thermodynamic Vacuum Dynamics
Continuous industrial operations-such as thermal power co-generation, metallurgical smelting, chemical processing, and municipal water supply-require uncompromised reliability in fluid intake systems. In many industrial installations, water sources are positioned below the pump center line, situated within subsurface holding sumps, raw river channels, retention reservoirs, or deep cooling tower basins. Conventional end-suction centrifugal equipment cannot draw liquid under these conditions without complex priming devices: any atmospheric gas pocket trapped in the suction pipe creates an immediate air-lock that collapses fluid momentum and leads to destructive dry-running seal failure.
The heavy-duty Industrial Self-Priming Water Pump resolves this fundamental limitation through an automated two-phase gas-liquid separation casing. Rather than relying on gravity flooded inlets or submersible borehole installations, this surface-mounted centrifugal unit utilizes a two-stage air-water separation volute paired with an overhead expansion degassing vault. During initial start-up, pre-loaded liquid within the casing mixes with incoming pipeline air, shearing into an emulsified froth that separates rapidly in the expansion chamber. Degassed air vents harmlessly out the discharge riser while deaerated fluid recirculates to the impeller eye, pulling a powerful static vacuum reaching 6.5 meters and drawing a continuous water column up from deep reservoirs in under two minutes.
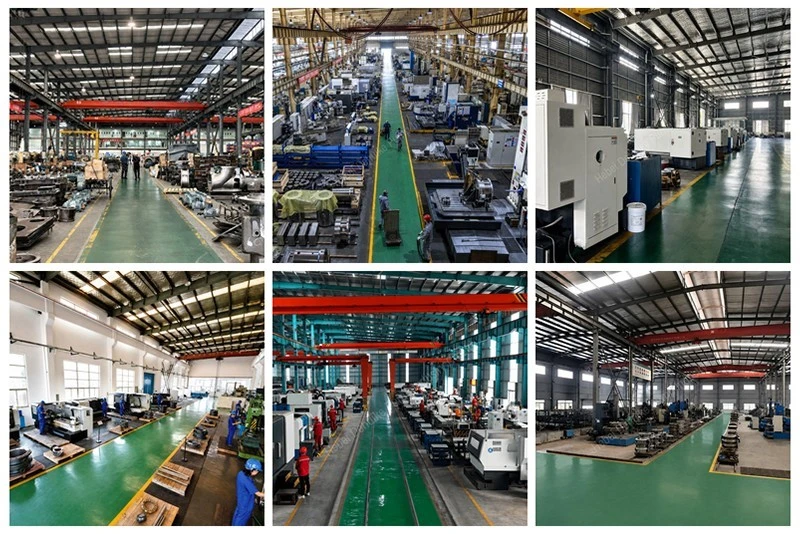
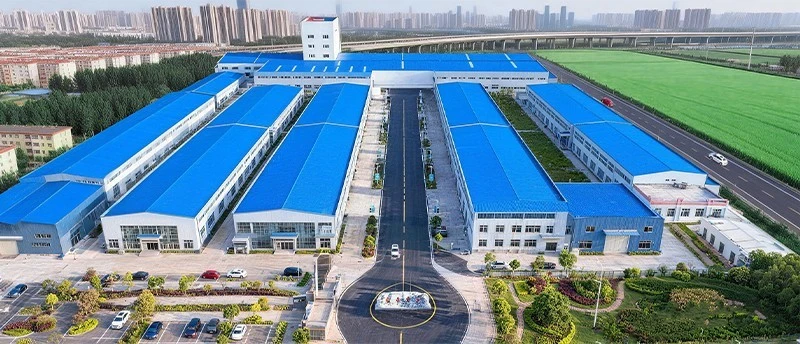
Engineered and fabricated by Hebei Dehuike Pump Industry Co., Ltd. (operating internationally under the DHK Pump mark), our ZX series clear water and ZW industrial effluent pumps draw upon over 30 years of specialized metallurgical casting and fluid machinery manufacturing. Operating from an integrated modern campus exceeding 8,000 m² and supported by an audited cooperative network comprising 900+ vetted supply partners, Dehuike delivers high-reliability self-priming pumping skids to industrial processing facilities, mining complexes, and municipal infrastructure projects across 50+ countries worldwide.
Mechanical Construction
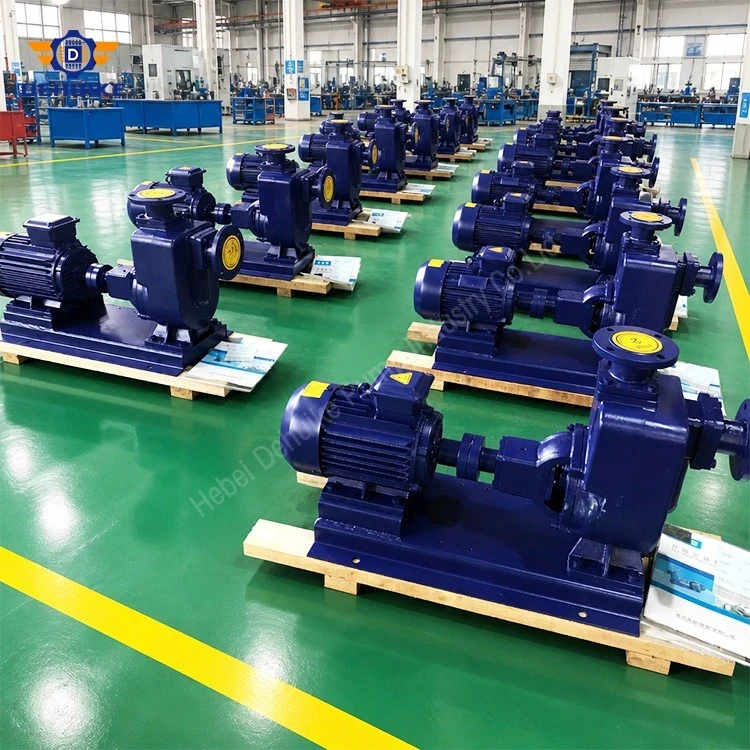
A forensic structural breakdown of the Industrial Self-Priming Water Pump illustrates why its surface-installed mechanical configuration provides decisive advantages in operational availability, operator safety, and maintenance accessibility. Key structural subsystems are engineered for continuous 24/7 service:
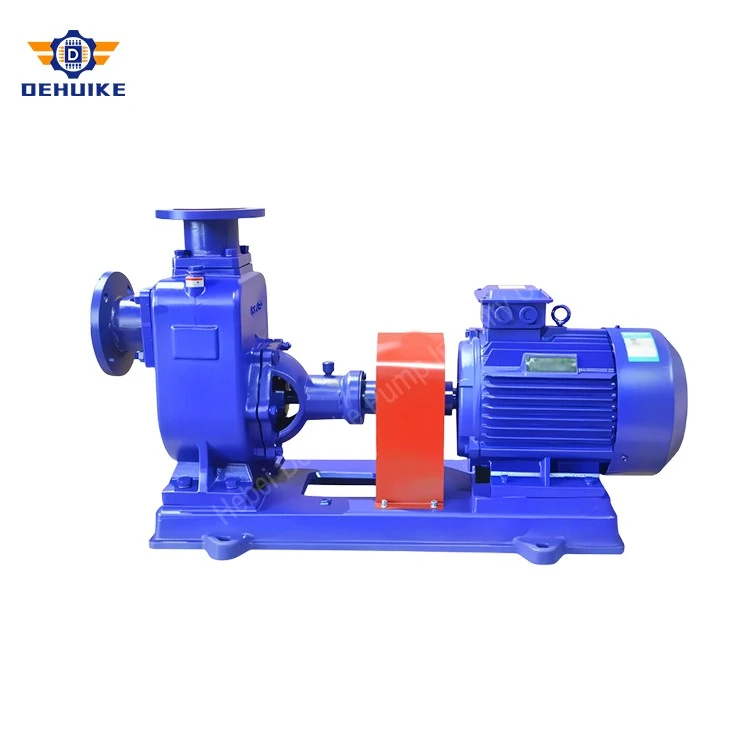
Dual-Chamber Volute & Vaulted Degassing Expansion Dome: The heavy cast-iron or stainless steel pump body is cast with a lower fluid storage basin and an enlarged upper deaeration chamber. This generous internal volume serves as an integrated reservoir that retains priming fluid after shutdown. The internal flow geometry slows discharge fluid velocity, allowing buoyant air bubbles to coalesce and vent into the delivery piping while returning clean fluid through bottom recirculation channels.
Precision-Balanced Closed Impeller with Optimized Shrouds: The hydraulic core incorporates an investment-cast enclosed multi-vane impeller. Precision-contoured backwards-curved vanes and smooth shroud surfaces minimize boundary layer friction and hydraulic slip, delivering dynamic heads up to 80 meters while generating exceptional fluid velocity to accelerate air evacuation during initial priming.
Integral Intake Check Valve (Eliminating Submerged Foot Valves): A durable synthetic elastomer flapper check valve is built directly into the horizontal suction nozzle of the pump. When the drive motor stops, gravity and casing backpressure seal the flap firmly against its seat, locking the full priming charge inside the volute. This eliminates down-hole foot valves at the bottom of the suction hose, preventing valve clogging from silt or weeds and guaranteeing immediate re-priming on automated restarts.
Oil-Quenched Cartridge Mechanical Shaft Seal: Because vacuum air evacuation creates temporary dry-running conditions across the shaft packing before water reaches the impeller, standard mechanical seals overheat rapidly. Our pumps integrate a balanced cartridge mechanical seal utilizing sintered hard-alloy mechanical seal rings submerged in an external oil lubrication bath. This oil bath dissipates frictional heat during deep air draw, ensuring hermetic sealing against vacuum leaks.
Rigid 40Cr Alloy Rotor Shaft & Heavy-Duty Bearing Carrier: The dynamic drive shaft is anchored by double-row angular-contact and cylindrical roller bearing assemblies inside a heavy cast pedestal isolated from the liquid casing. High-strength 40Cr structural alloy steel is normalized, tempered, and precision-ground to support heavy hydraulic thrust loads. The rigid shaft design restricts dynamic deflection beneath 0.035 mm at the stuffing box boundary, extending mechanical seal and bearing longevity.
Modular Back-Pull-Out Execution for Ground-Level Service: Designed for rapid field maintenance, the back-pull-out construction allows maintenance crews to withdraw the casing cover, dynamic seal cartridge, and pump impeller toward the motor without unbolting the suction or discharge pipe spools or disturbing the concrete foundation. Maintenance turnaround is reduced to under two hours in a clean, above-ground workspace.
Technical Parameters
Matching an Industrial Self-Priming Water Pump to plant requirements requires evaluating operating static lift heights, required delivery flow, piping friction head, and fluid temperatures. Dehuike Machinery manufactures standard self-priming units compliant with international centrifugal pump standards, providing plant engineers with versatile hydraulic selections.
The primary engineering parameter table below outlines certified operational performance ratings for representative ZX series clear water and process boosting models running at 1450 and 2900 RPM:
When conveying factory floor runoff, wastewater carryover, or light slurry mixtures, the ZW series provides wide-clearance hydraulic waterways. The table below outlines performance data across representative ZW solids-handling models:
Calculating Net Positive Suction Head Available (NPSHa)-by accounting for local atmospheric barometric pressure, vapor pressure at pumping temperature, vertical elevation lift, and line friction drag-ensures an operational buffer exceeding catalog NPSHr by at least 1.0 meter.
Testing Protocols
Because industrial utility water systems must operate without unexpected shutdowns or environmental leaks, Dehuike enforces rigorous non-destructive quality testing under accredited ISO 9001 governance, supported by international EAC and RoHS certifications:
Hydrostatic Proof Pressure Containment Testing: Every cast volute and casing cover undergoes hydrostatic pressure testing at 150% of rated working pressure (minimum 1.6 MPa to 2.4 MPa) for a continuous 30-minute hold period, verifying complete casting density and zero flange seepage.
Closed-Loop Hydraulic Performance Testing (ISO 9906 Grade 2B): Every completed pump operates on our computerized closed-loop hydraulic test station. Calibrated electromagnetic flowmeters and digital pressure transmitters log total head, flow capacity, shaft power, and efficiency across multiple throttling points to ensure full compliance with catalog curves.
Manufacturing Pedigree
Procuring industrial pumping machinery for plant construction or regional distribution demands selecting an established manufacturing partner with deep metallurgical mastery, precision machining capacity, and responsive commercial support. DHK Pump provides decisive competitive advantages for engineering contractors and plant owners:
Over Three Decades of Fluid Machinery Excellence: Supported by more than three decades of hydraulic casting mastery, our engineering works optimizes impeller geometries through numerical finite-element fluid analysis (FEA and CFD). Our designs optimize air evacuation speed without sacrificing hydraulic energy efficiency.
8,000+ m² Modern Integrated Heavy Manufacturing Facility: Our specialized industrial complex houses resin sand molding lines, medium-frequency electric melting furnaces, multi-axis horizontal boring machines, dynamic balancing stations, and automated test bays under one roof, providing complete quality traceability across every production step.
Audited Supply Chain Network (900+ Certified Partners): Leveraging an established cooperative network of 900+ verified domestic component providers across China, we maintain robust stocks of premium electric motors, heavy-duty mechanical seals, trailer axles, and certified alloy ingots, ensuring reliable production schedules and expedited deliveries.
Comprehensive 24-Month Factory Warranty Commitment: Every complete Industrial Self-Priming Water Pump manufactured by our works carries an official 24-month (two-year) comprehensive factory warranty covering the casing, rotor assembly, bearing bracket, and baseplate against defects in materials and craftsmanship.
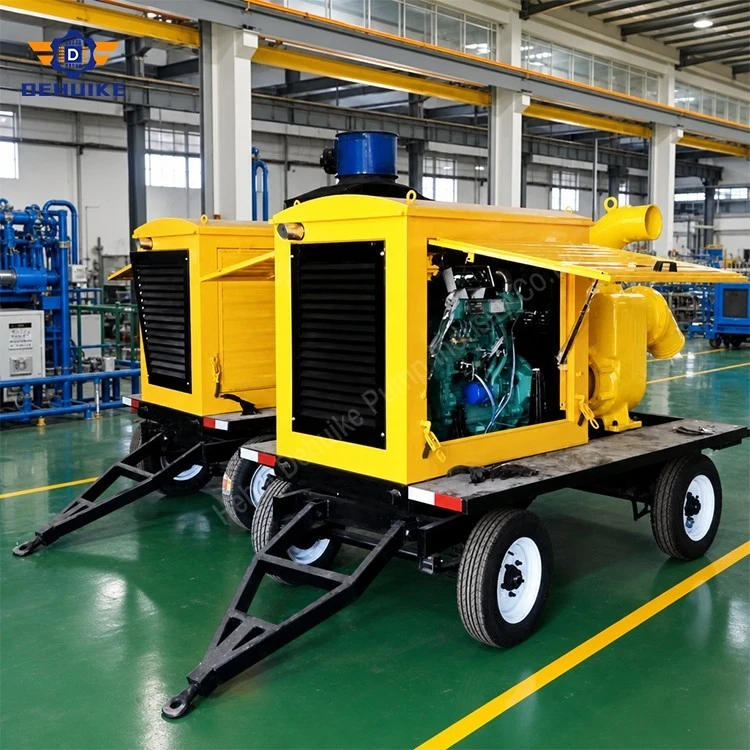
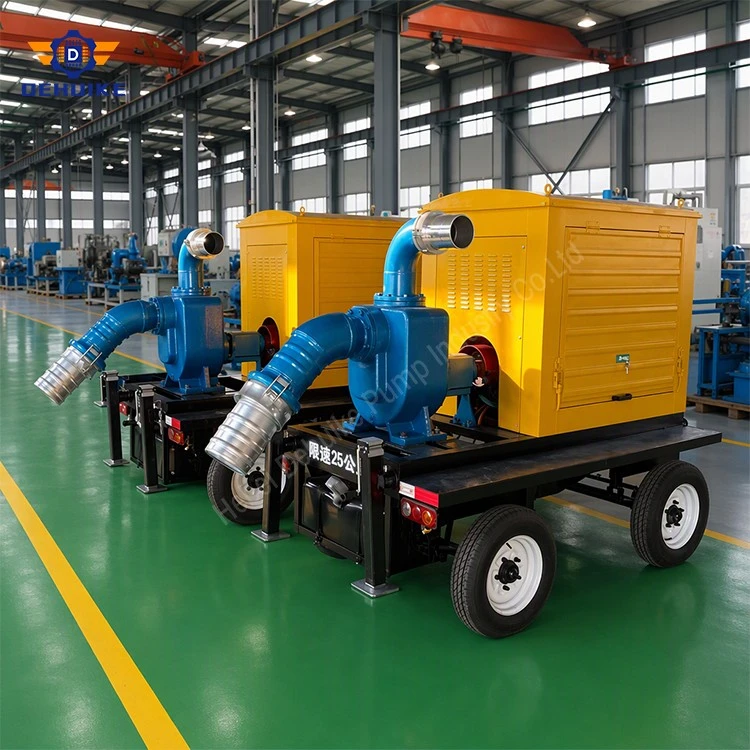
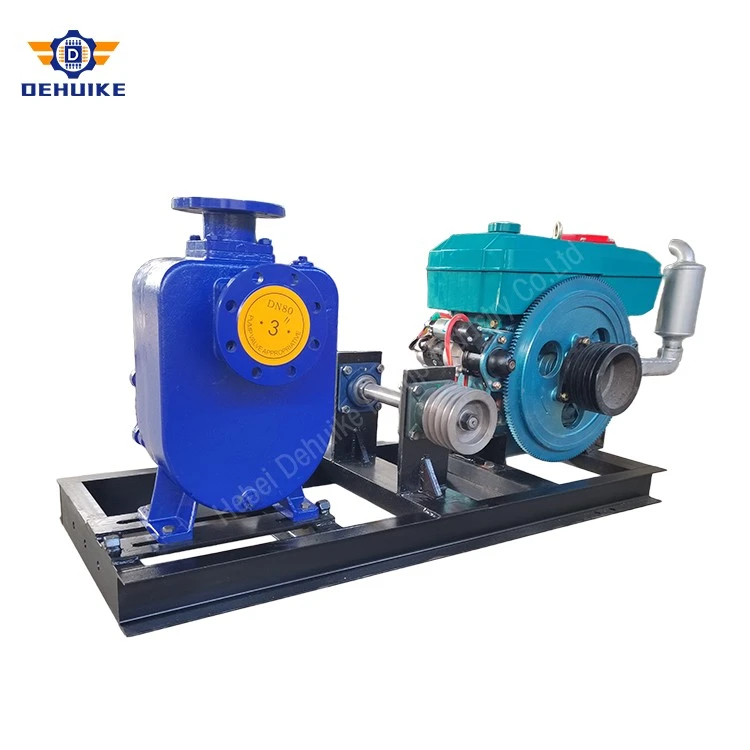
Flexible Powertrain Skid Packaging: Beyond stationary bare-shaft pumps, we engineer fully autonomous, skid-mounted or trailer-towable pump packages equipped with electric power drives (IP55 through IP66 weatherproof enclosures, Class F insulation with Class B temperature limits) or diesel engines with automated start controllers for standalone emergency service.
Worldwide Procurement Support
Dehuike provides complete commercial clarity, hydraulic engineering support, and dependable global logistics to streamline equipment procurement for international EPC contractors, municipal authorities, and industrial distributors:
Pre-Purchase Sump Hydraulic Analysis & CAD Layouts: Our applications engineering department provides complimentary technical evaluations for prospective installations. By reviewing static suction heights, pipeline runs, fluid densities, and operating temperatures, our engineers verify net positive suction head available margins (NPSHa), recommend optimal pump models, and provide customized 2D/3D CAD dimensional models within 2 hours of inquiry.
Custom Flange Standards & Voltage Windings: We accommodate international jobsite standards, machining connection flanges to ANSI/ASME B16.5 Class 150/300, European EN 1092-1 PN16/25, or Japanese JIS standards. Electric drive motors can be wound for international voltages and frequencies (such as 380V, 415V, 440V, 460V, or 575V at 50Hz or 60Hz).
Standardized International Multimodal Logistics: We manage international shipments strictly via maritime container shipping (>500 kg heavy pump skids) and dedicated air transport (50–500 kg for urgent maintenance spares). Commercial contracts are quoted under transparent international trade terms, offering FOB and CIF destination port agreements without hidden port handling fees. All units are secured inside heavy-duty, seaworthy non-fumigation plywood crates with internal vapor-corrosion-inhibitor wrapping.
Global Deployment Footprint
Leveraging over 30 years of specialized manufacturing experience in heavy industrial pumping equipment, Hebei Dehuike Pump Industry Co., Ltd. has established a formidable global footprint. Our heavy Industrial Self-Priming Water Pump packages operate reliably across critical infrastructure and process sectors across 50+ international export destinations:
Power Generation & Industrial Cooling Circuits (Southeast Asia): Installed across thermal power stations and petrochemical plants in Indonesia, Malaysia, and the Philippines, providing reliable water circulation for heat exchangers, cooling towers, and boiler auxiliary feeds.
Municipal Raw Water Intake & Utility Waterworks (Middle East): Operating on riverbank intakes, canal sumps, and raw water reservoirs in Saudi Arabia and the UAE, feeding municipal clarification reservoirs and potable water treatment filters without costly submerged wet wells.
Open-Pit Mining Dewatering & Mineral Concentrators (South America): Deployed on open-pit copper mine benches and quarry drainage trenches in Chile and Peru to evacuate abrasive pit runoff and gravel washdown into primary settling basins.
Chemical Processing & Industrial Washdown Facilities (Europe): Serving chemical manufacturing plants, pulp mills, and industrial surface finishing facilities across Germany and Poland, handling industrial washdown lines and fluid temperatures reaching 110°C.
Hot Tags: industrial self-priming water pump, China industrial self-priming water pump manufacturers, suppliers, factory