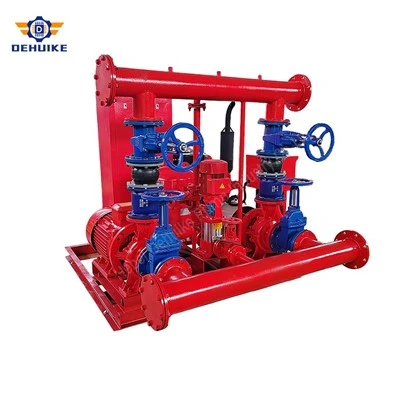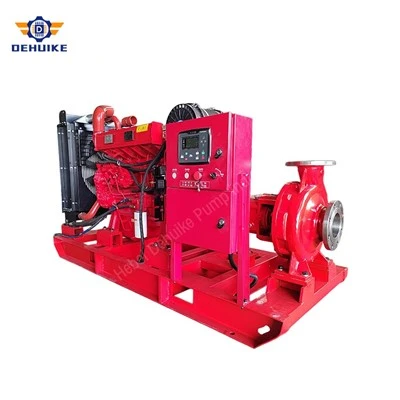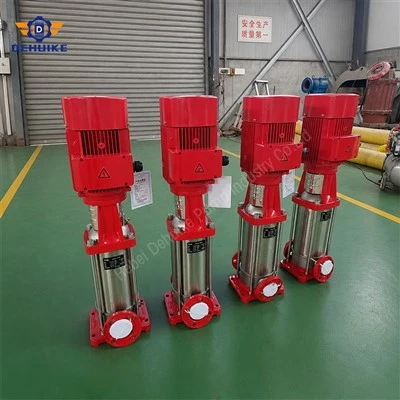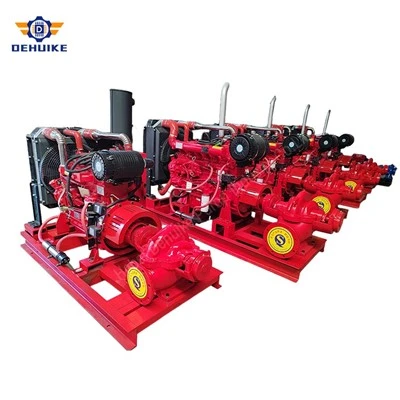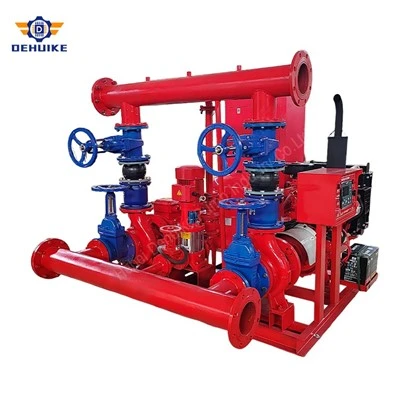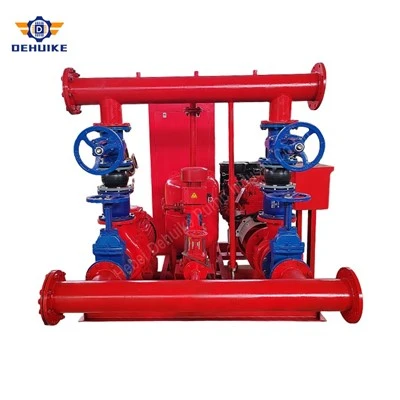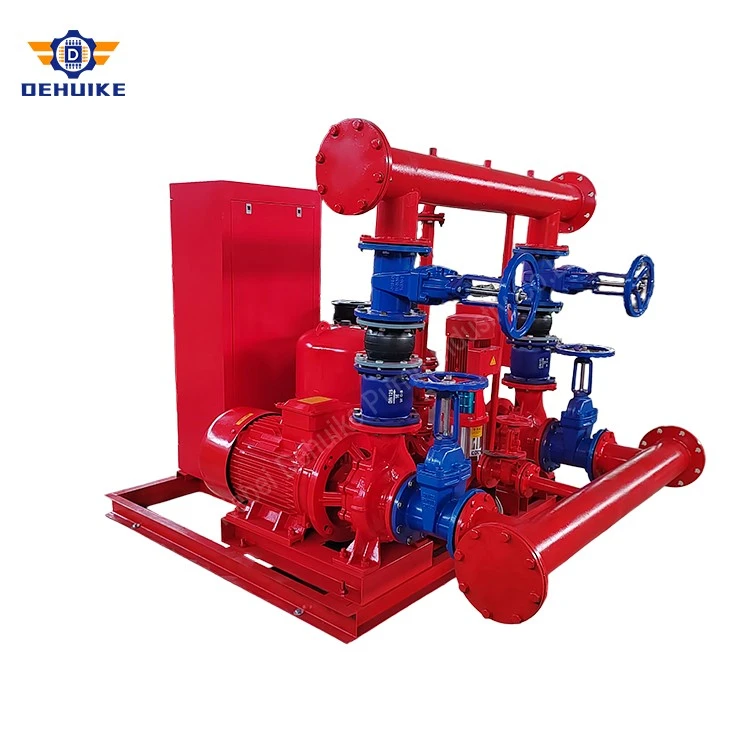
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of electric and diesel fire pump set in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk electric and diesel fire pump set for sale here from our factory. Also, pricelist is available.
Product Overview: Dual-Driver Water Supply Skid for Grid-Tied Duty and Blackout Emergency Standby
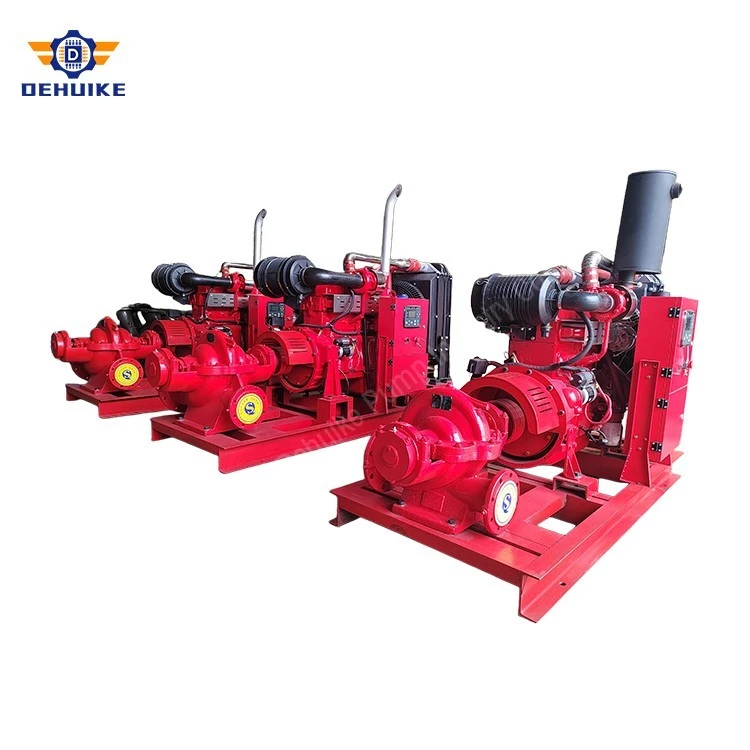
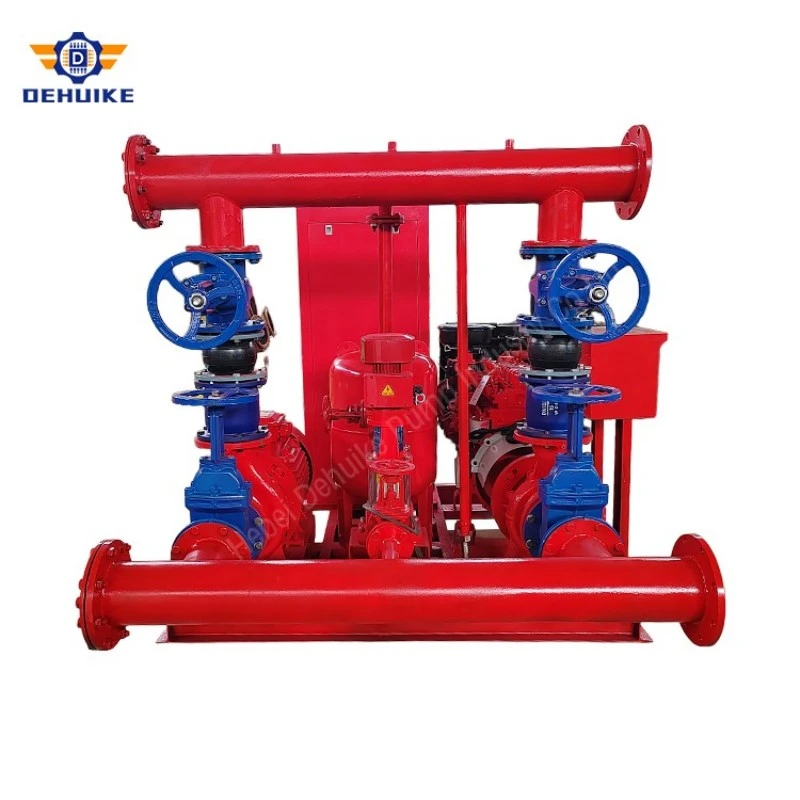
When a structural fire threatens an industrial complex, commercial tower, or municipal hub, water supply integrity cannot depend on a single utility feed. Grid power often drops out or is isolated during structural fires, leaving standard motor-driven pumps useless when sprinkler heads and standpipes demand full pressure. A dual-driver fire station resolves this vulnerability by coupling an efficient electric centrifugal pump with an autonomous compression-ignition diesel engine unit. Sharing a common manifold under automated cabinet coordination, the station delivers rated volume and head whether facility substations are live or completely blacked out.
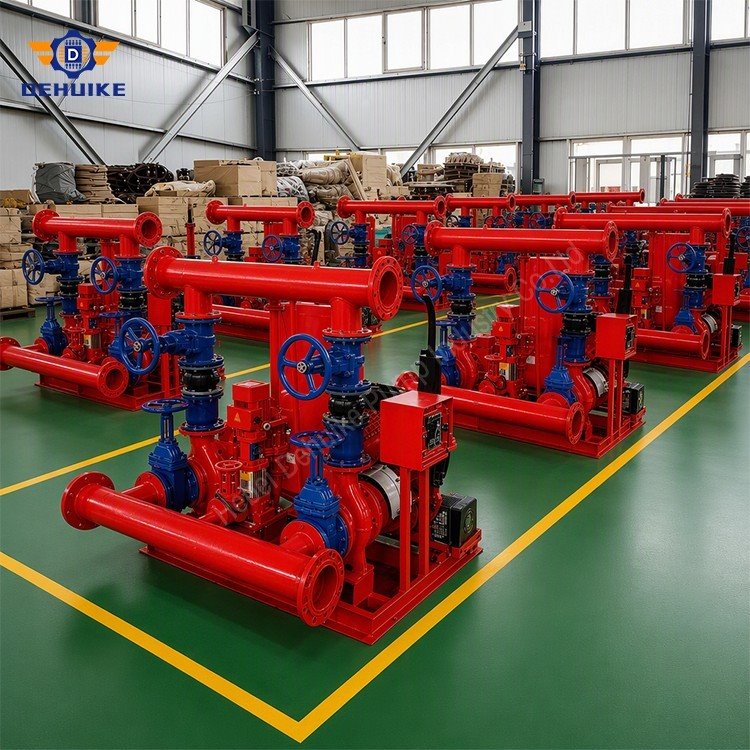
Engineered for international mechanical contractors, MEP consultants, and facility directors, this dual-power fire suppression package pairs reliable fluid machinery with heavy-duty engine mechanics. Rather than forcing a rigid layout, the package accommodates multiple casing styles: vertical in-line single-stage units for tight pump rooms, horizontal end-suction models for spacious utility floors, and vertical multistage barrel pumps for tall riser circuits. Paired with industrial diesel prime movers, pressure-maintaining jockey skids, and automated sequencing switchboards, each layout is custom configured to match calculated line losses, required nozzle pressures, room dimensions, and local codes.
For procurement officers and mechanical estimators, the justification for selecting a unified electric-diesel station extends well beyond acquiring two separate machines. Its genuine value lies in synchronized emergency response. During non-fire hours, an auxiliary jockey unit absorbs minor line weeping across distribution piping. When a sprinkler ruptures or a hose valve opens, the primary electric driver engages within seconds. Should the electrical grid fail, the diesel unit executes an automated cranking cycle, restoring rated fire flow without manual intervention. This coordinated failover architecture guarantees dependable life-safety compliance.
Engineering Specifications and Station Architecture Matrix
To accommodate varied structural footprints, available site power, and hydraulic duty requirements, the dual-driver station incorporates distinct casing architectures and driver pairings. The engineering matrix below outlines primary system functions, pump classifications, certified operating envelopes, and practical installation benefits for engineering review:
Selecting the ideal station requires aligning pump capabilities with calculated design flow, NPSHa margins, static elevation, piping friction, supply voltage, spatial clearances, and fuel placement. Our application engineers review these site factors to supply a harmonized package built for your exact project envelope.
Dual-Prime-Mover Coordination and Blackout Failover Mechanics
A resilient fire pump room addresses two fundamental requirements: steady baseline pressurization and high-output crisis survivability. Under standard standby, distribution piping remains charged with static water pressure, ensuring immediate discharge upon sprinkler glass bulb rupture. Once continuous flow initiates, the electric motor starts instantly, drawing primary power from building switchgear. However, structural fires often sever electrical lines or trigger transformer isolations. The diesel skid provides vital mechanical independence, maintaining required hydrant stream volumes and nozzle pressures even during a complete electrical blackout.
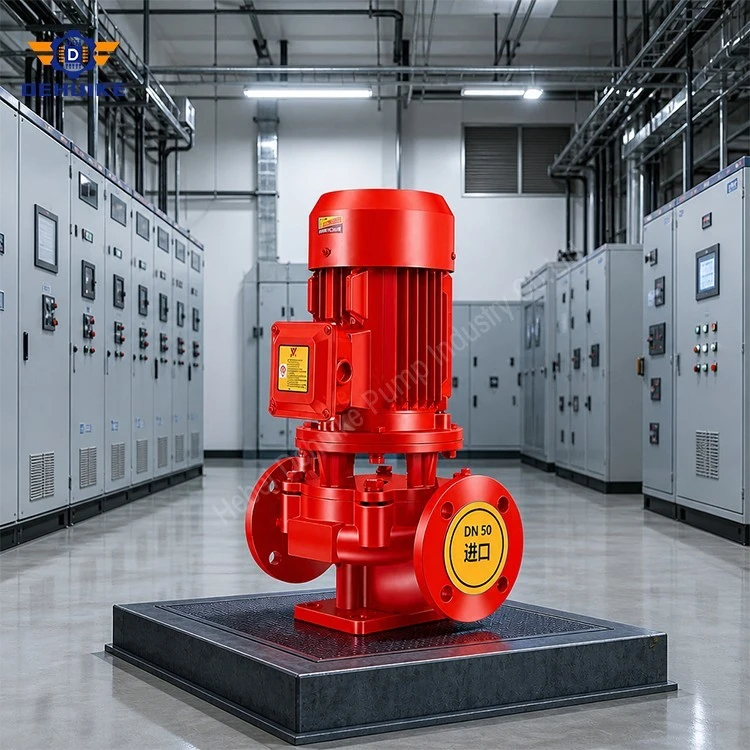
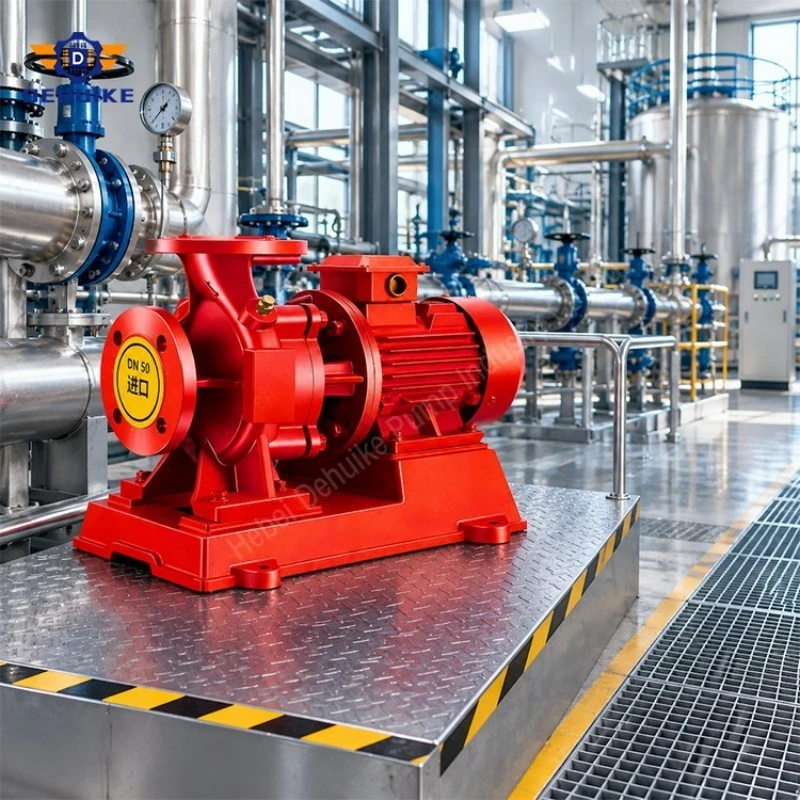
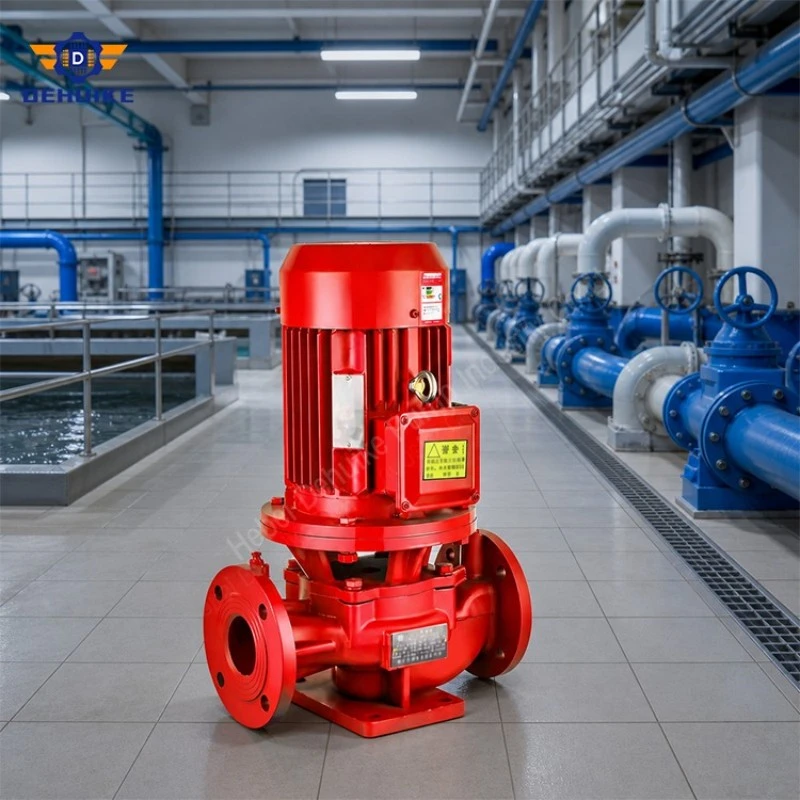
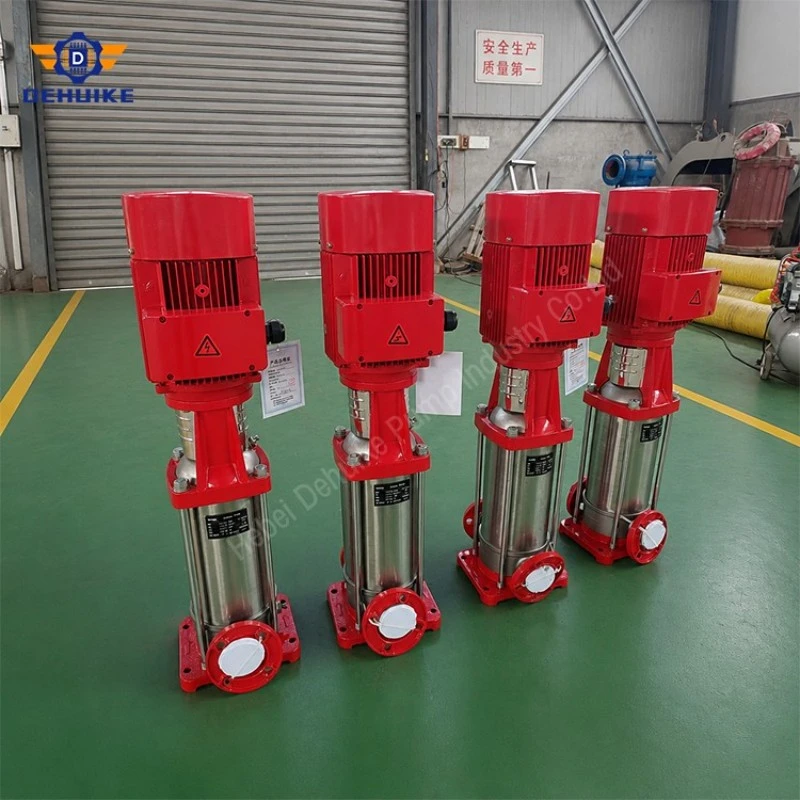
Casing architecture selection on the motor-driven branch directly influences plant room ergonomics and piping layout. Vertical in-line XBD-L units minimize required floor footprint by integrating suction and discharge flanges on a single horizontal axis. For spacious mechanical rooms with rigid inertia pads, horizontal XBD-W end-suction units provide direct access for bearing inspections and packing renewals. When multi-story buildings demand high static lift, vertical multistage XBD-GDL pumps generate steep head curves progressively through stacked impeller stages, matching calculated friction curves across multi-zone sprinkler risers.
On the secondary engine branch, successful operation depends on precise mechanical coupling and power margin sizing. Our engineering schedule pairs pump shaft demands (2.68kW to 48.3kW) with continuous diesel ratings from 5.67kW up to 60kW. Sizing the prime mover strictly to nominal hydraulic output creates operational hazards; engine selection must account for cooling radiator losses, high ambient engine-room temperatures, altitude de-rating, and fast acceleration torque. Our skids incorporate dual-cranking solenoids, jacket water heat exchangers, and heavy flywheels for rapid startup within fifteen seconds.
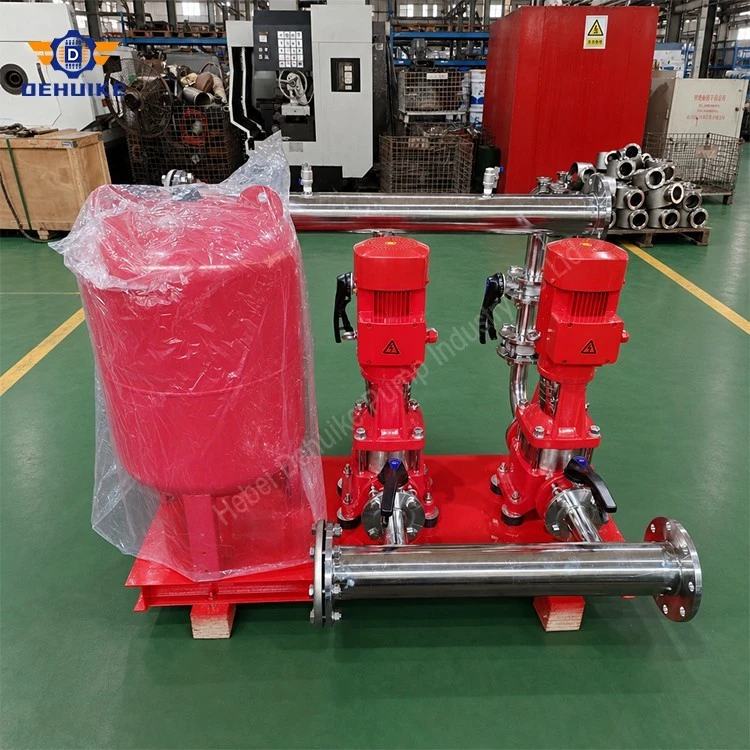
System automation and network pressure stabilization tie the dual drivers into a coherent life-safety asset. The vertical Z(W/L) jockey pump replenishes micro-losses from valve packing, preventing cyclic wear on main motors. The master control console monitors manifold transducers: if water pressure drops below the primary setpoint, the electric pump starts; if voltage drops or the motor fails, control logic triggers automated diesel cranking. All run signals, battery charges, and fault alarms are supervised continuously.
Field Deployment Environments: Commercial, Industrial, and Public Works
Dedicated life-safety water stations represent the foremost application for this dual-power equipment. Across underground pump vaults, centralized water supply reservoirs, and exterior hydrant loops, the package forms the hydraulic backbone of the facility, supplying wet-pipe risers, pre-action valves, and deluge systems in strict compliance with municipal fire regulations.
High-density commercial and residential developments rely heavily on this dual-driver concept. Office skyscrapers, shopping complexes, hotels, underground parking structures, and distribution centers present complex hydraulic gradients. Multistage electric units deliver sustained vertical lift to upper zones, while the diesel standby unit guarantees emergency water pressure if utility feeds are severed during a building evacuation.
Heavy industrial complexes impose severe operating hazards. Petrochemical refineries, chemical bulk storage terminals, mining pits, and thermal power plants handle flammable hydrocarbons and combustible dusts. In these hazardous environments, structural blazes can cause catastrophic explosions. Independent diesel pumping skids provide an uncompromised mechanical failsafe against plant-wide electrical blackouts.
Municipal infrastructure and transportation hubs demand dependable fire suppression networks. Subway stations, highway tunnels, aviation hangars, port terminals, and water treatment plants experience dense passenger movement and strategic importance. A certified electric-diesel package meets public safety guidelines while offering local maintenance crews accessible service points.
Our manufacturing expertise across more than thirty industrial pump categories-including slurry handling, chemical processing, and deep-well extraction-reinforces our fire package design. When developing large manufacturing facilities, general contractors often require utility water supply, effluent drainage, and fire protection simultaneously. Our broad fluid machinery background enables holistic site coordination, simplifying equipment procurement for overseas project managers.
Five-Stage Engineering Procedure: Hydraulic Sizing to Skid Delivery
Stage One: Establish the Hydraulic Duty Point. Sizing begins by calculating total water demand for the occupancy hazard class. Engineers combine the design sprinkler discharge with mandatory hose stream allowances. Total dynamic head (TDH) is determined by summing suction lift, elevation to the highest nozzle, piping friction losses, and required residual discharge pressure. Accurate TDH calculations prevent motor overload and ensure effective fire suppression.
Stage Two: Select the Electric Casing Architecture. Physical room dimensions guide pump casing selection. For space-constrained rooms, XBD-L vertical in-line pumps offer a compact footprint with simplified piping. When floor area allows and horizontal bearing servicing is preferred, XBD-W horizontal pumps represent a robust option. For multi-story projects requiring high pressures, XBD-GDL vertical multistage pumps provide efficient head development.
Stage Three: Match the Diesel Standby Unit and Derating Factors. The diesel engine must cover the full pump operating curve, including 150% of rated flow. Continuous engine horsepower must exceed maximum shaft power by 10% to 20%. Designers must also apply de-rating corrections for ambient temperature, site elevation, and radiator fan loads to guarantee reliable starting torque.
Stage Four: Audit Room Ventilation, Exhaust Backpressure, and Fuel Layout. Diesel prime movers require adequate combustion and cooling air through sized intake louvers and exhaust ducts. Exhaust piping must use flexible bellows, silencers, and sweeping bends to prevent excessive manifold backpressure. The fuel day tank must provide gravity head to the injection pump while maintaining safe clearance.
Stage Five: Verify Water Quality and Suction Conditions. Standard skids are built for clean water free of abrasive grit, operating within 80°C for XBD-W models. For surface river supplies or industrial holding ponds containing silt or salts, clients should supply water analysis reports. Our metallurgists can configure stainless steel impellers and hardened seals to resist erosion.
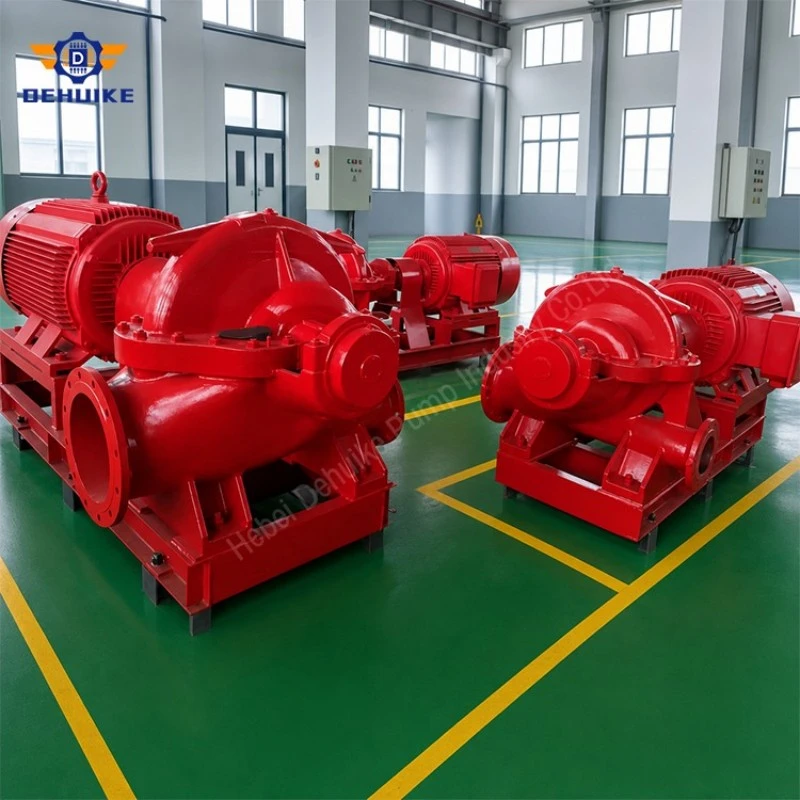
Manufacturing Capabilities and Industrial Heritage at Hebei Dehuike
Hebei Dehuike Pump Industry Co., Ltd. is an integrated fluid machinery enterprise combining research and development, hydraulic modeling, casting, machining, dynamic balancing, testing, and worldwide distribution. This end-to-end manufacturing control is essential for fire safety equipment, where casing strength, dynamic balance, engine governance, and automated switchgear must align seamlessly.
From raw metallurgical ingots to finished skids, our production enforces rigorous quality governance. Our plant houses modern foundries, CNC machining centers, dynamic balancing rigs, and a computerized hydraulic testing station. Every pump casing undergoes hydrostatic pressure verification, ensuring casting integrity and stable field operation.
With more than 30 years of specialized pump manufacturing experience, our engineering team utilizes CFD flow simulation and FEA modeling to refine equipment reliability. Our pumping packages operate across more than 50 countries throughout Southeast Asia, the Middle East, Central Asia, South America, and Europe. This export experience enables us to deliver compliant submittal packages and durable marine packaging.
Our production encompasses over thirty industrial pump series, including agricultural irrigation, heavy slurry, wastewater, clean water centrifugal, and submersible pumps. This extensive fluid handling capability allows us to support EPC contractors requiring multiple pumping systems across a single industrial development.
Quality Assurance Protocols, Factory Acceptance Testing, and Lifecycle Support
Quality control begins prior to mechanical assembly. Application engineers verify driver matching, shaft shear stress, and enclosure ratings. During fabrication, ultrasonic testing inspects high-stress casing sections, and CMM equipment verifies bearing tolerances. Each completed pump casing is held at 1.5 times maximum design working pressure during hydrostatic testing.
Prior to dispatch, every skid completes dynamic validation in our automated testing station. Technicians map the five-point performance curve: shut-off churn head, 50% flow, 100% rated duty point, 150% overload capacity, and the Rated Optimal Efficiency Point (BEP). Diesel units complete automated cold-cranking cycles, load acceptance checks, and vibration analysis.
Our facility operates under certified ISO 9001 quality management systems, alongside EAC and RoHS certifications. We back every fire pump set with a 2-year (24-month) factory warranty on non-wearing mechanical parts. Furthermore, our technical department provides pre-sale engineering reviews, CAD layout drawings, wiring diagrams, and remote commissioning guidance.
From an engineering procurement perspective, specifying an integrated dual-driver station streamlines project delivery. Rather than coordinating third-party engines and pumps on site, contractors receive a pre-aligned, factory-tested assembly. This single-source approach reduces procurement overhead and establishes clear warranty accountability.
Commercial Efficiency and Turnkey Delivery for Overseas Projects
For international engineering contractors, mechanical distributors, and industrial facility owners, our dual-power fire stations eliminate the risks of fragmented sourcing. By integrating electric pumps, diesel standby drivers, jockey units, and control consoles into a pre-tested package, project teams accelerate installation, reduce field changes, and ensure smooth authority approvals.
To ensure damage-free transit, every skid is preserved with rust inhibitors, wrapped in vapor-barrier film, and bolted inside heavy fumigated wooden crates. We offer flexible shipping arrangements, supporting ocean shipping (sea freight) for complete project lots and air freight for time-critical components, delivering dependable value to fire safety projects globally.
Frequently Asked Engineering Questions: Dual-Driver Fire Stations
Q1: How does an integrated electric-motor and engine-driven fire station operate during emergencies?
A dual-driver fire pumping station integrates two distinct prime movers on a single hydraulic manifold: an electric motor for standard grid-tied operation and an industrial diesel engine for autonomous emergency standby. If a power outage occurs while fire sprinklers or hydrants are discharging, the control console detects grid failure or low water pressure, instantly cranking the diesel engine to maintain uninterrupted fire suppression flow.
Q2: What primary centrifugal casing configurations are available for the motor-driven branch?
Depending on mechanical room clearances and pressure requirements, three primary casing designs can be selected: XBD-L vertical in-line single-stage pumps for space-constrained footprints; XBD-W horizontal end-suction pumps for plant rooms prioritizing horizontal bearing serviceability; and XBD-GDL vertical multistage pumps for high-rise buildings requiring substantial vertical lift.
Q3: What certified hydraulic output and horsepower ratings define the backup engine assemblies?
Standardized diesel packages provide hydraulic capacities of 10, 15, 20, or 25 L/s across pressure ratings from 0.20 to 1.62 MPa. Operating at rotational speeds of 1500, 2000, 2200, 2300, or 2400 rpm, these units absorb shaft power between 2.68 and 48.3 kW, paired with 4–55 kW electric starting motors and diesel prime movers rated from 5.67 up to 60 kW continuous output.
Q4: What technical risks justify pairing an auxiliary engine with a grid-connected motor?
Utility power lines frequently burn through, short circuit, or get deliberately isolated by municipal firefighters during severe building blazes. Coupling an autonomous diesel engine ensures that even if incoming electrical feeders are completely dead, the pumping station continues supplying water to life-safety networks through an isolated, mechanical source of motive power.
Q5: What essential site metrics and hydraulic variables should be submitted for equipment sizing?
To configure an exact equipment package, please provide: required design flow (L/s or m³/h), total dynamic head or discharge pressure (m or MPa), plant room spatial layout, site power parameters (voltage, frequency, phases), static suction water level (flooded or suction lift), ambient temperature and elevation, and local fire authority specifications.
Q6: Is this dual-driver arrangement suitable for multi-story towers and tall riser installations?
Yes. For multi-story commercial and residential towers, we specify high-head XBD-GDL vertical multistage pumps alongside heavy-duty XBD-W horizontal pumps. These units generate the high static pressure required to feed upper-floor sprinkler loops, matched with an engine-driven standby unit on the same manifold.
Q7: What raw water quality benchmarks and liquid characteristics must the suction supply satisfy?
The standard pump materials are engineered for clean water free from heavy sand, abrasive grit, or long stringy solids, with fluid temperatures up to 80°C for XBD-W horizontal units. For raw river intakes or brackish coastal reservoirs, please supply water quality data so our engineering team can provide stainless steel impellers or hardened mechanical seals.
Q8: How does the auxiliary jockey pressurization unit integrate into the main pipe network?
A vertical Z(W/L) series jockey package, featuring a small multistage pump, pressure switch manifold, and diaphragm surge tank, connects to the main header. It cycles on and off automatically to replenish normal line pressure drops caused by minor valve seepages, preventing unnecessary starts on the larger primary and emergency fire pumps.
Hot Tags: electric and diesel fire pump set, China electric and diesel fire pump set manufacturers, suppliers, factory