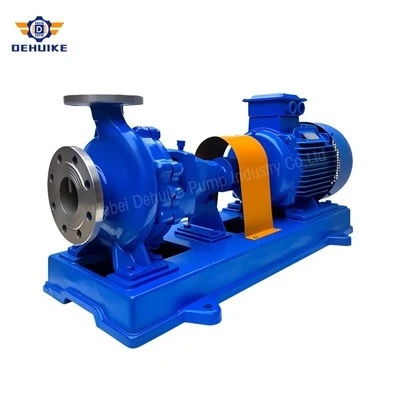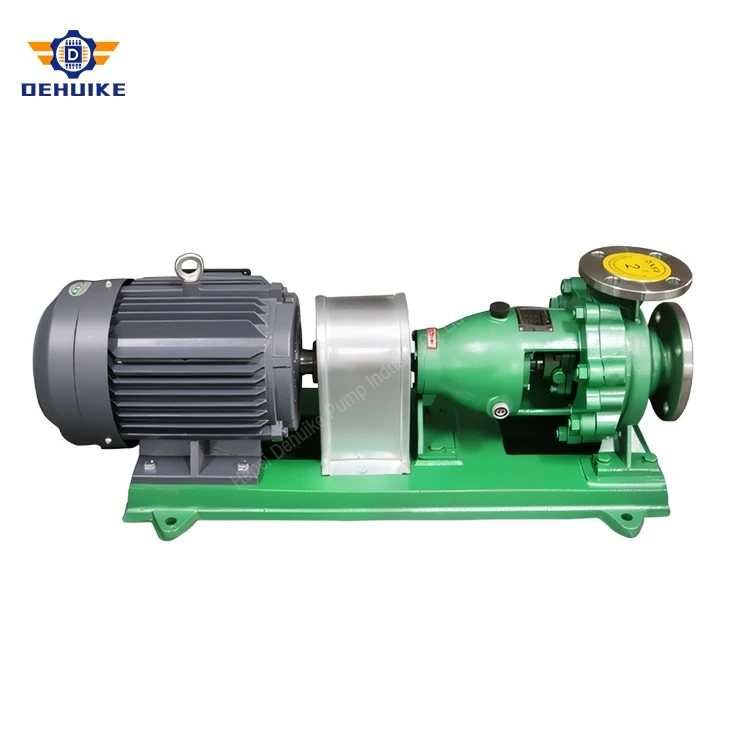
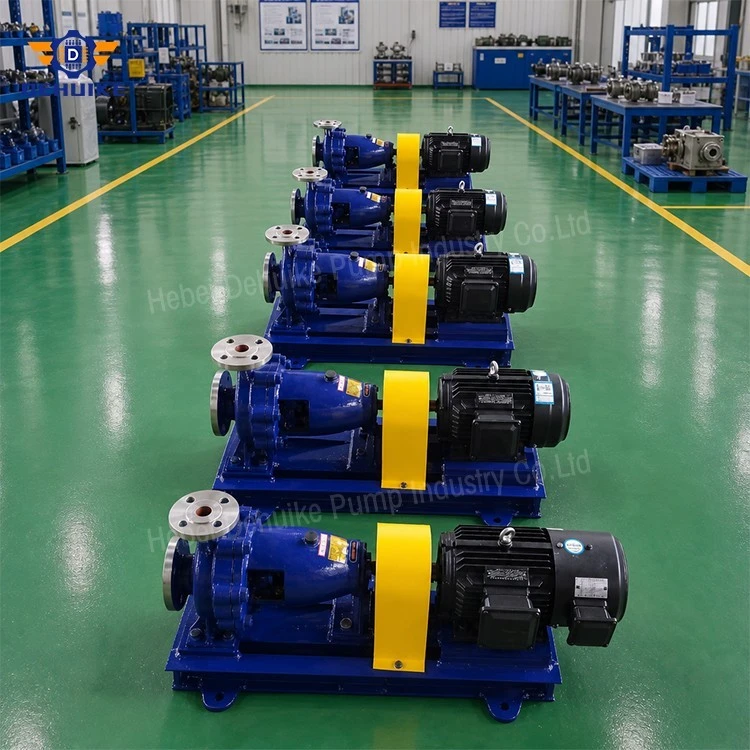
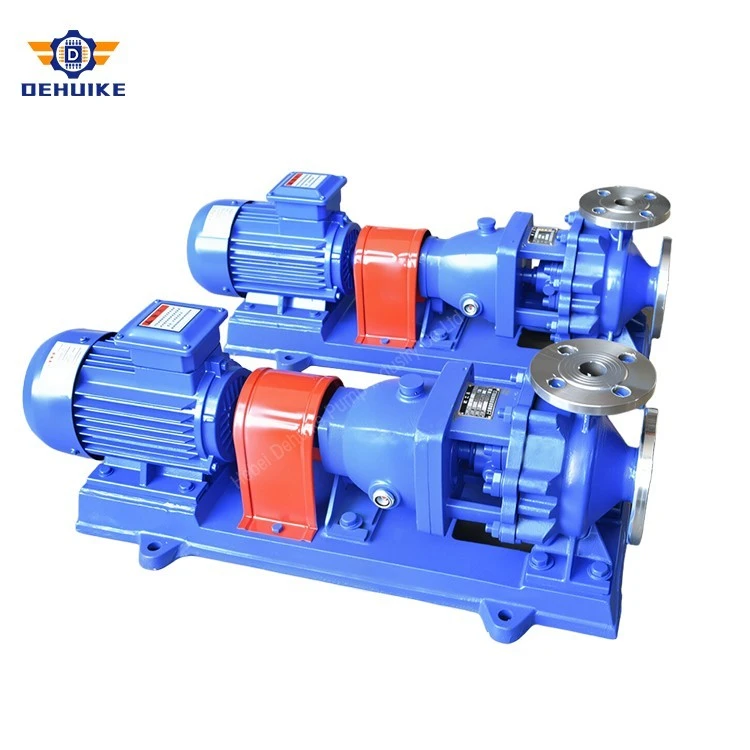
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of magnetic drive chemical pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk magnetic drive chemical pump for sale here from our factory. Also, pricelist is available.
Sealless Magnetics, Zero-Fugitive Emissions, and Hermetic Fluid Containment
In modern high-consequence process plants, conveying lethal, carcinogenic, pyrophoric, or highly volatile chemicals demands pumping hardware that eliminates mechanical shaft seal leakage entirely. Traditional packed glands and dynamic mechanical seals inevitably rely on liquid film lubrication across sliding faces, creating unavoidable microscopic vapor emissions and persistent seal face failure risks. When handling toxic substances such as phosgene derivatives, hydrocyanic solutions, benzene aromatics, or liquefied chlorine, even minute fugitive emissions present severe environmental non-compliance and life-safety hazards. The Magnetic Drive Chemical Pump provides an uncompromising sealless fluid architecture, replacing dynamic mechanical shaft penetrations with an impenetrable static containment barrier to deliver complete, hermetic fluid isolation.
Torque transmission in the Magnetic Drive Chemical Pump occurs via contactless magnetic synchronous coupling. An outer magnetic rotor driven by an electric motor rotates outside a static non-magnetic containment shell, while an inner magnetic rotor resides hermetically sealed inside the pump casing, connected directly to the hydraulic impeller shaft. High-energy permanent magnets-specifically grade Sm₂Co₁₇ samarium-cobalt with Curie points exceeding 350°C-generate powerful flux lines that penetrate the non-magnetic barrier wall without physical contact. The inner rotor tracks driver rotation synchronously, converting electrical motor torque into hydrodynamic fluid velocity while keeping aggressive process chemicals completely isolated from the atmosphere.
A decisive engineering advantage of this sealless architecture is the total eradication of dynamic shaft wear and external seal support systems. Mechanical seal systems handling toxic or volatile liquids typically demand complex API 682 Plan 53 barrier reservoirs, nitrogen pressurization racks, and continuous barrier liquid replenishing lines. The Magnetic Drive Chemical Pump eliminates these costly auxiliary circuits, utilizing internal product recirculation to lubricate silicon carbide sleeve bearings while continuously carrying away magnetic eddy-current thermal energy, drastically simplifying plant piping arrangements and lowering total cost of ownership.
Designed in full compliance with ISO 2858 envelope boundaries and ISO 5199 engineering standards, the pump integrates a modular back-pull-out structural layout. Maintenance personnel can dismantle and service internal rotating magnetic cartridges, thrust collars, and stationary bushings without breaking suction and discharge piping manifolds or disturbing motor foundation shims. This accessible design minimizes plant overhaul downtime, enhances maintenance personnel safety, and guarantees reliable compliance with regional Clean Air Act fugitive emission mandates.
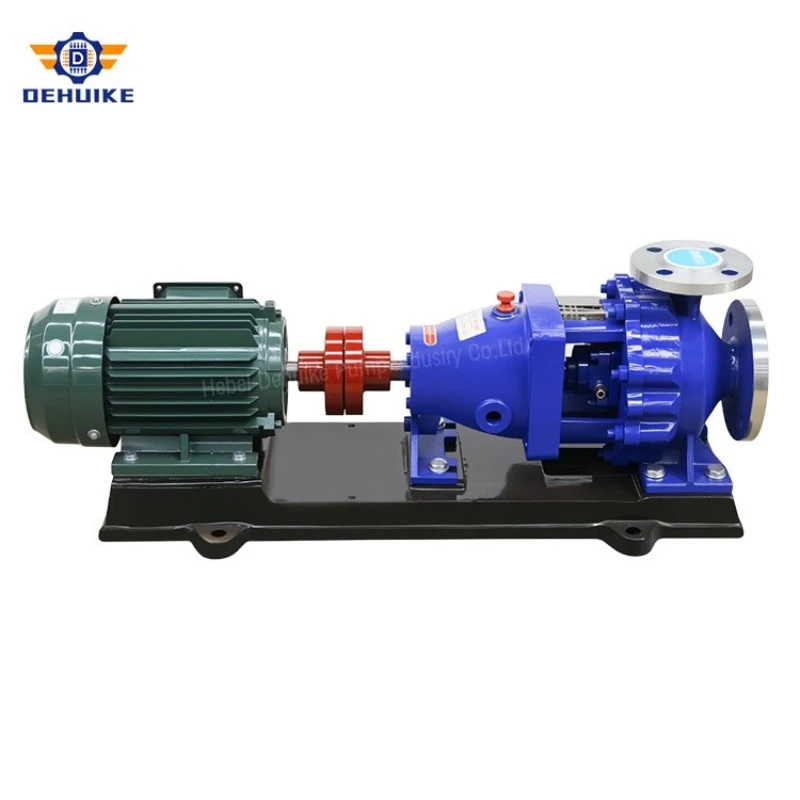
Technical Specifications & Tri-Series Parametric Envelopes
Pumping hazardous and volatile chemicals requires precise hydraulic sizing to prevent vapor formation across the internal magnetic containment cavity. To ensure optimum system integration while safeguarding magnetic synchronous coupling torque, the Magnetic Drive Chemical Pump is configured into three engineered operating series. Every data point corresponds to certified hydraulic dynamometer test records, presented by rotational frequency and calibrated impeller trimming profiles without combining operational classifications.
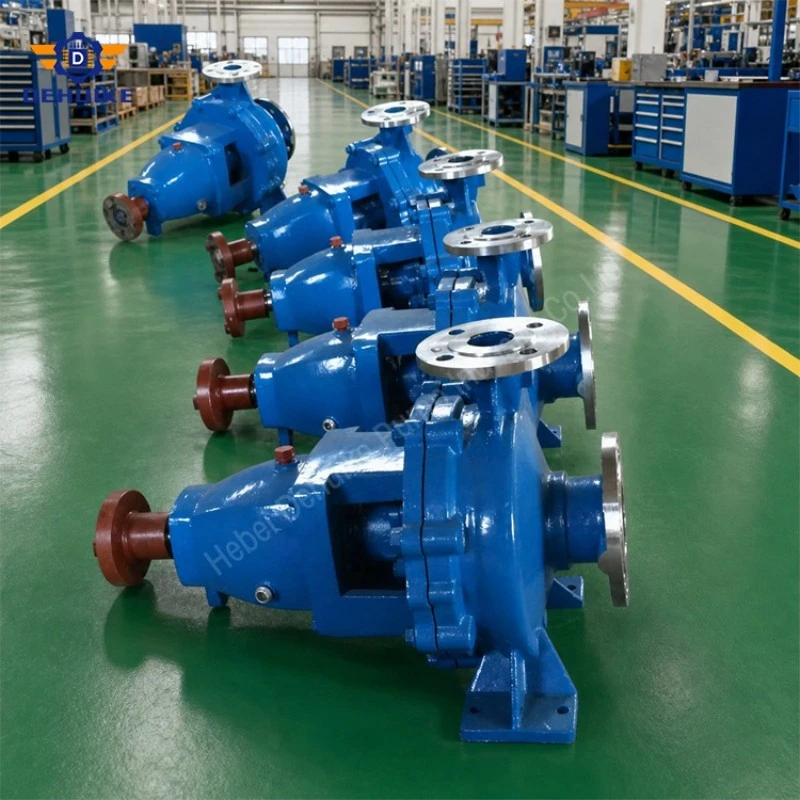
2.1 Series 1: Standard 2-Pole High-Head Sealless Magnetic Series (2900 r/min Baseline)
Series 1 incorporates high-speed two-pole synchronous magnetic drives operating at 2900 rpm. This velocity configuration develops discharge heads reaching up to 84 meters while delivering throughputs from 12.5 m³/h to 100 m³/h at optimal efficiency points, supplying vital fluid energy for pressurized reaction vessels, column reflux headers, and elevated tank farms.
Utilizing full-diameter impellers at 2900 rpm, Series 1 achieves hydraulic energy conversion ratings peaking at 78% in mid-to-large casings. Net positive suction head requirements remain stably bounded between 2.0 and 4.0 meters under full-flow velocity. Tabulated below are baseline operational ratings for representative Series 1 models:
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH50-32-125 |
50 |
32 |
2900 |
12.5 |
20 |
60 |
1.13 |
2.2 |
2 |
|
IH50-32-160 |
50 |
32 |
2900 |
12.5 |
32 |
54 |
2.02 |
3 |
2 |
|
IH65-50-160 |
65 |
50 |
2900 |
25 |
32 |
65 |
3.35 |
5.5 |
2 |
|
IH65-40-200 |
65 |
40 |
2900 |
25 |
50 |
60 |
5.67 |
7.5 |
2 |
|
IH80-65-160 |
80 |
65 |
2900 |
50 |
32 |
73 |
5.97 |
7.5 |
2.5 |
|
IH80-50-250 |
80 |
50 |
2900 |
30 |
84 |
52 |
13.2 |
22 |
2.5 |
|
IH100-80-160 |
100 |
80 |
2900 |
100 |
32 |
78 |
11.2 |
15 |
4 |
|
IH100-65-250 |
100 |
65 |
2900 |
100 |
80 |
72 |
30.3 |
37 |
3.8 |
2.2 Series 2: Precision Impeller-Trimmed Optimization Series (A/B Trims at 2900 r/min)
Specifying oversized sealless pumps to compensate for uncertain friction factors causes equipment to run far to the left of optimal efficiency, raising containment shell operating temperatures and wasting electrical power across discharge valves. Series 2 addresses this inefficiency through calibrated impeller outside diameter reductions (designated by suffixes A and B).
Machining outer vane tips in strict conformity with centrifugal laws adapts the pump head curve to actual piping system friction. For instance, trimming model IH50-32-125 down to trim 'A' reduces head from 20 m to 16 m, matching a 1.5 kW drive while preserving a 60% hydraulic rating. This trim precision lowers operational electrical draw across continuous processing shifts.
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH50-32-125A |
50 |
32 |
2900 |
11.2 |
16 |
60 |
1.18 |
1.5 |
2 |
|
IH50-32-160B |
50 |
32 |
2900 |
10.8 |
24 |
54 |
1.32 |
2.2 |
2 |
|
IH65-50-160A |
65 |
50 |
2900 |
23.4 |
28 |
65 |
2.75 |
4 |
2 |
|
IH65-40-200A |
65 |
40 |
2900 |
23.7 |
45 |
60 |
4.83 |
5.5 |
2 |
|
IH80-65-160A |
80 |
65 |
2900 |
46.8 |
28 |
73 |
4.8 |
5.5 |
2.5 |
|
IH80-50-250B |
80 |
50 |
2900 |
43.3 |
60 |
63 |
11.23 |
15 |
2.5 |
|
IH100-80-160A |
100 |
80 |
2900 |
93.51 |
28 |
78 |
9.16 |
11 |
4 |
|
IH100-65-250A |
100 |
65 |
2900 |
93.5 |
70 |
72 |
26.6 |
30 |
3.8 |
2.3 Series 3: 4-Pole Low-Speed Low-Eddy Heavy-Duty Series (1450 r/min J/JA Trims)
Pumping high-vapor-pressure chemicals, viscous reagents, or temperature-sensitive liquids at 2900 rpm generates elevated eddy-current heating that can cause localized liquid flashing within the containment shell. Series 3 resolves this thermal vulnerability by utilizing four-pole electric drives running at a conservative 1450 rpm (identified by the J suffix).
Halving shaft rotational speed cuts peripheral magnet velocity by 50%, which reduces metallic containment shell eddy-current thermal generation by more than seventy percent. Suction head demands remain remarkably benign, holding required NPSH down to 2.0 to 2.5 meters. Shaft power demands stay modest (0.16 kW to 4.0 kW), establishing Series 3 as an exceptional engineering choice for volatile solvent distillation, vacuum extraction, and continuous hazardous fluid service.
|
Model |
Suct. DN1 |
Disch. DN2 |
Speed (rpm) |
Flow (m³/h) |
Head (m) |
Eff. (%) |
Shaft P (kW) |
Motor P (kW) |
NPSH (m) |
|
IH50-32-125J |
50 |
32 |
1450 |
6.3 |
5 |
54 |
0.16 |
0.55 |
2 |
|
IH50-32-160J |
50 |
32 |
1450 |
6.3 |
8 |
48 |
0.29 |
0.55 |
2 |
|
IH65-50-160J |
65 |
50 |
1450 |
12.5 |
8 |
60 |
0.45 |
0.75 |
2 |
|
IH65-40-250J |
65 |
40 |
1450 |
12.5 |
20 |
46 |
1.48 |
2.2 |
2 |
|
IH80-65-160J |
80 |
65 |
1450 |
25 |
8 |
69 |
0.79 |
1.5 |
2.5 |
|
IH80-50-250J |
80 |
50 |
1450 |
25 |
20 |
60 |
2.27 |
3 |
2.5 |
|
IH100-80-160J |
100 |
80 |
1450 |
50 |
8 |
75 |
1.45 |
2.2 |
2.5 |
|
IH100-65-250J |
100 |
65 |
1450 |
50 |
20 |
68 |
4 |
5.5 |
2 |
Hermetic Containment Shell, High-Flux Magnetic Coupling, and Silicon Carbide Hydrodynamic Bearings
The operational durability of the Magnetic Drive Chemical Pump depends on its heavy-duty mechanical architecture and comprehensive fluid containment design. Every structural element is engineered to maintain dimensional stability and prevent fluid migration under aggressive chemical exposure:
- Heavy-Walled Hermetic Containment Shell: Formed from deep-drawn Hastelloy C-276, titanium, or non-conductive ceramics, the static isolation shroud encloses internal rotor components without weld seams. Wall profiles are optimized to provide generous burst safety margins exceeding 5.0 MPa while minimizing wall thickness to limit eddy-current thermal generation.
- Rare-Earth Permanent Magnetic Couplings: Both inner and outer magnetic rings incorporate high-density samarium-cobalt (Sm₂Co₁₇) magnets arranged in multipole cylindrical arrays. Magnets are hermetically encapsulated within laser-welded stainless or titanium alloy sheaths, shielding magnetic cores from chemical moisture and mechanical chipping.
- Self-Lubricating Sintered Alpha Silicon Carbide Bearings: Internal stationary bushings and rotating shaft sleeves are manufactured from diamond-hard sintered alpha silicon carbide (SSiC). This material provides extreme hardness (Vickers > 2500 kg/mm²), zero chemical reactivity across all pH levels, and low friction under liquid film hydrodynamic lubrication.
- Hydrodynamic Internal Cooling & Lubrication Circulation: A portion of pumped discharge fluid is diverted internally through dedicated channels, flowing through the containment shell annular gap to dissipate eddy-current heat and across silicon carbide bearings before returning to the pump suction eye.
- Dual-Containment Armored Outer Frame: The secondary containment casing consists of heavy ductile iron or stainless steel armor that encloses the drive assembly, providing secondary emergency containment in the rare event of primary shroud damage.
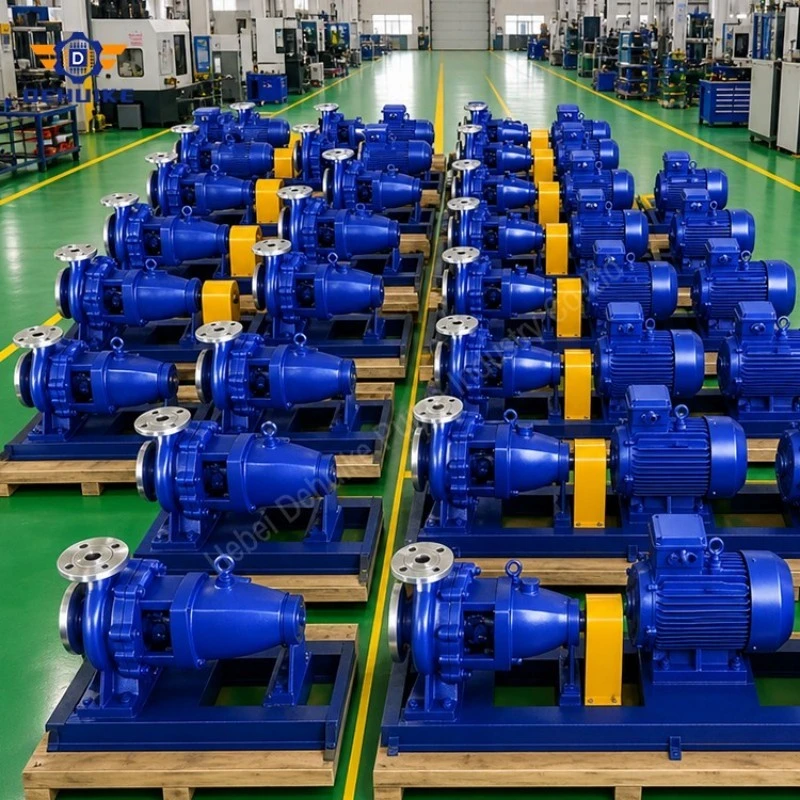
Zero Leakage Assurance, Thermal Eddy-Current Mitigation, and Process Dry-Run Protection
Operating in high-hazard chemical processing environments demands specialized mechanical construction that shields magnetic couplings from thermal and mechanical stress. The Magnetic Drive Chemical Pump incorporates several distinct structural features:
- Hermetic Zero-Fugitive Environmental Containment: By removing rotating dynamic shaft seals, the pump completely prevents chemical vapor leakage, odor escape, and hazardous material spills, complying with stringent environmental regulations such as TA-Luft and OSHA mandates.
- Eddy-Current Thermal Mitigation Geometry: The magnetic shroud cavity is hydrodynamically shaped to maintain vigorous liquid exchange even under low-flow operation. For heat-sensitive or volatile liquids, hybrid non-metallic or laminated composite containment shells eliminate eddy currents entirely, preventing fluid temperature rise.
- Magnetic Decoupling Protection & Overload Margins: Synchronous magnetic couplings are sized with a minimum 1.5 to 2.0 torque safety factor over peak motor shaft torque. If transient mechanical blockage occurs, magnets decouple synchronously without breaking internal drive components or overloading the driver.
- Diamond-Like Carbon (DLC) Bearing Surface Coating: Silicon carbide thrust and journal bearing faces can be enhanced with diamond-like carbon coatings, providing boundary dry-lubrication protection that withstands short-term dry-running or gas-entrainment episodes during pump priming.
- Integrated Bearing Housing Thermal Sensor Wells: Outer bearing carriers feature integrated PT100 resistance temperature detector (RTD) wells and vibration monitor mounts, enabling continuous predictive condition monitoring to catch abnormal thermal rise before magnet demagnetization occurs.
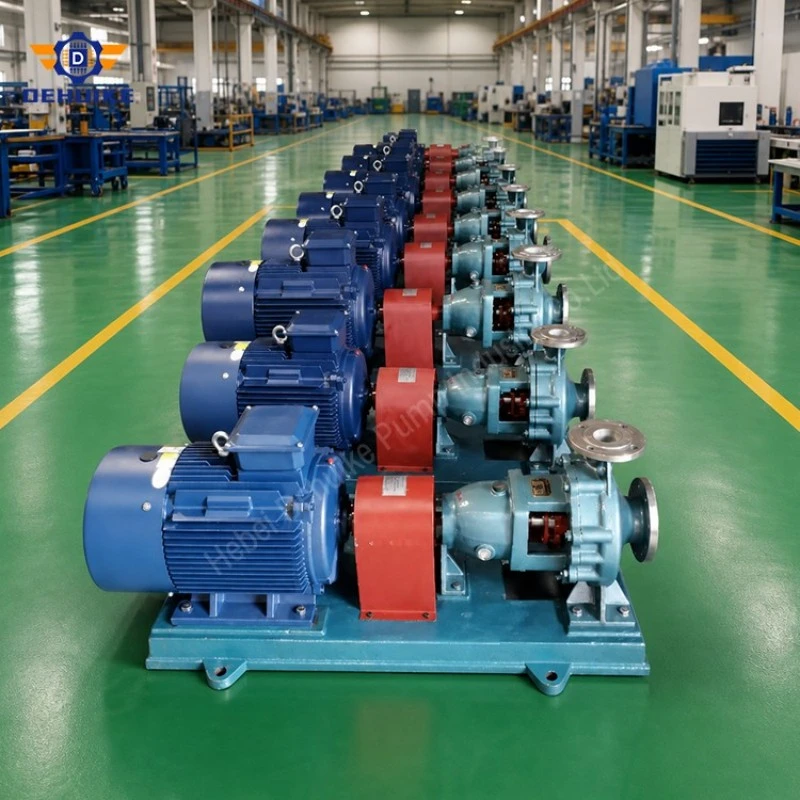
Precision Magnetic Sizing, In-House Eddy-Current Testing, and 30+ Years Engineering Heritage
Hebei Dehuike Pump Industry Co., Ltd. delivers compelling operational value founded upon complete manufacturing integration and four decades of specialized engineering focus. Backed by more than 30 years of specialized pump engineering and manufacturing expertise, our enterprise oversees every stage of fabrication within dedicated industrial facilities:
- Finite Element Magnetic Field Modeling: Our engineering team utilizes finite element electromagnetic simulation software to design magnetic couplings, optimizing flux concentration across the containment shroud while minimizing parasitic eddy-current power loss.
- In-House Containment Shell Burst & Eddy Testing: Every containment shell design undergoes destructive hydro-burst pressure testing up to 10 MPa, coupled with dynamometer thermal rise verification across various motor loads to certify eddy dissipation before factory release.
- Automated Five-Axis CNC Machining Accuracy: Precision boring and facing of volute registers, seal covers, and bearing housings take place on advanced multi-axis machining centers. Concentricity and perpendicularity tolerances are maintained within 0.015 mm, eliminating shaft binding and vibration.
- Extensive Metallurgical Compatibility Matrix: Casing and impeller components are cast in-house across diverse alloys-including 304 (CF8), 316L (CF3M), Duplex 2205, Hastelloy C-276, and titanium-providing complete material matching for specific chemical process streams.
Magnetic Coupling Torque Sizing, Fluid Viscosity / Vapor Margin Review, and International Standardization
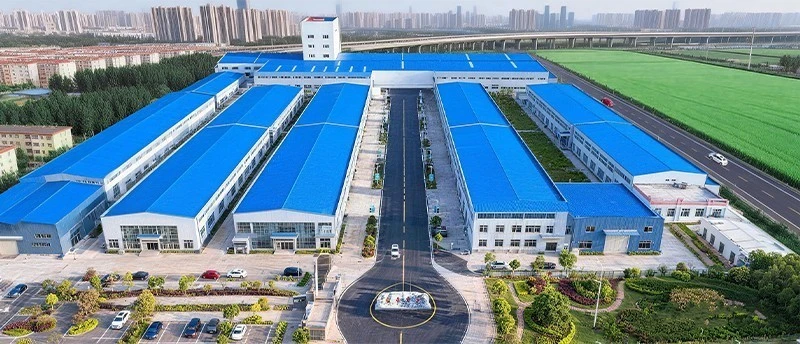
At Dehuike Pump Industry, customer commitment encompasses thorough engineering reviews to guarantee safe sealless pump integration across critical chemical installations:
- Containment Cavity Thermal Balance Analysis: Our engineering staff models fluid vapor pressure curves against calculated eddy-current heat inputs, ensuring internal cooling circulation maintains fluid temperatures at least 15°C below saturation boiling limits to prevent bearing dry-run.
- Coupling Breakaway Torque Margins: For high-viscosity media or cold startup scenarios, starting torque spikes can induce slip. We calculate transient startup shear to size magnetic couplings with verified 1.5x to 2.0x torque safety margins.
- Universal Piping Flange Connections: Outer armored casing nozzles are machined to international pipeline standards-supporting ANSI/ASME B16.5 Class 150/300, EN 1092-1 PN16/25, and JIS B2220 10K-eliminating field piping modifications.
- Field Support and Emergency Spares Readiness: We provide complete installation guidelines, power monitor calibration data, and dedicated warehouse inventory of replacement silicon carbide bearings, containment shells, and outer magnetic assemblies.
Toxic Reagents, Volatile Carcinogens, Flammable Solvents, and Ultra-Hazardous Chemical Synthesis
Delivering complete chemical containment across hazardous process fluids, the Magnetic Drive Chemical Pump performs critical duties across several high-consequence industrial sectors:
- Toxic Chemical Synthesis & Isocyanate Production: Transferring phosgene derivatives, methyl isocyanate, dimethyl sulfate, and hydrocyanic acid where zero leakage is an absolute life-safety mandate.
- Volatile Hydrocarbons & Flammable Solvent Handling: Circulating benzene, toluene, xylene, hexane, ethers, and acetone in explosion-proof refinery units without risking spark-induced atmospheric ignition.
- Refrigeration Systems & Liquefied Gas Handling: Pumping liquid ammonia, fluorinated refrigerants, sulfur dioxide, and pressurized liquefied gases under closed refrigeration and gasification loops.
- Electronic Chemicals & Ultra-Pure Chemical Distribution: Circulating high-purity acids, developers, and photoresist solvents with zero contamination from external mechanical seal barrier fluids.
- Nuclear, Radioactive & Heavy Chemical Processing: Safely circulating radioactive heavy water, enriched chemical isotopes, and hazardous catalyst slurries under hermetic isolation.
- Precious Metal & Specialty Catalyst Chemical Lines: Pumping high-value platinum, palladium, and rhodium catalyst solutions where mechanical seal leakage would incur significant financial loss.
Corporate Manufacturing Pedigree, Commercial Standards, and Direct Engineering Contacts
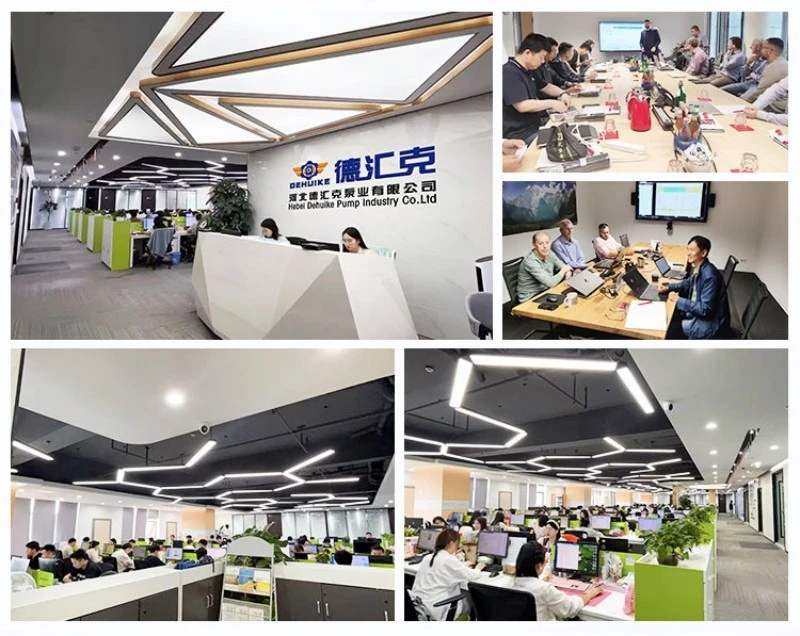
Hebei Dehuike Pump Industry Co., Ltd. is a recognized industrial manufacturer specializing in sealless, zero-leakage chemical fluid machinery. Drawing upon over three decades of focused engineering innovation, our production facilities deliver reliable pumping equipment to hazardous processing installations across more than 90 countries worldwide.
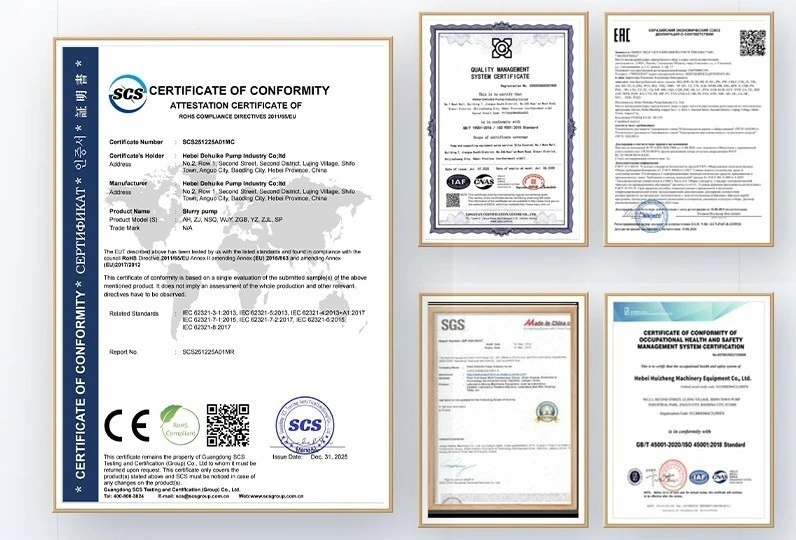
Our specialized technical staff conducts comprehensive upfront reviews of customer process conditions-evaluating chemical vapor pressures, temperature-viscosity curves, pipe friction calculations, and magnetic torque requirements to configure optimal pump frames, trims, and containment shells. Plant operations adhere strictly to certified ISO 9001 quality management guidelines, reinforced by EAC conformity certification and RoHS environmental directives. Global shipments are managed under FOB and CIF destination port trade terms, utilizing air cargo (50 kg to 500 kg) and maritime container freight (500 kg and higher).
Technical Decision Guide: Materials, Hydraulic Integrity, and Global Supply FAQ
Q1: What prevents high-temperature demagnetization in magnetic drive chemical pumps?
A: Magnetic stability is governed by magnet material selection and effective cooling flow design. We exclusively utilize high-temperature grade Sm₂Co₁₇ samarium-cobalt magnets possessing high magnetic coercivity and a Curie temperature above 350°C, permitting continuous chemical pumping at temperatures up to 250°C without flux decay. Additionally, internal product recirculation continuously sweeps across the containment shell, transferring eddy-current heat back into the main process stream to keep magnet operating temperatures safely below thermal degradation limits.
Q2: How do magnetic drive pumps handle liquids with entrained solid particles or crystalline precipitates?
A: Because internal sleeve bearings rely on pumped fluid for hydrodynamic lubrication, hard suspended solids can cause abrasive scoring on silicon carbide surfaces, and magnetic particles can adhere to inner rotor magnets. For services containing fine solids (<5% concentration by weight and <50 µm particle size), pumps can be equipped with external clean flush lines, magnetic separators, or internal cyclone separators that centrifuge clean liquid to the bearings while discharging solids back to the main flow path.
Q3: What causes magnetic decoupling, and how does the pump design prevent decoupling damage?
A: Magnetic decoupling occurs when system load torque exceeds the maximum breakaway torque of the magnetic coupling-often provoked by rapid valve closures, fluid slugging, or heavy motor starting currents. Our magnetic couplings are designed with a 1.5 to 2.0 torque safety margin over peak shaft torque. If decoupling occurs, magnets slip harmlessly without mechanical damage. Modern motor power monitors instantly detect the resulting motor load drop and shut down the driver within 0.1 seconds to prevent thermal buildup.
Q4: When should chemical plant designers specify a 1450 r/min four-pole drive rather than a two-pole 2900 r/min motor?
A: While two-pole 2900 rpm configurations offer compact footprints for high-head clean duties, four-pole 1450 rpm drives (J-series) are strongly indicated when handling liquids with kinematic viscosities above 30 cSt, warm volatile chemicals near boiling point, or slurries carrying fine crystal suspensions. Lowering rotational velocity reduces impeller peripheral tip speed by half, curbing mechanical seal face friction, suppressing cavitation inception, and extending equipment service life significantly.
Q5: How should piping designers calculate suction line losses to safeguard required NPSH?
A: In sealless magnetic pumps, cavitation does not merely erode impellers-it collapses the hydrodynamic fluid film across internal silicon carbide sleeve bearings, provoking instant dry friction and thermal shock fractures. Suction line design must ensure Net Positive Suction Head available (NPSHa) exceeds the pump threshold (NPSHr) by at least 1.0 meter under worst-case summer ambient temperatures. Suction piping must be sized one pipe diameter larger than the pump intake nozzle, incorporate straight piping runs of at least 5 to 10 pipe diameters before the suction flange, and strictly avoid high-point vapor traps.
Q6: What manufacturer warranty provisions cover magnetic drive pump installations?
A: All units carry our comprehensive 2-year (24-month) manufacturer equipment warranty, protecting against casting defects, containment shell rupture, and magnetic drive torque loss under specified process conditions. Because magnetic pumps eliminate dynamic mechanical seals, traditional seal leakage failures are completely avoided. Factory-certified replacement assemblies-including sintered silicon carbide bearing sets, containment shells, and matched magnetic rotor pairs-are stocked for rapid global dispatch.
Q7: What international packaging and export shipping standards apply to magnetic equipment?
A: Standard production fabrication requires 15 to 25 business days for standard stainless steel models, and 30 to 45 business days for custom Hastelloy or insulated jacketed configurations. Because high-energy permanent magnets can interfere with navigational avionics, air shipments feature specialized magnetic field shielding in accordance with IATA Packing Instruction 953. Maritime shipments are sealed in vapor-barrier foil with desiccants and secured within ISPM-15 certified plywood crates. Commercial contracts follow Incoterms 2020 on FOB and CIF destination port terms, utilizing expedited air freight (50 kg to 500 kg) and ocean container transport (500 kg and above).
Hot Tags: magnetic drive chemical pump, China magnetic drive chemical pump manufacturers, suppliers, factory