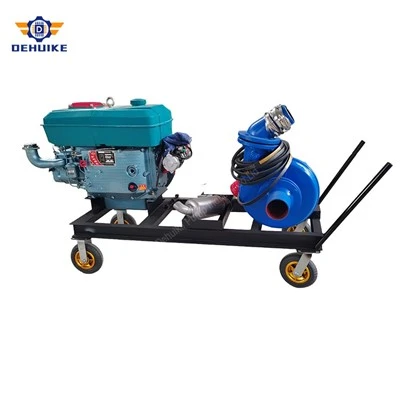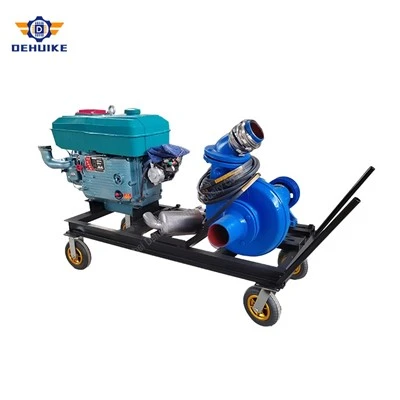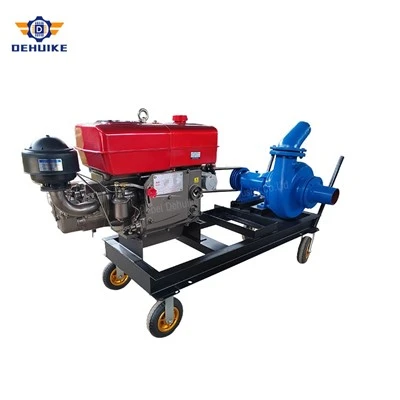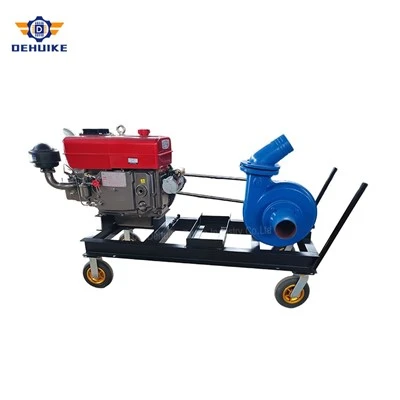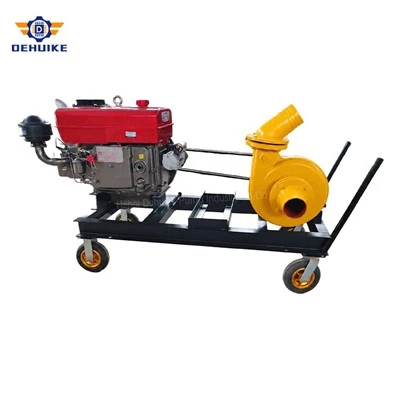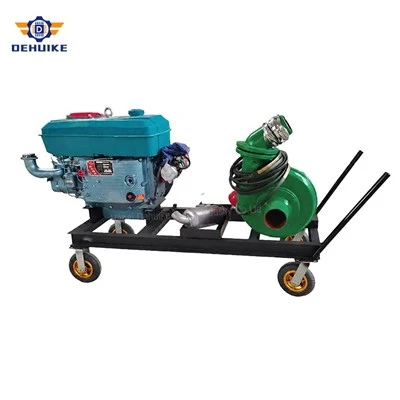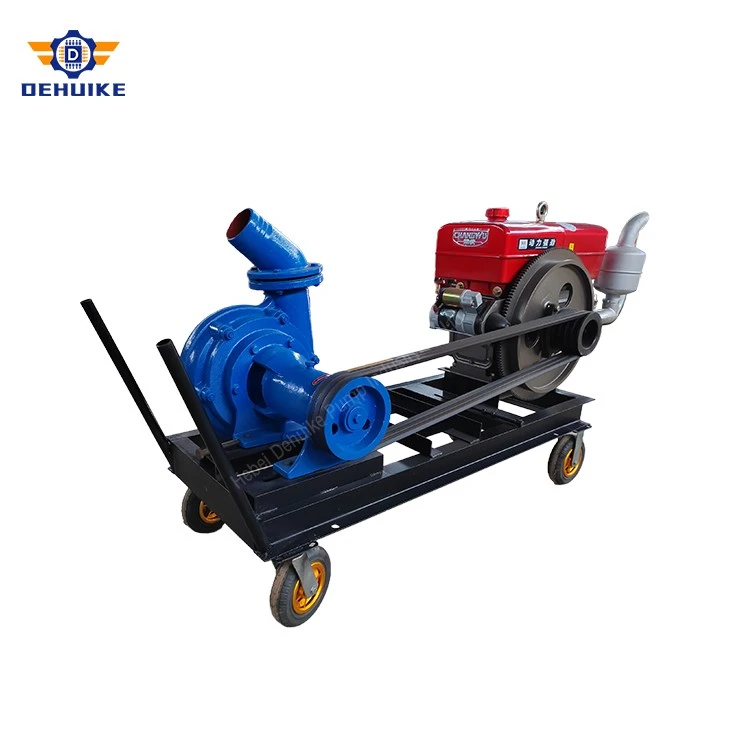
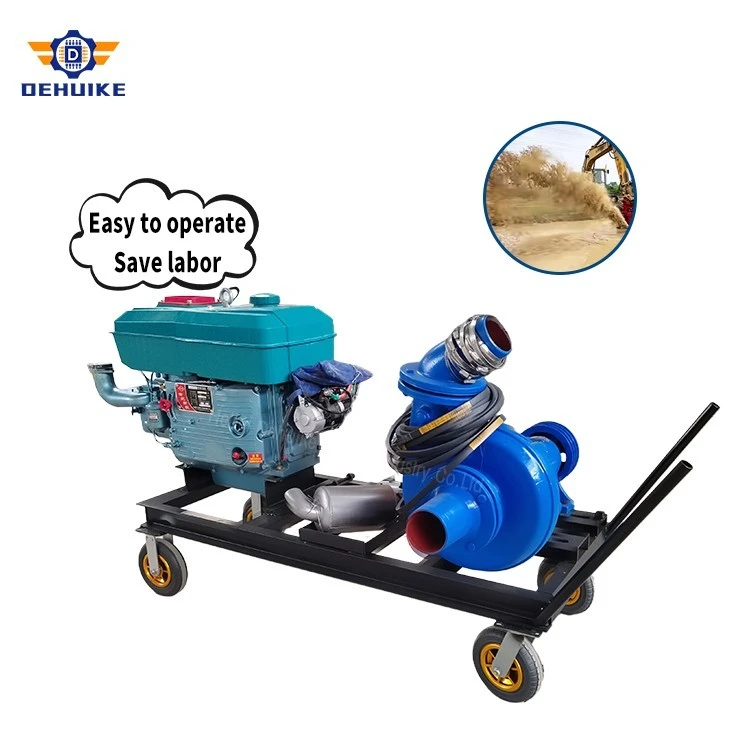
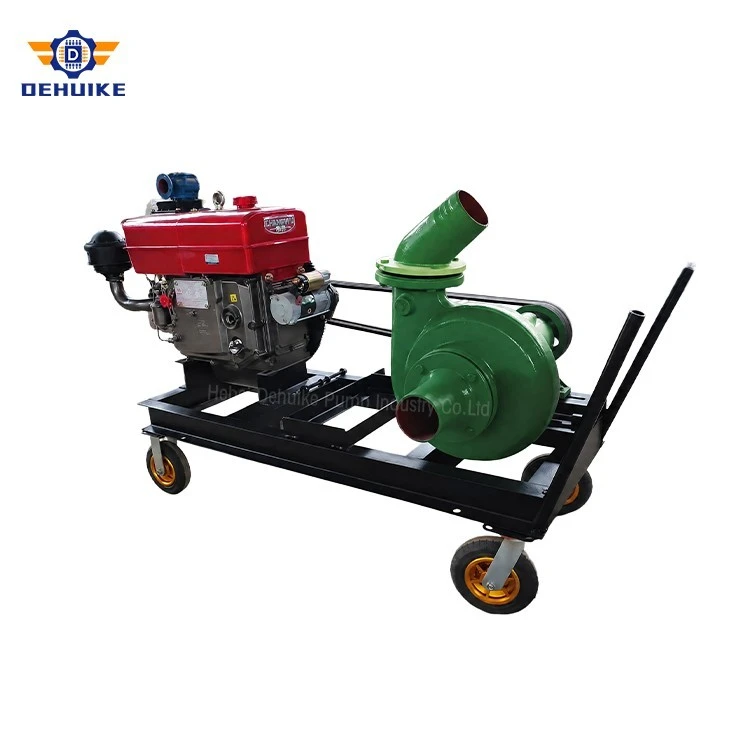
Hebei Dehuike Pump Industry Co., Ltd. is one of the most reliable manufacturers and suppliers of mini drainage pump in China. With abundant experience, we are committed to providing high quality customized pumps with competitive price. Welcome to wholesale bulk mini drainage pump for sale here from our factory. Also, pricelist is available.
Experience and Markets
Backed by over 30 years of continuous fluid equipment manufacturing, our factory engineers dependable dewatering solutions for harsh international engineering job sites. Each mini drainage pump leaving our production cells benefits from decades of empirical troubleshooting across emergency municipal dewatering, subterranean pipeline construction, and industrial effluent management.
To date, our pumps have served demanding project contractors across 50+ countries:
- Southeast Asian archipelagos: Handling monsoon stormwater evacuation, tidal basement dewatering, and brackish aquaculture basin circulation under severe ambient heat and 95%+ relative humidity.
- Middle Eastern infrastructure zones: Operating in coastal foundation trenching and telecom utility vaults, evacuating groundwater contaminated with abrasive gypsum fines and corrosive salts.
- The Americas: Dispatched to open agricultural canals, highway culvert cleanouts, and deep excavation sumps requiring continuous unattended drawdown.
- Eurasian and Central Asian territories: Utilized by municipal emergency crews on mobile response vehicles for rapid stormwater relief during seasonal snowmelt and flash inundation.
Our extensive cross-border field track record guarantees that every mini drainage pump we ship is hydraulically calibrated for genuine duty cycles rather than hypothetical catalog charts.
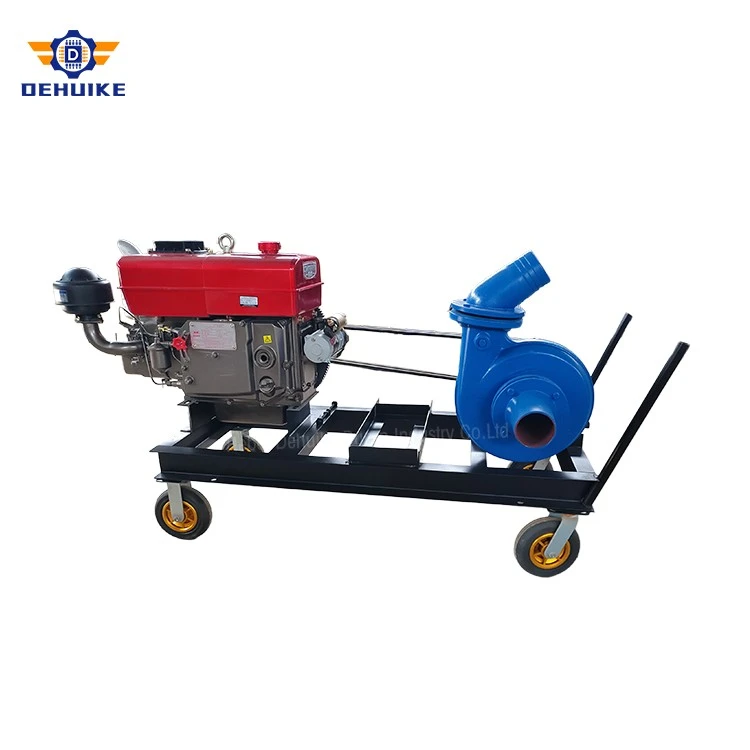
Company Milestones / History
Across three decades of industrial manufacturing, our company has evolved from a traditional pump foundry into a specialized exporter of high-spec submersible drainage machinery. The technological development of the mini drainage pump highlights our focused commitment to practical mechanical reliability:
- Phase 1 (Foundry Foundations): Commenced operations producing high-grade grey iron volutes and agricultural water extraction assemblies, establishing our foundational metallurgical controls.
- Phase 2 (Submersible Motor Encapsulation): Mastered airtight motor encapsulation and stator vacuum resin impregnation, overcoming moisture leakage failures common in early electrical pumps.
- Phase 3 (Compact Hydraulics R&D): Created a dedicated mini drainage pump engineering unit focused on high-torque, low-weight vortex hydraulics, specifically designed for confined utility manholes.
- Phase 4 (International Trade Compliance): Aligned all dimensional tolerances, testing criteria, and electrical insulation standards with global industrial directives, opening volume exports to overseas utility contractors.
- Phase 5 (Digital Hydrodynamic Testing): Constructed a fully digitized, closed-loop testing facility to test flow rates, electrical consumption, and thermal curves for every production batch.
This long manufacturing history proves our engineering integrity; we build our own motors, machine our own castings, and inspect every critical clearance directly under our own roof.
Customer Questions
During technical bid reviews and equipment procurement evaluations for the mini drainage pump, mechanical engineers and site superintendents routinely address the following critical inquiries:
Q1: How effectively does this compact unit handle abrasive mud, fine sand, and suspended solids?
While built with a compact silhouette, the internal vortex impeller is cast from high-strength wear alloy, creating a generous internal swirling action that channels solids out through the discharge port without pinching against the casing walls. A heavy-duty oil-bathed dual mechanical seal (silicon carbide vs. silicon carbide) maintains a protective barrier against sand ingress.
Q2: Can these pumps be deployed with portable job site fuel generators?
Yes. Our motor stators are designed with heavy wire cross-sections to tolerate ±10% voltage variance commonly generated by portable site generators. Dual frequency windings (50 Hz and 60 Hz) and multiple worldwide voltage configurations (from 110V single-phase up to 460V three-phase) are built directly to project order.
Q3: What warranty protection and spare part support does the factory provide?
We grant an extensive 24-month (2-year) warranty on the complete pump assembly (wear parts excluded per standard global industry practice). Essential maintenance kits-including replacement mechanical seal cartridges, O-ring sets, and spare impellers-are stocked in depth for immediate expedited dispatch via air freight.
Our Factory Facilities
Covering an integrated industrial footprint exceeding 8,000 square meters, our manufacturing complex integrates advanced fabrication, precision component finishing, and clean assembly lines under a unified production management system:
- Precision CNC Machining Facility: Features rigid horizontal turning centers, vertical CNC milling machines, and dedicated shaft-grinding stations. Tight tolerances on bearing fits, shaft concentricity, and mechanical seal register grooves are held within micrometric thresholds.
- Specialized Stator Winding & Dipping Bay: Stators are wound using high-purity oxygen-free electrolytic copper magnet wire on automated programmable winding machines. Completed assemblies undergo dual vacuum pressure impregnation (VPI) with Class H insulating resin, followed by uniform convection oven curing.
- Dedicated Pump Assembly Lines: Every mini drainage pump is assembled in clean, dust-controlled workstations. Technicians use precision dial gauges to calibrate impeller running clearances and ensure correct spring pre-load compression on all mechanical seal sets.
- Heavy-Duty Protective Coating Line: Pump castings undergo automated shot-peening to white-metal surface cleanliness, followed by electrostatic application of cross-linked high-build epoxy powder cured at 200°C to withstand chemical effluents and coastal salinity.
- Multimodal Export Packaging Section: Finished machines are bolted securely onto timber skids, lined with moisture-resistant protective film, and crated in sturdy export-grade wooden cases engineered for long-haul sea freight and air freight handling
Our Equipment Testing Lab
1. Computerized Hydrodynamic Test Center: Built to ISO 9001 Grade 2B international testing standards, this closed-loop station utilizes calibrated electromagnetic flow transmitters, digital pressure transducers, and precision torque analyzers to verify head-flow curves and efficiency across the operating range.
2. Microcomputer Dynamic Balancing Benches: Rotating components of each mini drainage pump-including impellers, motor rotors, and drive shafts-are individually dynamically balanced to ISO 1940 Grade G2.5, minimizing vibration to protect bearing longevity.
3. Optical Coordinate Measuring System: High-precision CMM inspection arms verify casting profiles, motor register tolerances, and volute scroll dimensions against original 3D CAD design files.
4. Pressurized Submerged Leak Testing Rigs: Prior to shipping, each fully assembled pump motor chamber and mechanical seal oil reservoir is pressurized with dry compressed air and submerged under clean water to confirm zero seal leakage.
5. Digital Insulation & Dielectric Breakdown Tester: High-voltage surge and dielectric withstand tests (up to 2,500V AC) are performed on every electrical assembly, validating complete operator protection in wet working environments.
Our Certificate Compliance
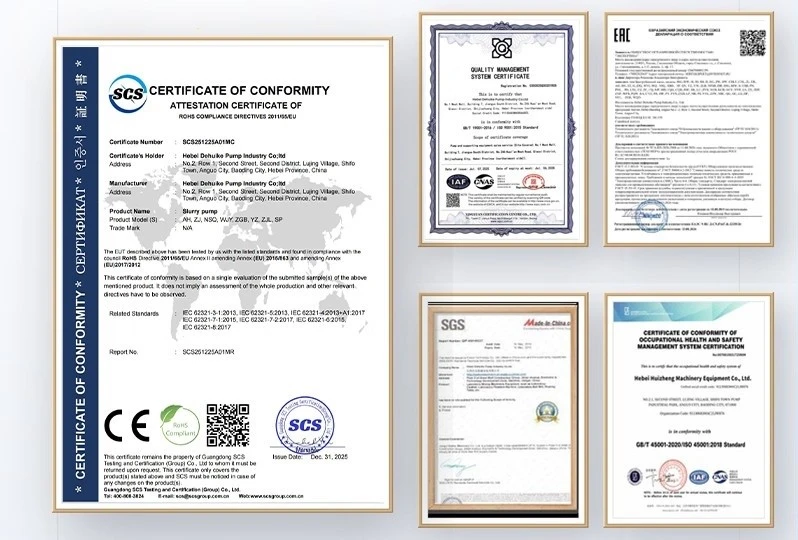
- ISO 9001:2015 Quality Management System: Fully certified across engineering design, metallurgy casting, CNC machining, winding encapsulation, final assembly, and after-sales support for dewatering pump lines.
- EAC Technical Regulation Compliance (CU-TR 010/2011 & CU-TR 004/2011): Validated for machinery safety and low-voltage electrical integrity, guaranteeing regulatory compliance throughout the Eurasian Economic Union.
- RoHS Directive Compliance (EU 2015/863): Rigorously confirms that motor cables, solder alloys, insulation lacquers, and synthetic elastomer seals contain zero restricted hazardous substances.
- Comprehensive Factory Test Certifications: Every export batch of the mini drainage pump is supplied with authenticated factory inspection records, electrical dielectric withstand receipts, and ISO-compliant hydrodynamic curve data sheets.
- ISPM 15 Phytosanitary Packaging Compliance: All export wooden packaging and pallets undergo professional heat treatment and carry certified stamps, assuring hassle-free border clearance across international maritime ports and airports.
Hot Tags: mini drainage pump, China mini drainage pump manufacturers, suppliers, factory